Rare earth materials, including elements such as neodymium, praseodymium, and cerium, are vital in modern industries like electronics, aerospace, and renewable energy. Efficient handling and transportation of these materials are crucial for production efficiency and product quality. Pneumatic conveying systems are widely used for transporting rare earth powders due to their ability to handle fine, abrasive, and potentially hazardous materials with minimal contamination and high throughput. This article examines the working principle and key features of rare earth pneumatic conveying systems, offering insights into their design, operation, and advantages.
Working Principle of Rare Earth Pneumatic Conveying Systems
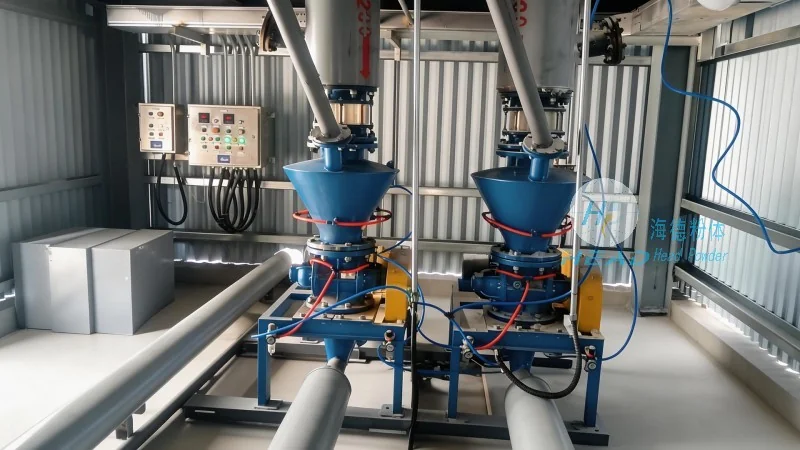
The fundamental operation of a rare earth pneumatic conveying system involves using compressed air or other gases to move solid particles through a pipeline. The system typically includes components like a material feed hopper, conveying line, control valve, and discharge point. The process starts with material being fed into the hopper, then introduced into the conveying line under the pressure of the air stream. The air velocity within the pipeline is maintained at a level to keep rare earth particles suspended, preventing settlement or clogging. The conveying line may have bends, expansions, or other features to accommodate direction or elevation changes, ensuring smooth transport. At the discharge end, air and material are separated, with material collected in a container and air either vented or recirculated for energy efficiency.
Key Features of Rare Earth Pneumatic Conveying Systems
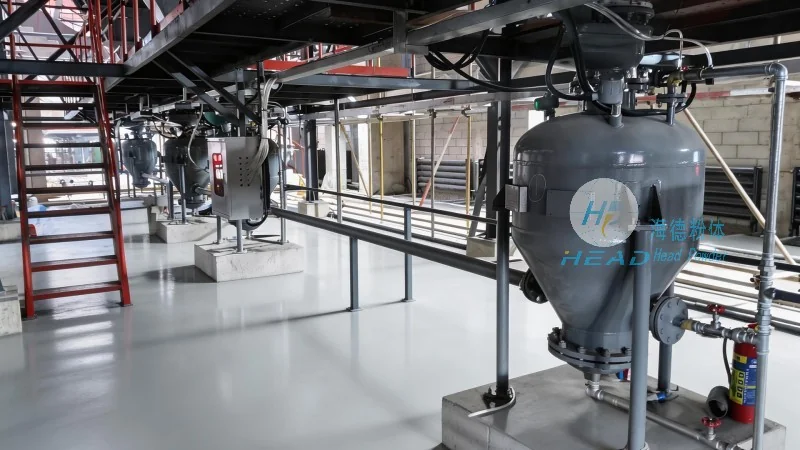
Several features make rare earth pneumatic conveying systems ideal for these specialized materials. First, the system provides high containment, minimizing dust and environmental impact—critical for hazardous rare earth powders. Second, it allows precise control over flow rates and pressure for accurate dosing and consistent quality. Third, it can handle a wide range of particle sizes and shapes without extensive pre-processing. Fourth, the equipment is compact and integrates easily into existing lines, reducing installation costs and space needs. Finally, the system prevents contamination by keeping material away from external surfaces, ensuring purity and freedom from impurities.
Application Considerations for Rare Earth Pneumatic Conveying
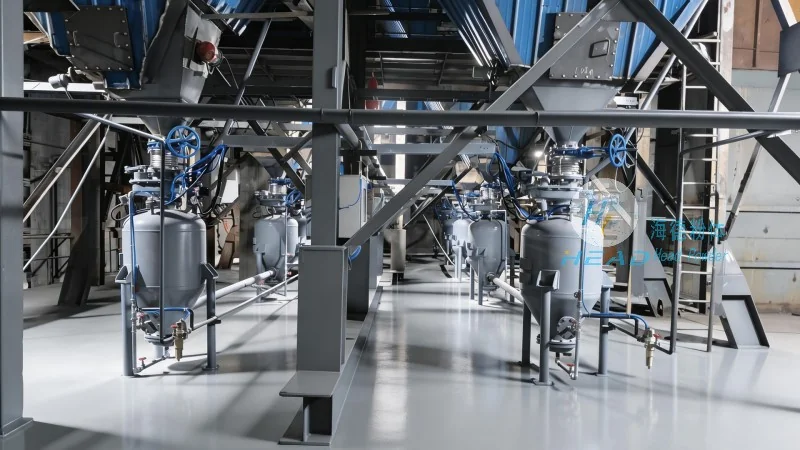
When implementing a rare earth pneumatic conveying system, several factors must be considered. The first is the rare earth material's particle characteristics—density, moisture, and abrasiveness—which influence air velocity, pipeline diameter, and feed mechanisms. Second, the system must meet environmental and safety requirements, such as explosion-proofing or dust collection. Third, energy efficiency is evaluated as compressed air consumption can be a significant cost. Finally, maintenance and longevity are important, as rare earth materials can be abrasive and cause component wear over time.
Conclusion and Company Overview
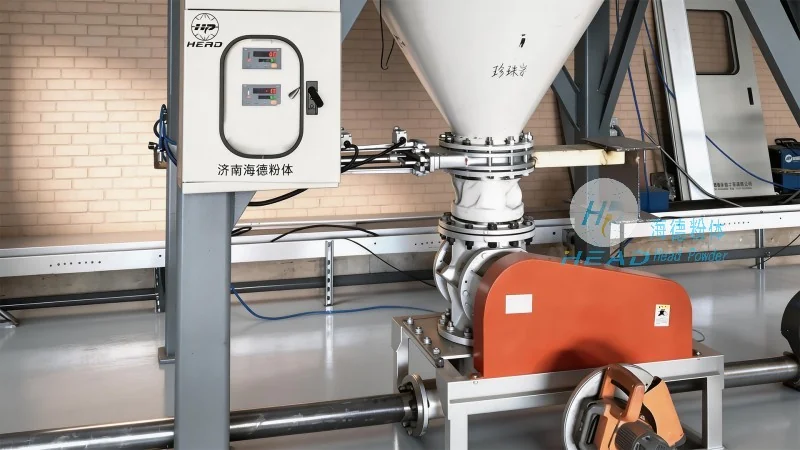
Rare earth pneumatic conveying systems offer a sophisticated solution for efficiently and safely handling rare earth materials. By using compressed air to transport fine powders, these systems provide advantages in containment, precision, and flexibility unmatched by traditional methods. For industries reliant on rare earth elements, investing in a well-designed pneumatic conveying system is essential for maintaining competitiveness and product quality. Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in customizing systems for rare earth processing facilities. With a focus on durability, efficiency, and safety, HeadPowder's systems are engineered for reliable performance in demanding industrial environments. Based in Shandong, China, the company combines advanced engineering with practical experience to deliver solutions that enhance productivity and protect the environment. Whether for new installations or upgrades, HeadPowder's expertise in rare earth pneumatic conveying ensures clients receive optimal equipment for their specific applications.




