Heavy calcium powder, also known as heavy calcium carbonate, is a widely used industrial material in various sectors including construction, plastics, and paper manufacturing. The efficient and reliable transportation of this fine powder is crucial for maintaining production efficiency and product quality. Pneumatic conveying systems have emerged as a preferred solution for handling heavy calcium powder due to their ability to transport materials in a dust-free environment and with minimal product degradation. This article explores the working principle and key features of such systems, highlighting their applications and benefits.
Working Principle of Heavy Calcium Powder Pneumatic Conveying Systems
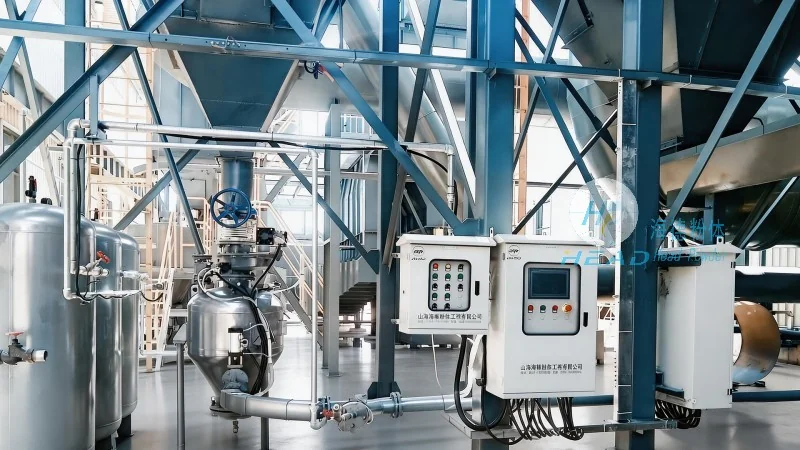
The core mechanism of a pneumatic conveying system involves the use of compressed air to move bulk materials through a pipeline. In the case of heavy calcium powder, the system typically operates on the principle of pressure or vacuum. The process begins with the material being fed into a hopper or feeder, where it is then drawn or pushed into the conveying line by the air flow. The compressed air creates a flow that carries the powder particles along the pipeline, ensuring a continuous and controlled transport. The system may include components such as rotary valves, filters, and cyclones to manage the material flow and prevent blockages or dust emissions. The choice between positive pressure and negative pressure systems depends on factors like the distance to be covered and the nature of the material being conveyed.
Key Features of Heavy Calcium Powder Pneumatic Conveying Systems
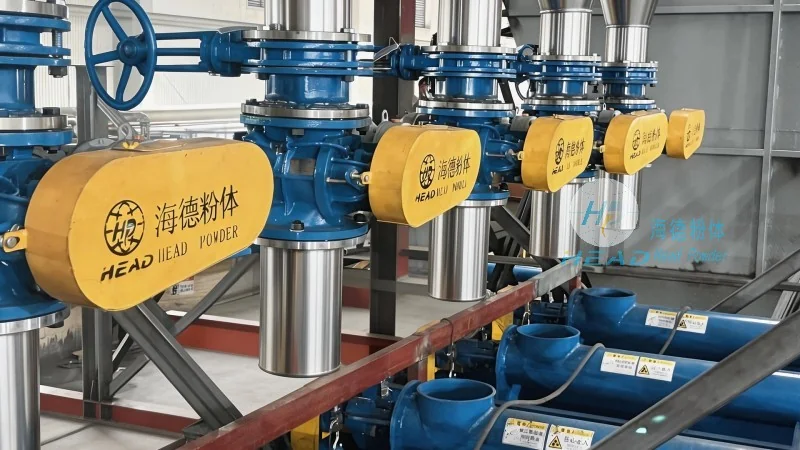
Several distinct features make pneumatic conveying systems suitable for heavy calcium powder applications. Firstly, the systems are designed to operate in a closed environment, which significantly reduces dust pollution and improves workplace safety. This is particularly important in industries where fine powders can cause respiratory issues or environmental contamination. Secondly, the technology allows for gentle handling of the powder, minimizing the risk of agglomeration or degradation of the material. The smooth flow through the pipeline ensures that the particles remain in a consistent state, preserving their quality for downstream processes. Thirdly, the systems offer flexibility in terms of layout and integration with existing production lines. They can be customized to fit various plant configurations, accommodating different distances and material volumes. Additionally, the equipment is relatively easy to maintain, with components like filters and cyclones that can be cleaned or replaced as needed to ensure long-term operational efficiency.
Applications and Benefits in Industrial Settings
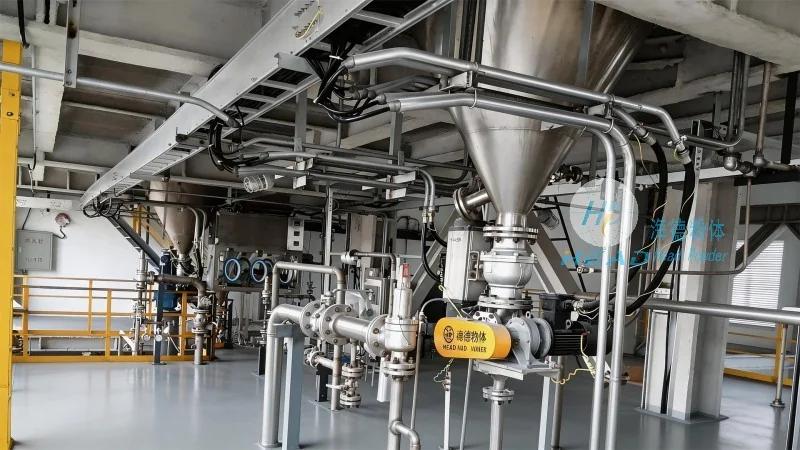
Heavy calcium powder pneumatic conveying systems are widely utilized in industrial settings where the handling of fine powders is essential. In the construction industry, these systems are used to transport calcium carbonate for cement and concrete production, ensuring a consistent supply of raw material. In the plastics industry, the systems help in delivering heavy calcium powder to compounding machines, maintaining the quality of plastic products. The paper industry also benefits from these systems by efficiently conveying calcium carbonate for coating and filler applications. The primary benefits include improved production efficiency, reduced labor costs due to automated material handling, and enhanced product quality through minimized contamination and degradation. Furthermore, the closed system design contributes to environmental compliance by controlling dust emissions, which is increasingly important in modern industrial operations.
Conclusion and Company Overview
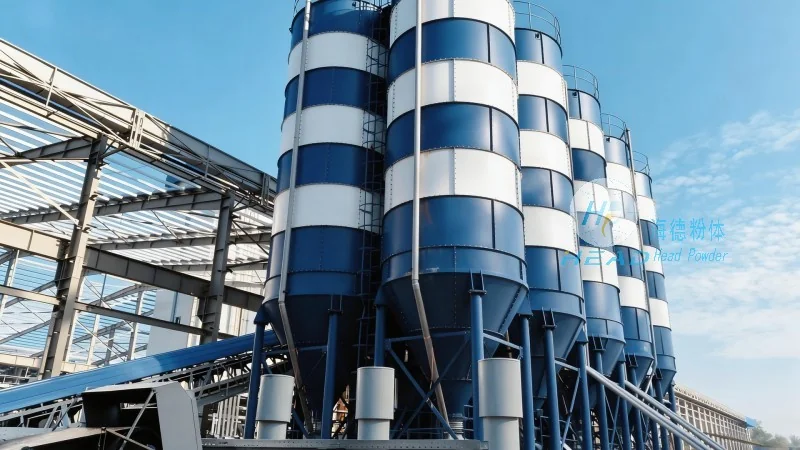
Heavy calcium powder pneumatic conveying systems represent a sophisticated solution for the efficient and safe transportation of fine industrial materials. By leveraging compressed air to move materials through a pipeline, these systems offer numerous advantages over traditional methods like bucket elevators or belt conveyors. The working principle, which involves the controlled use of air pressure or vacuum, ensures a continuous and reliable flow of heavy calcium powder. Key features such as dust-free operation, gentle material handling, and flexible integration make these systems ideal for various industrial applications. The benefits extend to improved workplace safety, reduced product degradation, and enhanced environmental performance. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of clients. With a focus on quality and innovation, the company ensures that its systems meet the highest standards of efficiency and reliability, supporting the operational demands of industries that rely on heavy calcium powder.




