For industries dealing with vanadium compounds, particularly oxidized vanadium materials, efficient and reliable material handling is crucial. An oxidized vanadium material handling system is a specialized equipment setup designed to transport, process, and manage these specific materials safely and effectively. This system integrates various components to ensure smooth operation, from intake to discharge, while adhering to safety and operational standards. The design principles behind such systems are rooted in the unique properties of oxidized vanadium, including its chemical reactivity, physical characteristics, and the need for controlled environments to prevent contamination or degradation.
Key Components of an Oxidized Vanadium Material Handling System
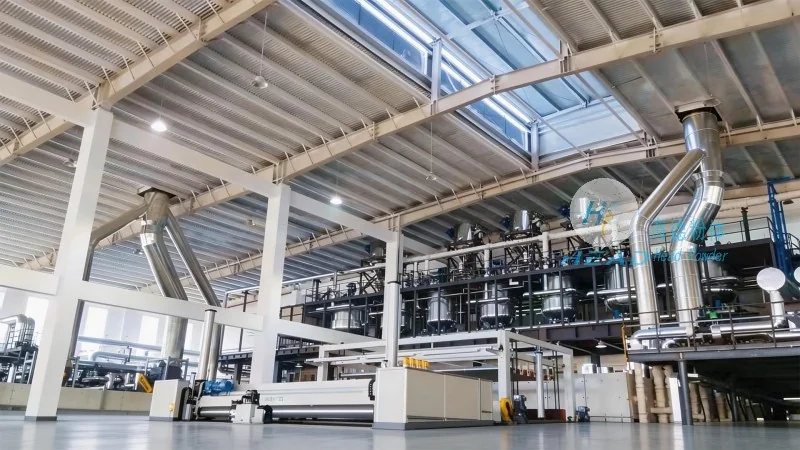
The core of an oxidized vanadium material handling system consists of several interconnected components that work in tandem to achieve optimal performance. These components typically include feed hoppers or chutes for material intake, conveying mechanisms such as screw conveyors, belt conveyors, or pneumatic systems for transporting the material, storage silos or bins for intermediate storage, and discharge mechanisms like spouts or chutes for delivering the material to the next stage of processing. Each component is selected based on the specific properties of oxidized vanadium, such as its particle size, moisture content, and flowability, to ensure efficient and safe handling. For instance, if the material is fine and powdery, a screw conveyor might be preferred to prevent clogging, while a pneumatic system could be used for more delicate or reactive materials that require minimal contact with equipment surfaces.
Design Principles for Safe and Efficient Operation
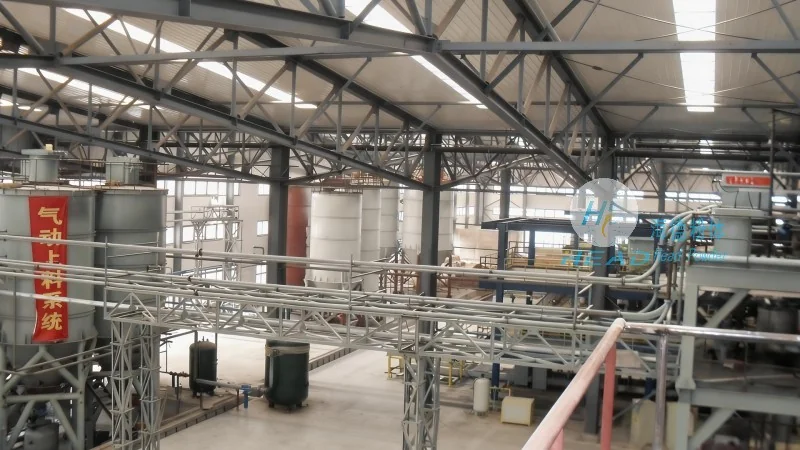
The design principles of an oxidized vanadium material handling system prioritize safety, efficiency, and durability. Safety is paramount due to the potential reactivity of oxidized vanadium with other substances or environmental factors. Therefore, systems are often equipped with explosion-proof features, such as spark-proof motors and sealed components, to prevent accidental ignition. Additionally, the system may include dust suppression mechanisms, like wet scrubbers or dust collection systems, to minimize airborne particles and protect both the material and personnel. Efficiency is achieved through optimized material flow paths, reduced friction, and minimal downtime. This involves careful consideration of the material's flow characteristics, ensuring that the conveying speed and pressure are appropriate to maintain a consistent flow without causing blockages or degradation. Durability is another critical factor, as the system must withstand the corrosive or abrasive nature of oxidized vanadium over extended periods. Materials used in the construction of the system, such as stainless steel or specialized alloys, are chosen to resist wear and corrosion, extending the system's lifespan and reducing maintenance costs.
Application-Specific Considerations
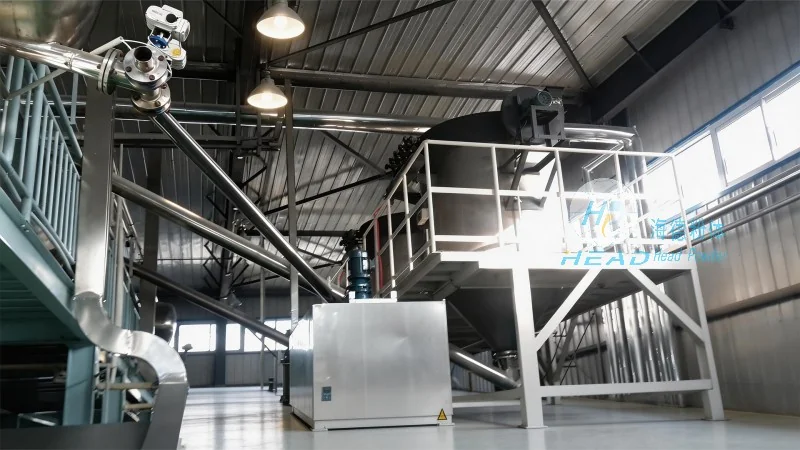
The design of an oxidized vanadium material handling system is often tailored to the specific application or industry. For example, in the chemical industry, where oxidized vanadium is used as a catalyst or raw material in production processes, the system may need to integrate with existing processing lines, requiring compatibility with other equipment and control systems. In mining or mineral processing, the system might handle larger, bulkier oxidized vanadium materials, necessitating robust and heavy-duty components capable of handling high volumes and varying particle sizes. The system may also incorporate monitoring and control features, such as sensors for level, temperature, or pressure, to provide real-time data and enable automated adjustments. This allows operators to maintain optimal conditions and respond quickly to any deviations, ensuring consistent product quality and preventing equipment damage.
HeadPowder Engineering's Expertise in Oxidized Vanadium Material Handling
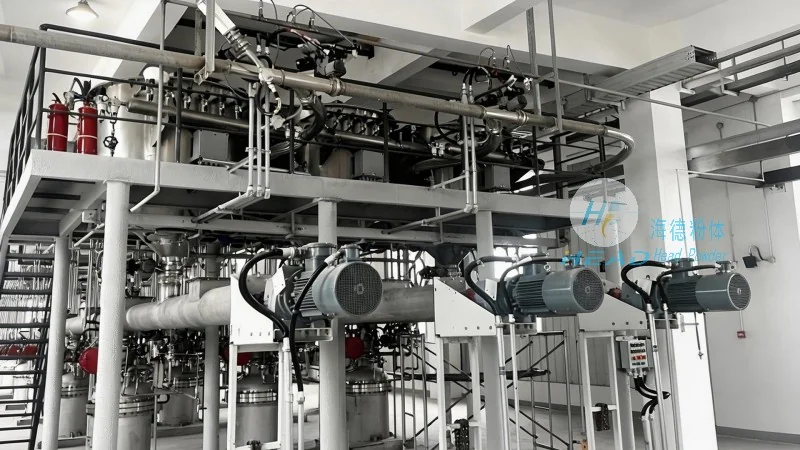
Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized material handling solutions, offers comprehensive services for oxidized vanadium material handling systems. With years of experience in the industry, HeadPowder understands the unique challenges associated with handling oxidized vanadium and designs systems that meet the highest standards of safety, efficiency, and reliability. The company's team of engineers and technicians works closely with clients to assess their specific needs, from material properties and processing requirements to operational constraints and budget considerations. This collaborative approach ensures that the final system is tailored to the client's unique situation, providing a customized solution that maximizes performance and minimizes risks. HeadPowder's commitment to quality is evident in the materials and components used in their systems, which are sourced from reputable suppliers and undergo rigorous testing to ensure compliance with industry standards and regulations. The company also provides ongoing support and maintenance services, ensuring that the system operates at peak performance throughout its lifecycle.




