Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of advanced material handling solutions. This article explores the working principle and key features of our tote bag dust-free loading station material handling systems, designed to enhance efficiency and safety in industrial material transfer processes.
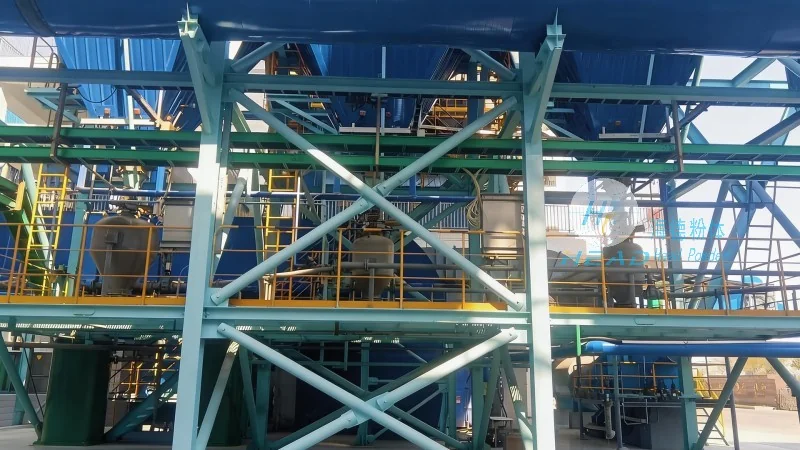
Introduction to Tote Bag Dust-Free Loading Station Material Handling Systems
Our tote bag dust-free loading station is engineered to facilitate the seamless transfer of bulk materials from large tote bags into processing equipment, while maintaining a controlled, dust-free environment. This system is particularly crucial in industries such as pharmaceuticals, food processing, and chemical manufacturing, where contamination control is paramount. The system integrates advanced dust extraction, material feeding, and automation technologies to ensure optimal performance and compliance with industry standards.
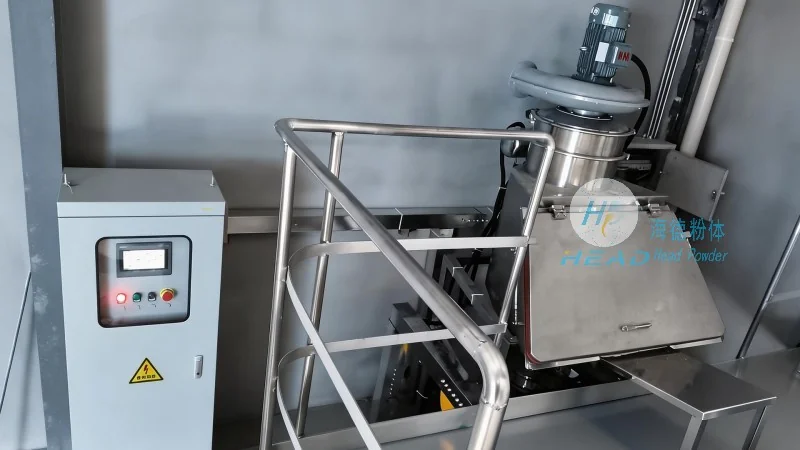
Working Principle of the Material Handling System
The core working principle of the tote bag dust-free loading station involves a multi-stage process that ensures efficient material transfer and minimal dust generation. Initially, the system receives a tote bag filled with bulk material. The bag is then positioned on a loading platform, which is equipped with a sealing mechanism to prevent dust leakage. Next, an automated conveyor or feeding mechanism extracts the material from the tote bag and directs it into a processing vessel or storage container. Simultaneously, a dust extraction system, typically integrated with the loading platform, captures any airborne particles, ensuring that the working environment remains clean and safe. The process is controlled by a programmable logic controller (PLC), which coordinates the movement of the tote bag, the feeding mechanism, and the dust extraction system to achieve precise and repeatable operations.
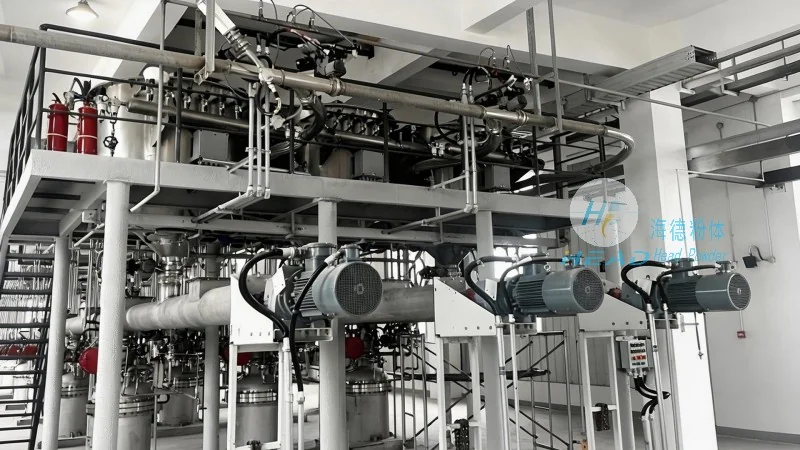
Key Features of the Tote Bag Dust-Free Loading Station
Our tote bag dust-free loading station material handling system is equipped with several key features that enhance its functionality and reliability. Firstly, the system incorporates a robust dust extraction system that uses high-efficiency particulate air (HEPA) filters to capture fine particles, ensuring that the air quality in the workspace meets stringent environmental standards. Secondly, the automated feeding mechanism is designed to handle a wide range of material types, including powders, granules, and bulk solids, with adjustable feeding rates to accommodate different processing requirements. Thirdly, the system features a user-friendly control interface, allowing operators to monitor and adjust the process parameters in real-time. Additionally, the design incorporates safety features such as emergency stop buttons and interlocks to prevent accidental exposure to dust or mechanical hazards. The system is also modular, enabling easy integration with existing production lines and scalability for future expansion.
Technical Specifications and Application Scenarios
The technical specifications of our tote bag dust-free loading station are tailored to meet the diverse needs of industrial applications. The system can handle tote bags with capacities ranging from 500 to 2000 liters, depending on the model. The feeding speed can be adjusted from 0.5 to 5 tons per hour, providing flexibility for different production volumes. The dust extraction system is capable of capturing particles as small as 0.3 microns, with an airflow rate of up to 2000 cubic meters per hour. The system operates on a standard 380V, 50Hz power supply, with a power consumption of approximately 15 kW. In terms of application scenarios, the system is widely used in pharmaceutical manufacturing for the transfer of active pharmaceutical ingredients (APIs), in food processing for the handling of powders like flour and sugar, and in chemical industries for the transfer of bulk chemicals. The system's ability to maintain a dust-free environment makes it suitable for applications where product purity and worker safety are critical.
Company Information and Service Commitment
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering high-quality, reliable material handling solutions to our clients. With our headquarters located in Shandong, China, we leverage over 20 years of industry experience to design and manufacture systems that meet the evolving needs of modern industries. Our team of engineers and technicians is dedicated to providing comprehensive support, from initial consultation and system design to installation, commissioning, and after-sales service. We pride ourselves on our ability to customize solutions to meet specific client requirements, ensuring that our systems not only enhance operational efficiency but also contribute to a safer and more sustainable working environment.




