Compound fertilizer material handling is a critical process in the agricultural and chemical industries, ensuring efficient movement of nutrient-rich materials from production to distribution. This article explores the working principle and key characteristics of compound fertilizer material transport systems, highlighting the technological advancements and operational efficiencies that define modern handling solutions.
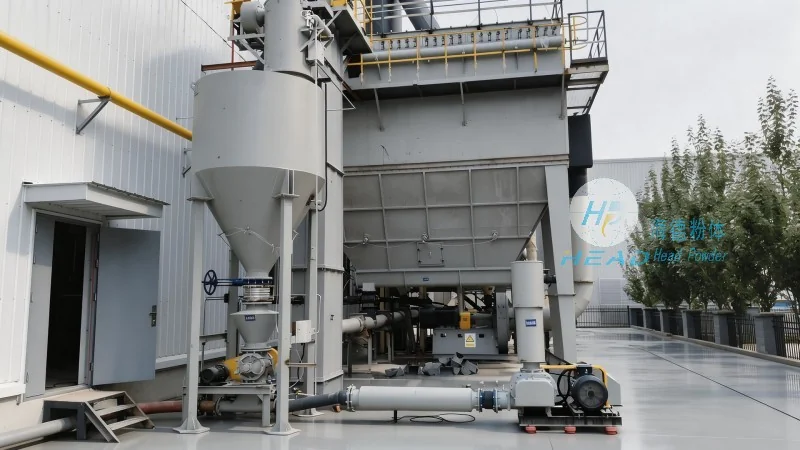
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized engineering solutions, is headquartered in Shandong, China. With a focus on innovation and quality, the company has established itself as a trusted partner in the development and implementation of advanced material handling systems for the fertilizer sector. Their expertise in designing and manufacturing tailored solutions has enabled them to meet the evolving needs of clients across various industrial applications.
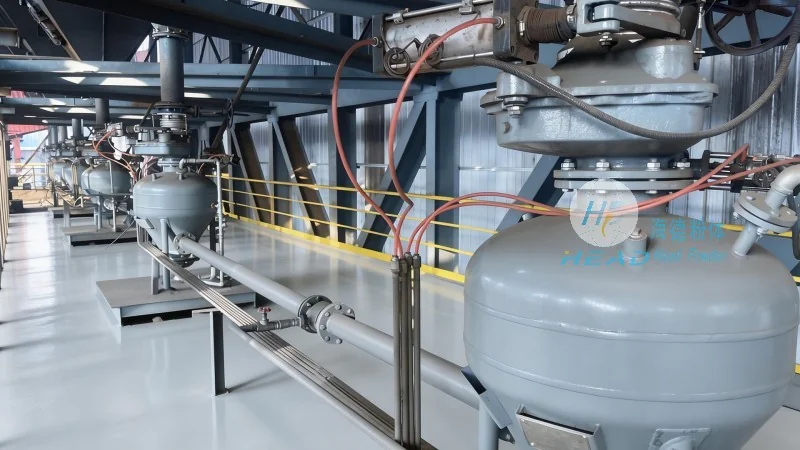
Working Principle of Compound Fertilizer Material Handling
The working principle of compound fertilizer material transport involves a systematic approach that integrates multiple components to ensure seamless material movement. At the core of the system are bulk material handling equipment such as conveyor belts, screw conveyors, and pneumatic systems, which are engineered to handle the specific properties of compound fertilizers, including their granular structure, moisture content, and bulk density. The process typically begins with material storage in silos or hoppers, where the fertilizer is collected and prepared for transport. From there, the material is transferred through a series of conveyors or pneumatic lines to the processing or packaging stages. Each component is designed to maintain the integrity of the fertilizer, preventing segregation or degradation during transit. The control systems, often equipped with sensors and automation, monitor the flow rate, pressure, and temperature to optimize performance and ensure safety. This integrated approach allows for a continuous and efficient workflow, minimizing downtime and maximizing throughput.
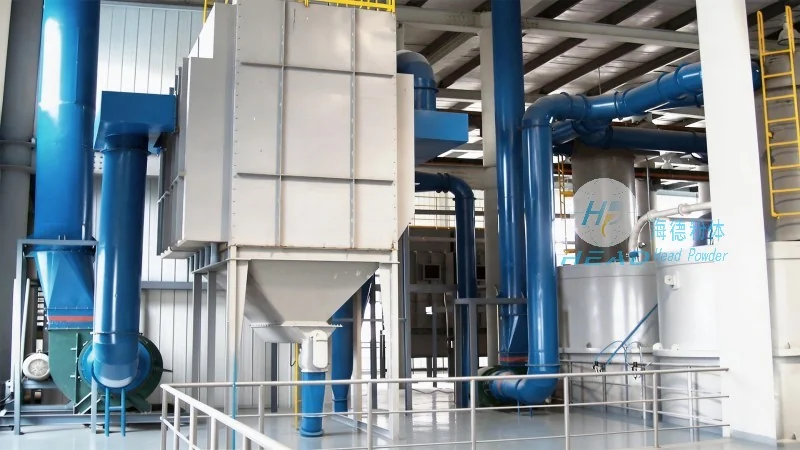
Key Characteristics of Compound Fertilizer Material Transport
Compound fertilizer material transport systems exhibit several distinct characteristics that make them suitable for industrial applications. One of the primary features is their high efficiency, which is achieved through the use of automated control systems and optimized equipment configurations. These systems can handle large volumes of material with minimal human intervention, reducing labor costs and increasing operational productivity. Another notable characteristic is the emphasis on safety and environmental protection. Modern transport solutions incorporate dust suppression mechanisms, sealed conveyor systems, and material containment measures to prevent environmental contamination and ensure worker safety. Additionally, the adaptability of these systems to different fertilizer types and processing requirements is a significant advantage. Whether handling standard NPK blends or specialized slow-release fertilizers, the equipment can be adjusted to accommodate varying material properties, ensuring consistent performance. The durability and reliability of the components are also critical characteristics, as they are exposed to harsh operating conditions and continuous use. High-quality materials and robust construction ensure long service life and minimal maintenance requirements, contributing to overall cost-effectiveness.
Technical Advancements in Material Handling Technology
Technological advancements have significantly enhanced the capabilities of compound fertilizer material transport systems. The integration of digital control systems and IoT (Internet of Things) sensors allows for real-time monitoring and data analysis, enabling predictive maintenance and performance optimization. Automated sorting and blending systems further improve the precision of material handling, ensuring consistent nutrient ratios in the final product. Additionally, energy-efficient designs, such as variable-speed drives and optimized airflow in pneumatic systems, reduce operational costs and environmental impact. The use of advanced materials, such as corrosion-resistant alloys and high-strength polymers, enhances the durability of equipment in corrosive environments commonly found in fertilizer processing. These advancements collectively contribute to more sustainable and efficient material handling solutions, aligning with industry standards and regulatory requirements.
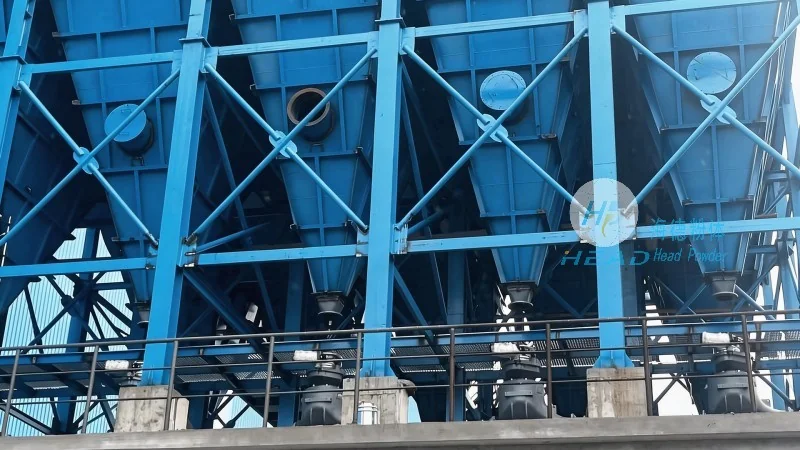
Application and Operational Benefits
The application of compound fertilizer material transport systems spans various stages of the fertilizer production and distribution chain. From raw material intake to final packaging, these systems play a vital role in maintaining the flow of operations. The operational benefits of implementing such systems include improved productivity, reduced material loss, and enhanced safety. By streamlining the material handling process, companies can achieve higher throughput rates and lower production costs. The reliability of modern systems also minimizes the risk of material spills or contamination, which is crucial for maintaining product quality and regulatory compliance. Furthermore, the scalability of these systems allows for easy expansion as production volumes increase, providing long-term value to the investment. The combination of efficiency, safety, and adaptability makes compound fertilizer material transport an essential component of modern fertilizer manufacturing and distribution operations.




