HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in providing advanced material conveying solutions for industries handling sorghum distillers grains. This article explores the working principles and key characteristics of systems designed to efficiently transport this specific agricultural byproduct.
Working Principle of Sorghum Distillers Grains Material Conveying Systems
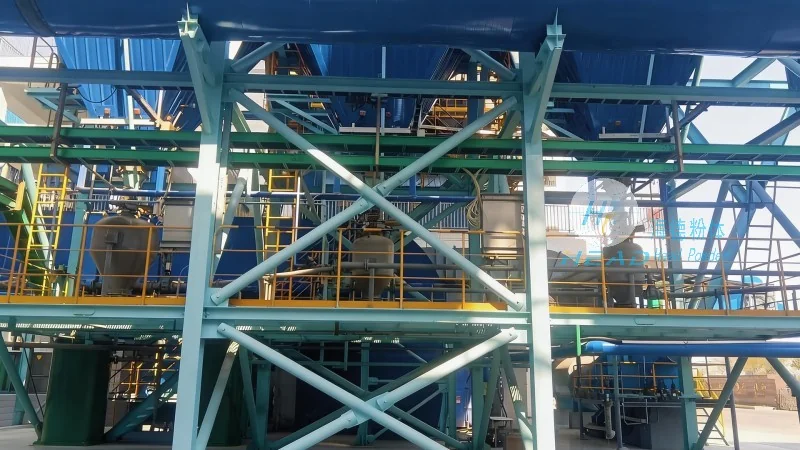
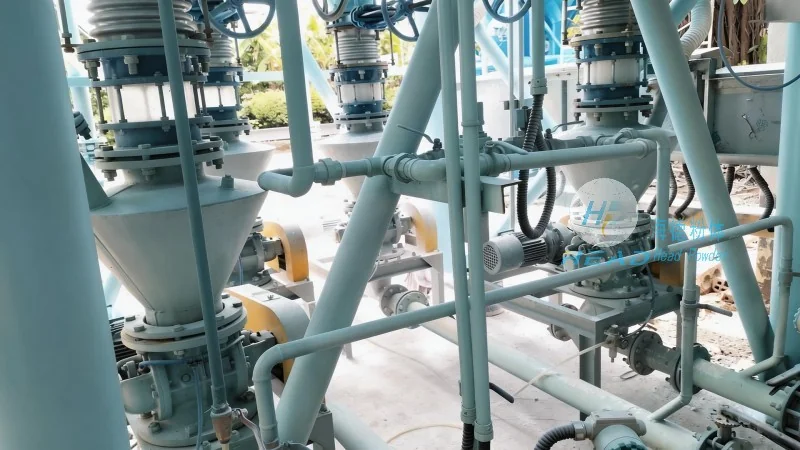
The core of sorghum distillers grains material conveying systems lies in their ability to handle bulk materials with precision and reliability. These systems typically incorporate a combination of mechanical components, such as belt conveyors, screw conveyors, and vertical lift mechanisms, tailored to the unique properties of distillers grains. The process begins with the collection of raw sorghum distillers grains, which are often in a semi-dry or wet state, requiring specialized equipment to prevent clogging and ensure smooth movement. Belt conveyors, for instance, use a continuous loop of rubber or fabric with attached flanges to transport materials horizontally or at slight inclines, while screw conveyors utilize a rotating helical screw to push material forward through a closed tube. Vertical lift systems, such as bucket elevators, are employed to move grains vertically, often integrating with horizontal conveyors to form a complete material handling line. The working principle emphasizes energy efficiency and minimal material degradation, as distillers grains are valuable feed ingredients and must be preserved during transport. Control systems, including variable frequency drives (VFDs) and sensors, regulate the speed and flow of the conveying process, adapting to changes in material volume and density. This automation ensures consistent performance and reduces operational costs.
Key Features of Sorghum Distillers Grains Material Conveying Solutions
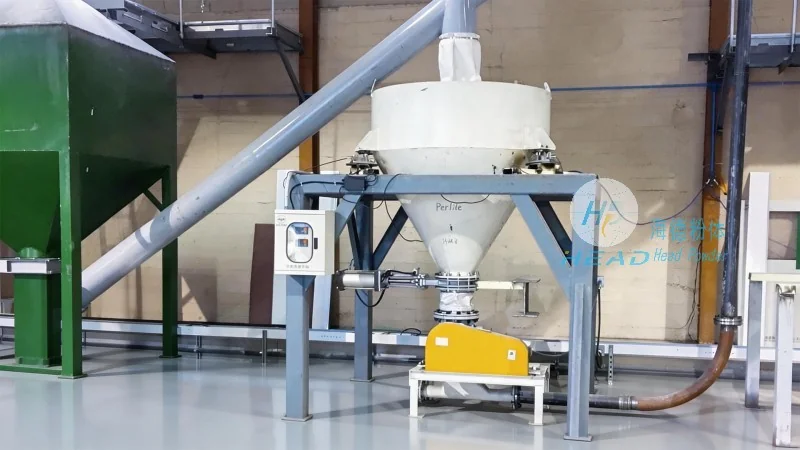
HeadPowder Engineering Co., Ltd. offers a range of features that enhance the functionality and durability of sorghum distillers grains material conveying systems. One of the primary advantages is the robust construction designed to withstand the abrasive nature of distillers grains, which can cause wear on traditional equipment. High-quality materials, such as stainless steel and heavy-duty rubber, are used in the construction of conveyor belts and components, extending the lifespan of the system. Additionally, the systems are engineered for high capacity, capable of handling large volumes of material with minimal downtime. This efficiency is crucial for industrial applications where continuous production is essential. The design also prioritizes hygiene and compliance with food safety standards, as distillers grains are used in animal feed and human nutrition. Sanitary features, including smooth surfaces and easy-to-clean components, are incorporated to prevent contamination. Another notable feature is the adaptability of the conveying systems, which can be customized to fit specific plant layouts and operational requirements. This flexibility allows HeadPowder to provide tailored solutions for clients, ensuring optimal performance in diverse industrial settings. Furthermore, the integration of advanced monitoring technology enables real-time tracking of material flow and system performance, facilitating proactive maintenance and reducing unexpected breakdowns. These features collectively contribute to the effectiveness and reliability of sorghum distillers grains material conveying solutions.
Application and Industry Impact
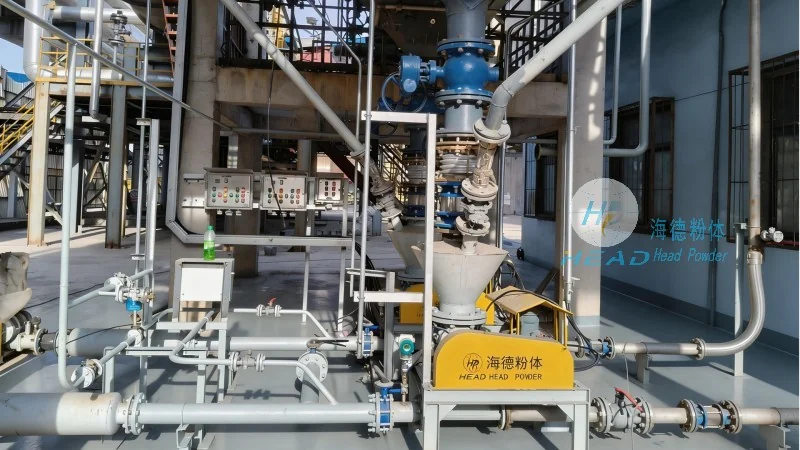
The efficient handling of sorghum distillers grains through specialized conveying systems has a significant impact on the distillery and feed processing industries. By ensuring smooth material transport, these systems support higher production throughput and reduce labor costs associated with manual handling. The consistent quality of the conveyed material also improves downstream processing, such as drying or pelletizing, leading to better product quality. HeadPowder Engineering Co., Ltd.'s solutions are particularly valuable in regions like Shandong, China, where the distillery industry is prominent. The company's commitment to innovation and customer-centric design has positioned it as a trusted partner for businesses seeking reliable material handling equipment. As the demand for sustainable and efficient processing methods grows, the importance of advanced conveying systems for sorghum distillers grains will continue to increase. These systems not only enhance operational efficiency but also contribute to environmental sustainability by minimizing waste and optimizing resource utilization. The combination of robust engineering, adaptability, and customer support makes HeadPowder Engineering Co., Ltd.'s solutions a preferred choice for industries handling this valuable byproduct.




