Positive pressure dense phase pneumatic conveying systems are advanced industrial equipment used for transporting bulk materials over long distances with high efficiency and minimal product degradation. These systems operate by forcing air or gas under pressure through a pipeline, carrying the material in a dense, particulate form rather than as a dilute cloud. This method offers significant advantages over traditional pneumatic conveying, including reduced product attrition, improved flow control, and the ability to handle a wide range of materials, from fine powders to granules and even bulk solids.
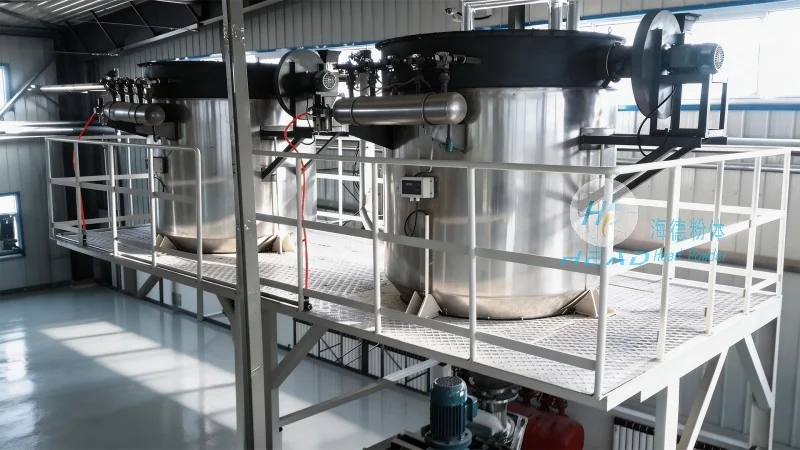
Key Features of Positive Pressure Dense Phase Pneumatic Conveying
The core feature of a positive pressure system is the continuous, high-pressure air flow that moves material through the pipeline. Unlike negative pressure systems, which draw material into the system, positive pressure systems push material forward, ensuring consistent flow and preventing backflow. This design allows for longer conveying distances and the ability to handle materials with higher moisture content or stickiness, as the dense phase reduces the risk of clogging and material separation.
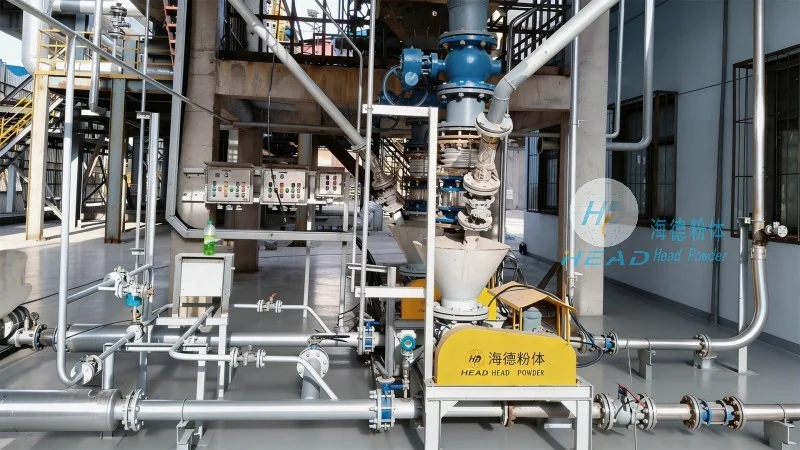
Design Principles of Positive Pressure Dense Phase Systems
The design of a positive pressure dense phase pneumatic conveyor involves several critical components and principles. The system typically includes a blower or compressor to generate the necessary air pressure, a hopper or feeder to introduce the material, a pipeline network to transport the material, and a discharge device to release the material at the destination. The key design principle is maintaining a dense phase flow, where the material particles are closely packed, reducing the air-to-material ratio and minimizing the velocity of the material. This is achieved by controlling the air pressure, flow rate, and material feed rate to ensure the material remains in a solid, non-entrained state.
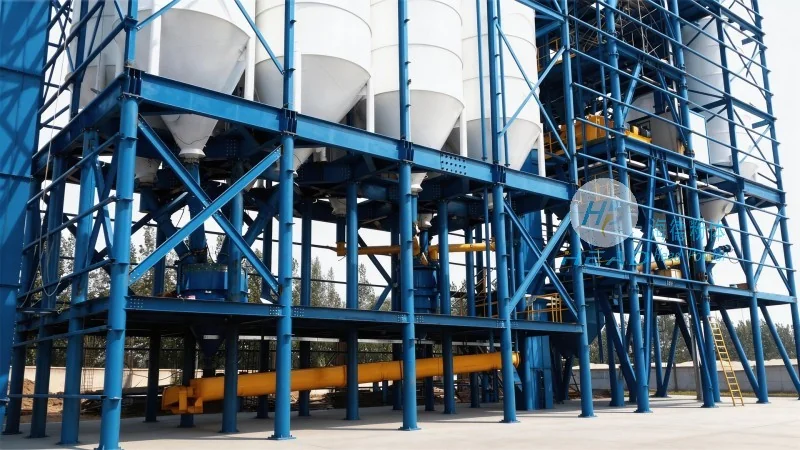
Advantages of Using Positive Pressure Dense Phase Conveying
Positive pressure dense phase pneumatic conveying offers numerous benefits for industrial applications. These include reduced product degradation due to lower particle velocities, improved material handling for sensitive or abrasive materials, and enhanced safety as the system operates under positive pressure, preventing dust emissions from the line. Additionally, the system can handle varying material characteristics, such as different particle sizes, densities, and flow properties, making it versatile for diverse industrial processes. The ability to transport materials over long distances without the need for intermediate storage or transfer points also contributes to operational efficiency and cost savings.
Applications in Industrial Settings
Positive pressure dense phase pneumatic conveyors are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, these systems are employed to transport ingredients like flour, sugar, and spices, ensuring product purity and minimal contamination. In pharmaceutical manufacturing, the system's ability to handle sensitive materials under controlled conditions is crucial for maintaining product quality and compliance with regulatory standards. The chemical industry utilizes these conveyors for transporting powders and granules, such as catalysts and pigments, while the mining sector applies them to move bulk materials like ores and coal from processing plants to storage or further processing facilities.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of advanced pneumatic conveying systems. With a focus on innovation and quality, the company specializes in designing and manufacturing positive pressure dense phase pneumatic conveyors tailored to meet the specific needs of industrial clients. HeadPowder's products are engineered to deliver high performance, reliability, and durability, ensuring efficient material handling while minimizing maintenance and operational costs. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge solutions for the global market.




