

Working Principle and Features of Automatic Bulk Bag Unloading Pneumatic Conveying Equipment for Pow
The automatic bulk bag unloading pneumatic conveying equipment is a critical piece of industrial machinery designed to efficiently handle the unloading and transportation of powders and granules from bulk bags (also known as big bags or FIBCs). This equipment streamlines the material handling process, reducing manual labor, minimizing dust exposure, and enhancing overall operational efficiency in various industries such as food processing, pharmaceuticals, chemicals, and construction materials.
Working Principle of the Equipment
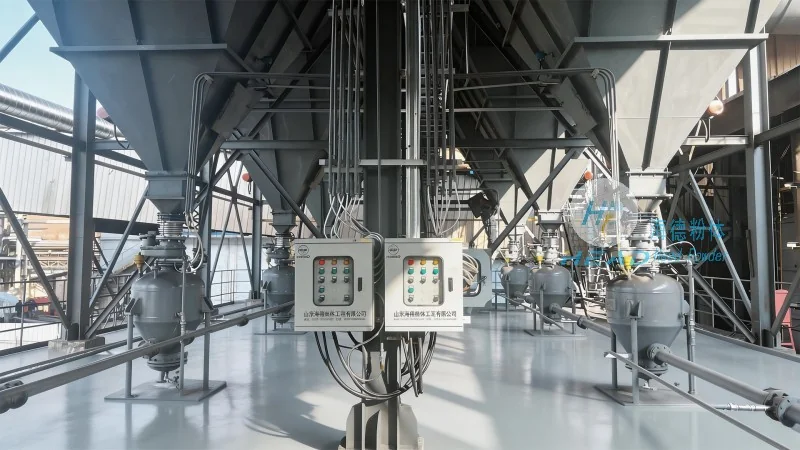
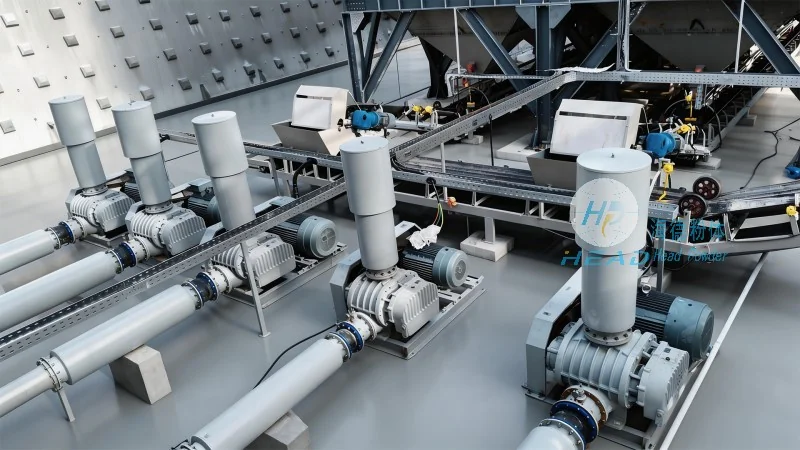
The operation of the automatic bulk bag unloading pneumatic conveying system involves several key steps. First, the bulk bag is placed onto a discharge hopper or frame, which is equipped with a sealing mechanism to prevent dust leakage. Once the bag is secured, the system initiates the unloading process by using a combination of vacuum or pressure to draw the material from the bag into a hopper or storage container. The pneumatic conveying component then transports the material through a pipeline network to the desired destination, such as a silo, storage tank, or processing unit. The system typically includes components like a bag emptying valve, a filter system to capture dust particles, and a control panel for automated operation. This integrated approach ensures a continuous and controlled flow of material, minimizing downtime and maximizing productivity.
Key Features and Advantages
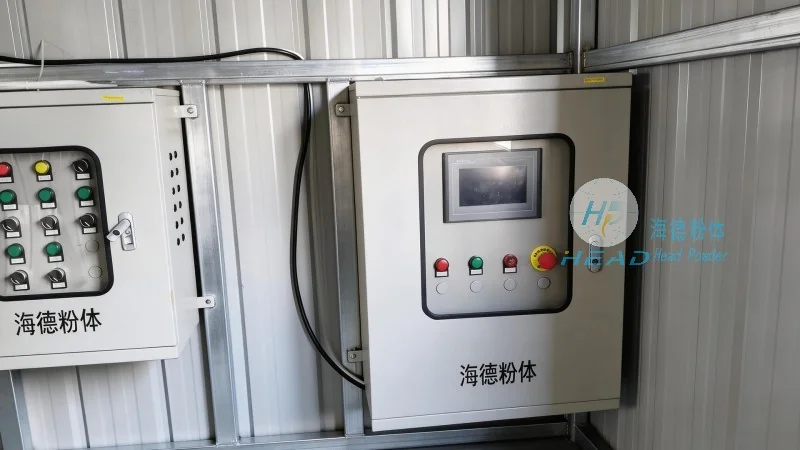
The automatic bulk bag unloading pneumatic conveying equipment offers several notable features and advantages that make it a preferred choice for industrial applications. One of the primary features is its fully automated operation, which eliminates the need for manual handling of heavy bulk bags, reducing the risk of workplace injuries and improving safety standards. The equipment is also designed for high efficiency, with the ability to handle large volumes of material quickly and consistently, thereby increasing production throughput. Additionally, the system incorporates advanced filtration technology to ensure that the material is conveyed in a clean and dust-free manner, which is particularly important in industries where product purity is critical, such as pharmaceuticals and food processing. Another key feature is the flexibility of the conveying system, which can be adjusted to accommodate different material types and bag sizes, providing versatility for various industrial needs. The equipment also includes user-friendly control systems that allow for easy monitoring and adjustment of the conveying process, enhancing operational control and reliability.
Company Information
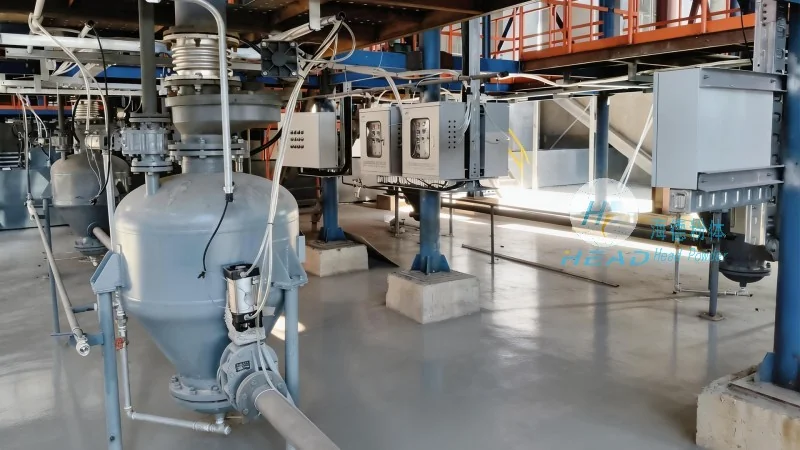
HeadPowder, a leading manufacturer of industrial material handling equipment, specializes in providing high-quality solutions for bulk bag unloading and pneumatic conveying applications. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the industry. The company is headquartered in Shandong, China, and leverages advanced engineering and manufacturing capabilities to deliver reliable and efficient equipment that meets the diverse needs of its clients. By focusing on quality, durability, and performance, HeadPowder ensures that its products deliver long-term value and contribute to improved operational efficiency for its customers.