Pharmaceutical pneumatic conveying equipment is a critical component in modern pharmaceutical manufacturing, enabling the efficient and hygienic transport of powders and granules within production lines. This equipment plays a vital role in ensuring product quality, maintaining sterile conditions, and enhancing overall operational efficiency in pharmaceutical facilities.
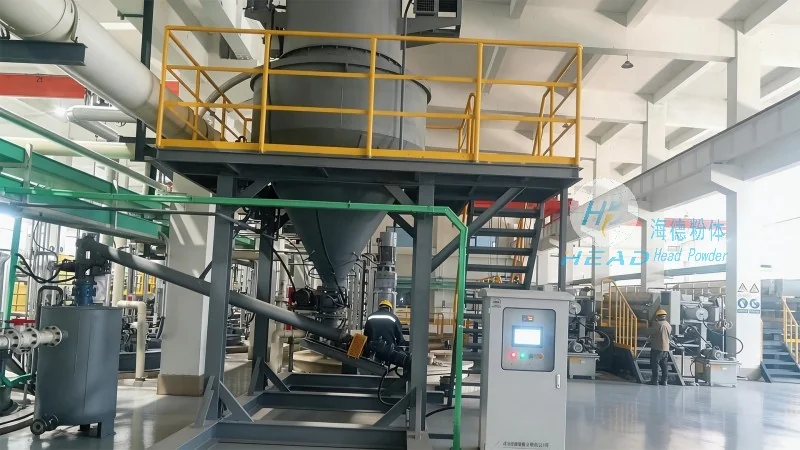
HeadPowder: A Leading Manufacturer of Pharmaceutical Pneumatic Conveying Systems
HeadPowder, the professional brand under Shandong HeadPowder Engineering Co., Ltd., is dedicated to providing high-quality, customized pneumatic conveying solutions tailored to the specific needs of the pharmaceutical industry. With a strong presence in Shandong, China, HeadPowder leverages advanced engineering and manufacturing capabilities to deliver reliable equipment that meets stringent regulatory requirements and industry standards.
Core Components and Structural Principles of Pharmaceutical Pneumatic Conveying Systems
The fundamental structure of a pharmaceutical pneumatic conveying system typically includes several key components, each designed to ensure optimal performance and compliance with industry regulations. These components work in concert to facilitate the safe and efficient movement of powders from one processing stage to another.
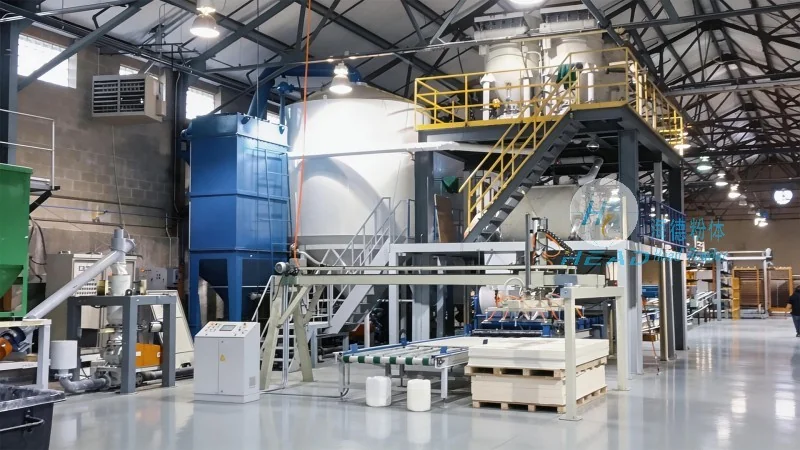
1. Conveying Lines and Tubing
The primary conduits for material transport are the conveying lines, which are constructed from materials such as stainless steel or food-grade plastic to ensure durability, corrosion resistance, and hygienic compatibility. The tubing is carefully designed with smooth inner surfaces to minimize particle buildup and ensure consistent airflow. In pharmaceutical applications, the choice of tubing material is critical, as it must withstand cleaning and sterilization processes without compromising product purity.
2. Air Supply and Control Systems
Air supply systems, including blowers or compressors, generate the necessary pressure and airflow to move the material through the conveying lines. These systems are equipped with advanced control mechanisms to regulate pressure, flow rate, and air volume, ensuring precise control over the conveying process. In pharmaceutical settings, air quality is paramount, and systems often incorporate filtration and drying units to remove contaminants and maintain a clean, dry environment for product handling.
3. Feeders and Hoppers
Feeders and hoppers are essential components that control the rate at which material is introduced into the conveying system. These devices ensure a consistent and controlled feed of powders, preventing overloading or underfeeding that could lead to inefficiencies or product degradation. In pharmaceutical applications, feeders are often designed with sanitary features, such as easy-to-clean surfaces and integrated cleaning mechanisms, to maintain compliance with GMP (Good Manufacturing Practice) standards.
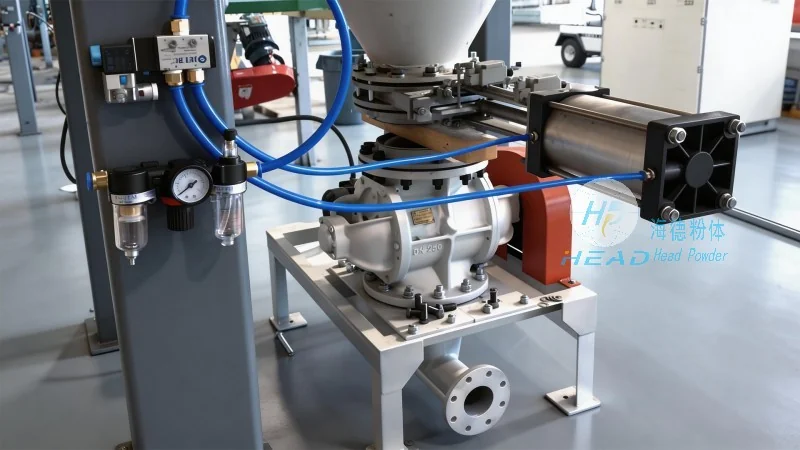
4. Separators and Filters
Separators and filters are critical for maintaining product purity and preventing material loss during the conveying process. These components capture fine particles and prevent them from being carried back into the system or contaminating downstream processes. In pharmaceutical pneumatic conveying systems, high-efficiency filters are used to ensure that only clean air and material are circulated, while also protecting equipment from clogging and damage.
5. Control and Monitoring Systems
Modern pharmaceutical pneumatic conveying systems are equipped with sophisticated control and monitoring systems that allow operators to track performance, detect anomalies, and adjust parameters in real-time. These systems may include sensors for pressure, flow, and temperature, as well as digital control panels for easy operation and data logging. The integration of advanced monitoring technology enhances process reliability and helps maintain consistent product quality throughout the manufacturing cycle.
Operational Principles and Benefits in Pharmaceutical Manufacturing
The operational principle of pharmaceutical pneumatic conveying involves the use of air to create a pressure differential that moves material through the system. This method offers several advantages over traditional mechanical conveying, including reduced risk of contamination, improved product handling in sterile environments, and the ability to transport materials over long distances without the need for multiple transfer points. The hygienic design of these systems, combined with their ability to maintain product integrity, makes them ideal for pharmaceutical applications where quality and safety are non-negotiable.
Customization and Compliance with Regulatory Standards
HeadPowder understands that each pharmaceutical facility has unique requirements, and therefore, offers customized pneumatic conveying solutions that are tailored to specific production needs. The company’s engineering team works closely with clients to design systems that meet not only operational demands but also stringent regulatory standards, such as those outlined by the FDA and other international health authorities. By adhering to GMP guidelines and industry best practices, HeadPowder ensures that its equipment contributes to a safe and compliant manufacturing environment.
Conclusion
Pharmaceutical pneumatic conveying equipment, with its robust structural design and advanced operational principles, is an indispensable tool in modern pharmaceutical manufacturing. HeadPowder, as a trusted manufacturer based in Shandong, China, continues to innovate and provide high-quality solutions that enhance efficiency, maintain product purity, and support regulatory compliance. By leveraging its expertise and commitment to quality, HeadPowder helps pharmaceutical companies achieve their production goals while upholding the highest standards of safety and reliability.




