Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design and production of advanced tonne bag packaging material conveying equipment. This equipment is engineered to efficiently handle bulk materials, ensuring smooth and reliable transportation from the source to the packaging point. The system integrates multiple components that work in tandem to achieve optimal performance, making it a critical solution for industries dealing with large volumes of powders or granules.
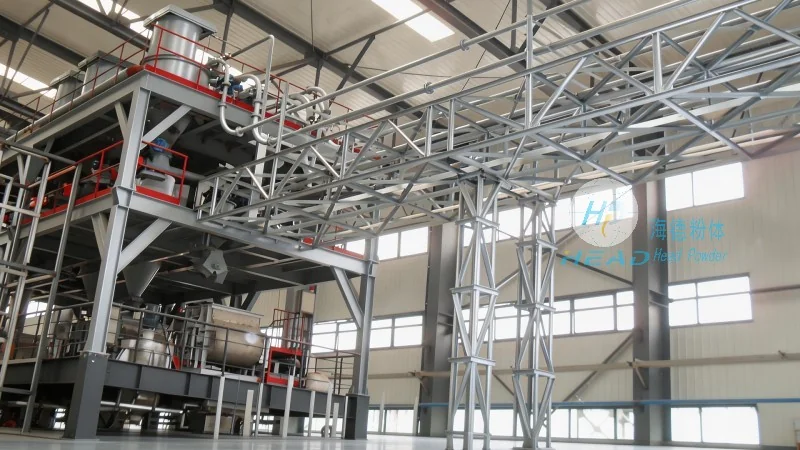
Key Components and Their Functions
The tonne bag packaging material conveying equipment typically consists of several key components, each playing a vital role in the overall operation. The primary components include the material hopper, which serves as the storage and feeding unit; the conveyor system, responsible for transporting the material; the control panel, which manages the operational parameters; and the discharge mechanism, which delivers the material into the tonne bags. Each component is designed with durability and efficiency in mind, ensuring long-term performance and minimal maintenance requirements.
Working Principle of the Conveying Process
The operation of the tonne bag packaging material conveying equipment begins with the material being loaded into the hopper. The material then flows into the conveyor system, which can be either a belt conveyor or a screw conveyor, depending on the specific application. The conveyor transports the material to the discharge point, where it is collected into tonne bags. The control panel monitors the flow rate, pressure, and other parameters to maintain consistent performance. The system is equipped with sensors and safety features to prevent overloading or blockages, ensuring safe and reliable operation.
Operation Process: Step-by-Step Guide
The operation process of the tonne bag packaging material conveying equipment involves several sequential steps. First, the material is fed into the hopper from the storage silo or bulk container. The hopper then regulates the flow of material into the conveyor. The conveyor transports the material to the discharge chute, which is positioned above the tonne bag. The control system adjusts the speed of the conveyor to match the packaging rate. As the tonne bag is filled, the system may include a mechanism to seal or tie the bag, ensuring it is properly sealed before being removed. The entire process is automated, reducing the need for manual intervention and increasing production efficiency.
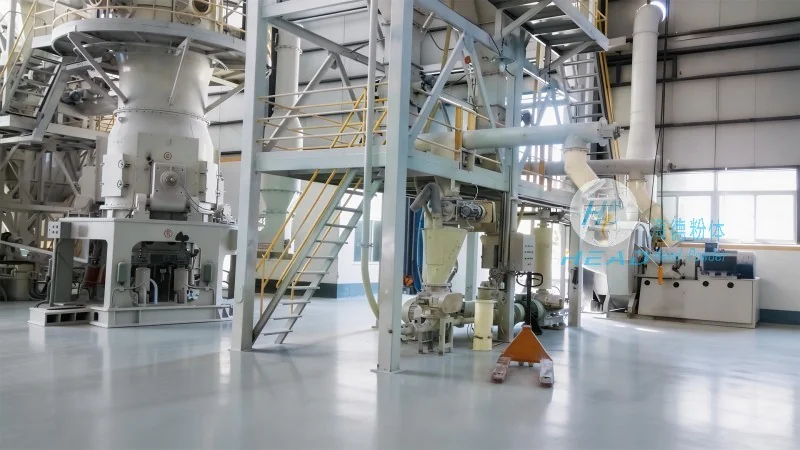
Advantages of Using Tonne Bag Packaging Material Conveying Equipment
Implementing tonne bag packaging material conveying equipment offers several advantages for industrial applications. Firstly, it enhances operational efficiency by automating the material handling process, reducing labor costs and increasing throughput. Secondly, the equipment ensures consistent material flow, minimizing variations in product quality and reducing waste. Thirdly, the system is designed for durability and low maintenance, providing long-term cost savings. Additionally, the equipment can be customized to meet specific material characteristics and production requirements, making it a versatile solution for various industries.
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd. provides high-quality tonne bag packaging material conveying equipment that meets the demands of modern industrial operations. With its advanced design and reliable performance, the equipment is ideal for industries such as mining, chemicals, and food processing. The company’s commitment to innovation and customer satisfaction ensures that clients receive tailored solutions that enhance their production processes. Based in Shandong, China, HeadPowder Engineering continues to lead the market with cutting-edge technology and superior customer service.




