Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading enterprise in the field of powder conveying technology, particularly specializing in systems for fly ash handling. With a strong commitment to innovation and quality, the company has developed advanced solutions tailored to the unique challenges of transporting fly ash from storage silos to various end-use applications. The fly ash silo powder conveying system is a critical component in power plant operations, ensuring efficient and safe material transfer while minimizing operational risks.
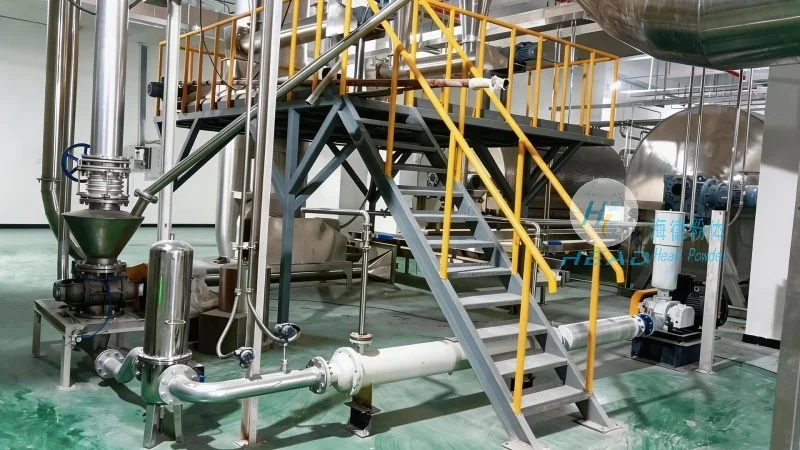
Overview of the Fly Ash Silo Powder Conveying System
The fly ash silo powder conveying system is engineered to handle the bulk transportation of fly ash, a byproduct of coal combustion, from large storage silos to processing units or disposal sites. This system integrates several key components, including a silo discharge mechanism, a conveyor system (such as pneumatic or mechanical conveyors), and a control panel for automated operation. The design prioritizes reliability, efficiency, and compliance with industrial safety standards, making it suitable for both new installations and retrofits in power generation facilities.
Step-by-Step Operation Process
The operation of the fly ash silo powder conveying system follows a systematic sequence to ensure smooth and continuous material transfer. The process begins with pre-operational checks, where the system's components are inspected for proper functionality and safety. This includes verifying the integrity of the silo, checking the conveyor's operational status, and ensuring that all electrical and pneumatic connections are secure. Once the pre-checks are completed, the system is initiated by the control panel, which activates the discharge mechanism in the silo to release the fly ash into the conveyor system.
During the conveying phase, the system uses either pneumatic or mechanical means to transport the fly ash through the pipeline network. Pneumatic systems utilize compressed air to create a flow that moves the powder, while mechanical systems employ screw conveyors or belt conveyors to physically move the material. The control panel continuously monitors key parameters such as pressure, flow rate, and temperature, adjusting the system's operation in real-time to maintain optimal performance. This monitoring ensures that any deviations from normal operation are detected promptly, allowing for immediate corrective actions to prevent system downtime or material loss.
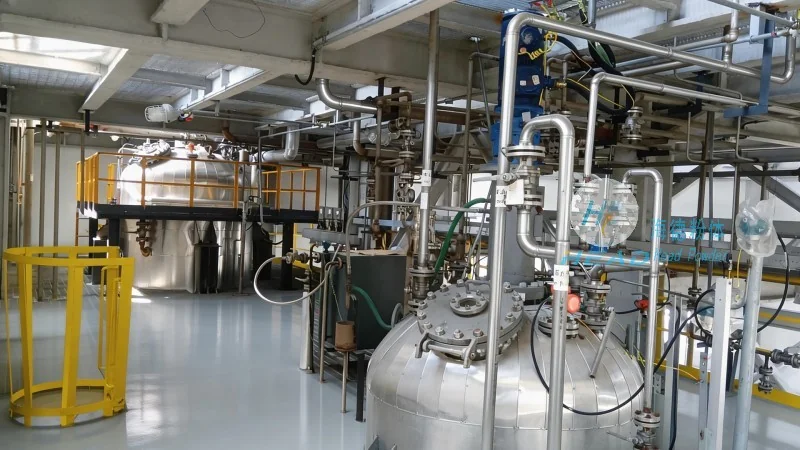
As the fly ash is conveyed, it passes through various valves and check points that regulate the flow and prevent backflow. These components are strategically placed to control the direction of material movement and to ensure that the system operates within safe pressure limits. The control panel also manages the speed of the conveyor, adjusting it based on the volume of fly ash being processed. This dynamic adjustment helps to maintain a consistent flow rate, reducing the risk of clogging or overloading the system.
Working Principle of Key Components
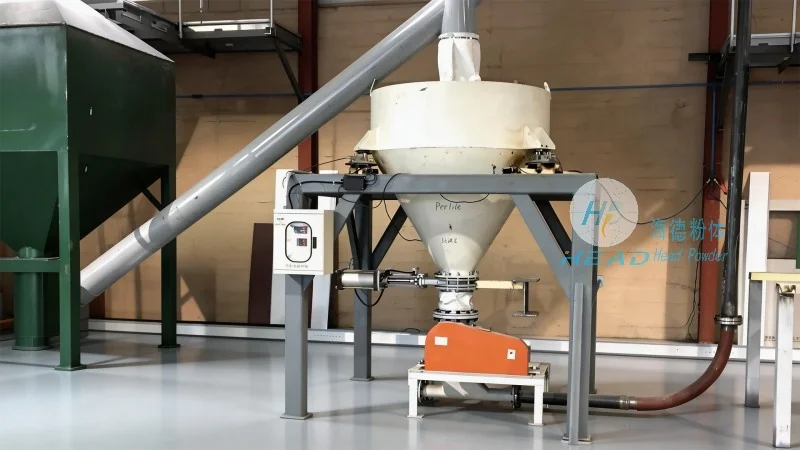
The effectiveness of the fly ash silo powder conveying system relies on the coordinated operation of several key components. The silo discharge mechanism, typically a rotary valve or a gate valve, is responsible for controlling the release of fly ash from the storage silo. This component ensures that the material is discharged at a controlled rate, preventing sudden surges that could damage the conveyor system or cause safety hazards. The conveyor itself, whether pneumatic or mechanical, is designed to handle the bulk density and flow characteristics of fly ash, which can vary depending on moisture content and particle size.
Pneumatic conveying systems operate by creating a pressure differential between the silo and the discharge point. Compressed air is introduced into the system, drawing the fly ash particles into the pipeline. The air velocity is carefully controlled to ensure that the particles remain suspended and move efficiently without causing excessive wear on the pipeline or components. Mechanical conveyors, on the other hand, use rotating screws or belts to push the fly ash through the system. These systems are often preferred for applications where high pressure or abrasive materials are involved, as they provide more direct control over the material flow.
The control panel is the brain of the system, integrating sensors, actuators, and software to manage the entire operation. It receives real-time data from various sensors, including pressure transducers, flow meters, and temperature sensors, and uses this information to adjust the system's parameters. The control panel also includes safety features such as emergency stop buttons and overload protection, which are critical for preventing accidents and ensuring compliance with industrial safety regulations. Additionally, the control panel may include a user interface that allows operators to monitor the system's status, adjust settings, and generate operational reports.
Advantages and Applications
The fly ash silo powder conveying system developed by Shandong HeadPowder Engineering Co., Ltd. offers several advantages that make it an ideal solution for power plants and other industrial facilities. One of the primary benefits is its high efficiency in transporting large volumes of fly ash with minimal operational downtime. The system's design minimizes material loss and reduces the risk of clogging, which can significantly impact productivity and increase maintenance costs. Additionally, the system is engineered for durability, with components made from materials resistant to corrosion and abrasion, ensuring long-term reliability and low maintenance requirements.
The system is widely used in power generation facilities where fly ash is a byproduct of coal combustion. It is also applicable in other industries, such as cement production, where fly ash is used as a supplementary cementitious material. The versatility of the system allows it to be adapted to various applications, from small-scale installations to large, high-capacity systems. The company's expertise in powder conveying technology ensures that the system is tailored to meet the specific needs of each client, providing customized solutions that enhance operational efficiency and safety.
In conclusion, the fly ash silo powder conveying system is a sophisticated and reliable solution for the efficient handling of fly ash. By integrating advanced components and control systems, the system ensures smooth and continuous operation, minimizing risks and maximizing productivity. Shandong HeadPowder Engineering Co., Ltd. continues to innovate in this field, providing high-quality systems that meet the evolving needs of the industrial sector. With its commitment to quality and customer satisfaction, the company remains a leader in the development of advanced powder conveying technologies.




