High-pressure bin pumps are critical equipment in material handling and transportation systems, particularly in industries that require efficient and reliable bulk material transport over long distances or challenging terrains. These systems are designed to handle a wide range of materials, from powders and granules to bulk solids, with precision and minimal loss. Understanding the underlying principles and the specific characteristics of their working scenarios is essential for optimizing operational efficiency and ensuring safety in industrial applications.
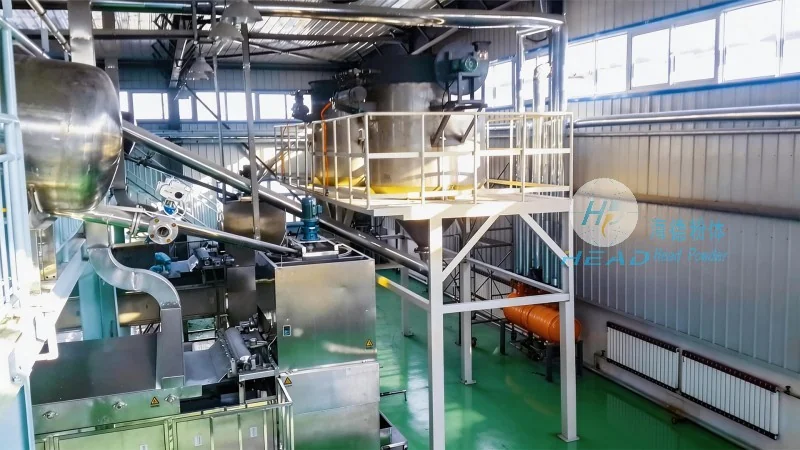
Introduction to High-Pressure Bin Pump Material Transport Systems
At the core of high-pressure bin pump systems is the ability to transfer bulk materials from a storage bin or hopper to a destination point, such as a processing plant, storage facility, or processing unit. The system typically consists of a pressure vessel (the bin), a pump mechanism, and a pipeline network. The bin is filled with the material, and the pump then generates the necessary pressure to force the material through the pipeline to the target location. This method is particularly advantageous in scenarios where traditional conveyor systems may be impractical due to space constraints, material characteristics, or the need for high-pressure transport.
The Working Principle of High-Pressure Bin Pumps
The operation of a high-pressure bin pump is based on the principle of pressure differentials and fluid dynamics. When the bin is filled with material, the pump creates a high-pressure environment within the system. This pressure is generated by either a mechanical pump or an air compressor, depending on the system design. The high-pressure air or fluid then acts as a carrier, pushing the material through the pipeline. The pump cycles between filling and discharging phases, maintaining a consistent flow rate and pressure to ensure smooth material transport. The system is equipped with valves and controls to regulate the pressure and flow, preventing backflow and ensuring that the material is delivered to the correct destination without interruption.
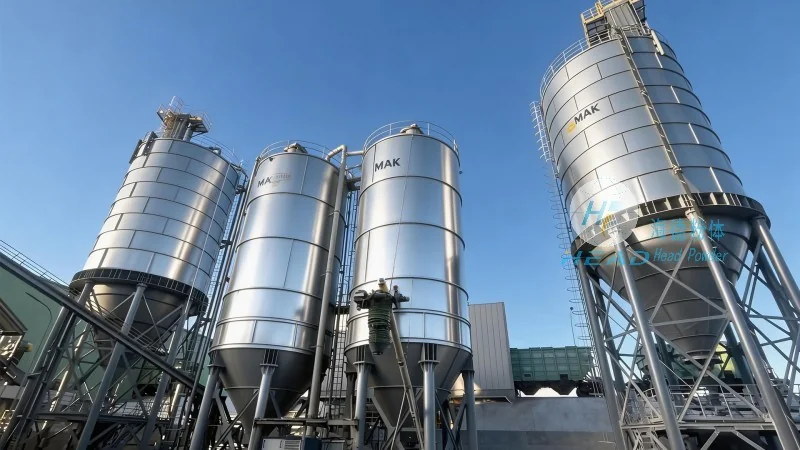
Key Features and Advantages in Working Scenarios
High-pressure bin pumps offer several key advantages that make them suitable for diverse working scenarios. One of the primary benefits is their ability to handle abrasive and corrosive materials without significant wear or damage to the equipment. The robust construction of the pump and the pipeline system ensures long-term durability, even in harsh industrial environments. Additionally, these systems are highly efficient in terms of energy consumption, as they use pressure to move materials rather than mechanical force, reducing operational costs over time. Another advantage is the flexibility in material handling, as the system can be adapted to transport various types of bulk materials, from fine powders to large granules, with minimal adjustments. This adaptability makes high-pressure bin pumps a versatile solution for different industrial applications.
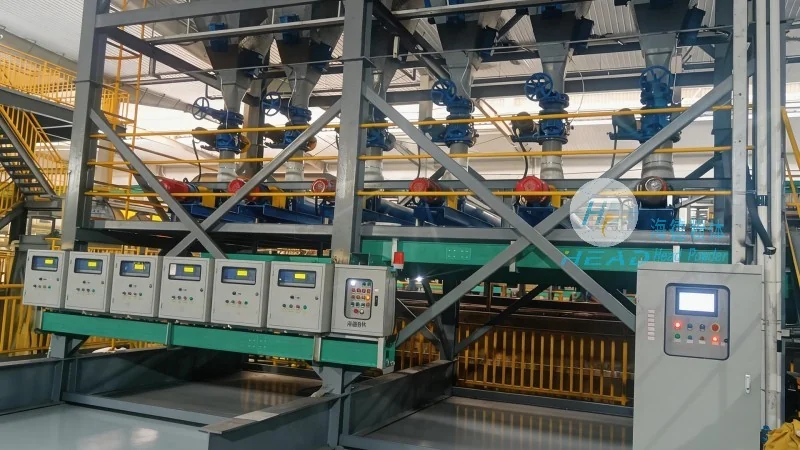
Application Scenarios and Industry Usage
High-pressure bin pumps are widely used in various industries, including chemical processing, mining, and food processing. In chemical plants, they are used to transport raw materials and finished products, ensuring that hazardous materials are handled safely and efficiently. In mining operations, these systems are crucial for transporting ore and other bulk materials from the mine to processing facilities, often over long distances and challenging terrains. The food processing industry also benefits from high-pressure bin pumps, as they can handle sensitive materials like grains and powders without compromising quality or safety. The system's ability to maintain consistent pressure and flow rates makes it ideal for applications where material quality and uniformity are critical.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of high-pressure bin pump material transport systems. With a strong presence in China, particularly in Shandong province, the company specializes in designing, manufacturing, and installing customized material handling solutions tailored to the specific needs of industrial clients. The company's headquarters and main operations are located in Shandong, China, where it leverages advanced technology and expertise to deliver high-quality products and services. Headpowder is committed to providing reliable and efficient material transport solutions that enhance operational productivity and safety for its clients, contributing to the success of various industrial sectors.




