HeadPowder, a leading provider in the field, specializes in advanced dust material conveying systems designed to efficiently transport bulk materials in industrial settings. These systems are engineered to handle a wide range of dusty or particulate materials, ensuring reliable and safe operation in various production environments. The core principles behind these systems revolve around the integration of mechanical components and control mechanisms that optimize material flow while maintaining operational efficiency.
Core Principles of the Conveying System
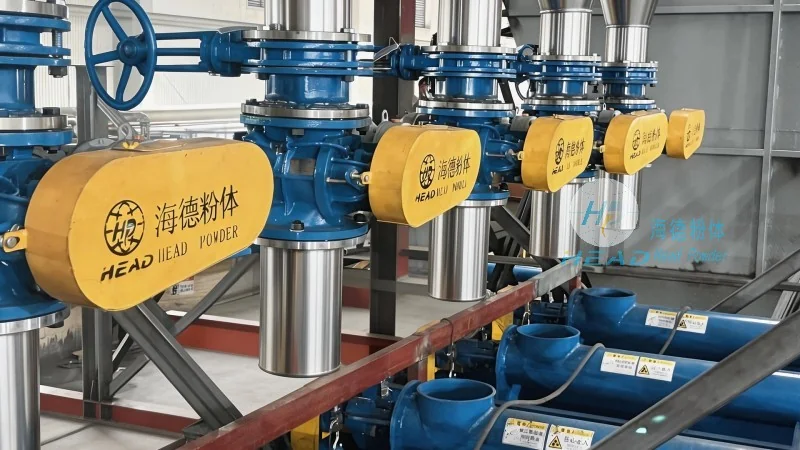
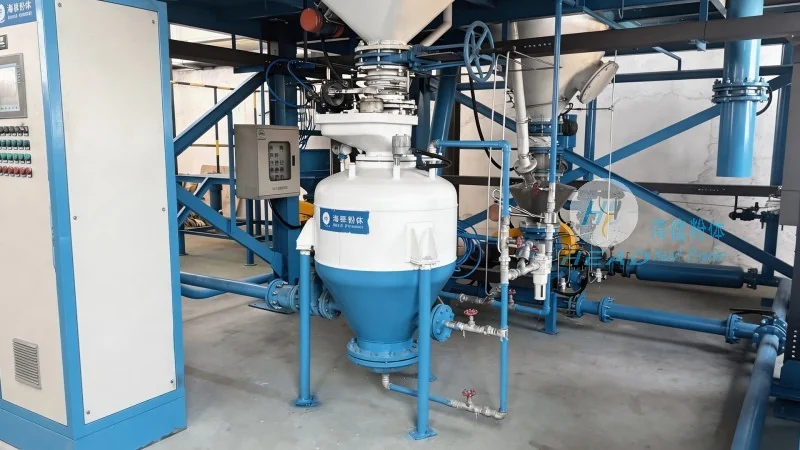
The fundamental principle of dust material conveying systems is the use of air or mechanical forces to move particulate materials from one location to another. In pneumatic conveying systems, for example, compressed air is used to create a flow that transports the material through pipelines. This method is particularly effective for handling fine powders and dusts, as it minimizes material degradation and contamination. Mechanical conveying systems, such as screw conveyors or belt conveyors, rely on rotating components to push or pull the material along a path. Both approaches are tailored to the specific characteristics of the material being transported, including particle size, density, and moisture content.
Working Scene Characteristics and Applications
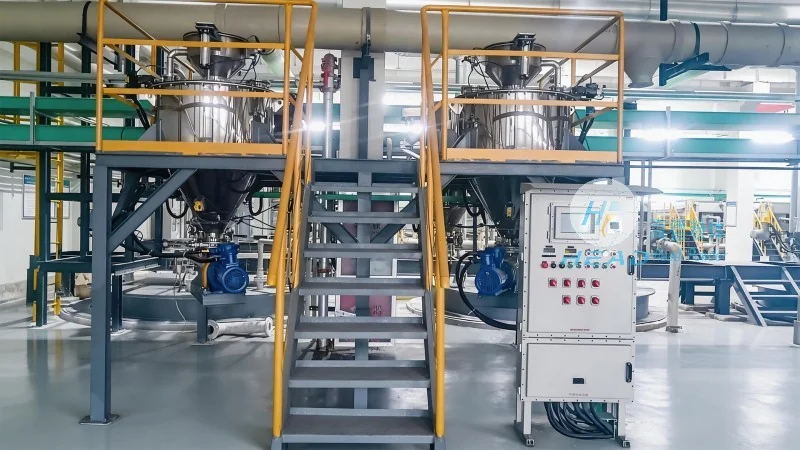
The working scene characteristics of dust material conveying systems are defined by their adaptability to diverse industrial environments. These systems are commonly used in industries like mining, cement production, chemical processing, and food processing, where the handling of bulk materials is essential. The key characteristics include high efficiency in material transport, low maintenance requirements, and the ability to operate in hazardous environments with dust or fumes. For instance, in cement plants, these systems are crucial for transporting raw materials and finished products, ensuring a continuous production flow. In chemical facilities, they help manage powders that may be reactive or sensitive to moisture, maintaining product quality and safety.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, as the company name suggests, is dedicated to engineering and manufacturing high-quality dust material conveying solutions. Based in Shandong, China, the company leverages years of industry experience to develop customized systems that meet the unique needs of each client. The company’s team of engineers and technicians works closely with clients to understand their operational requirements, ensuring that the final solution is both effective and cost-efficient. HeadPowder’s commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, which guarantee the reliability and durability of its products.
Key Features and Advantages
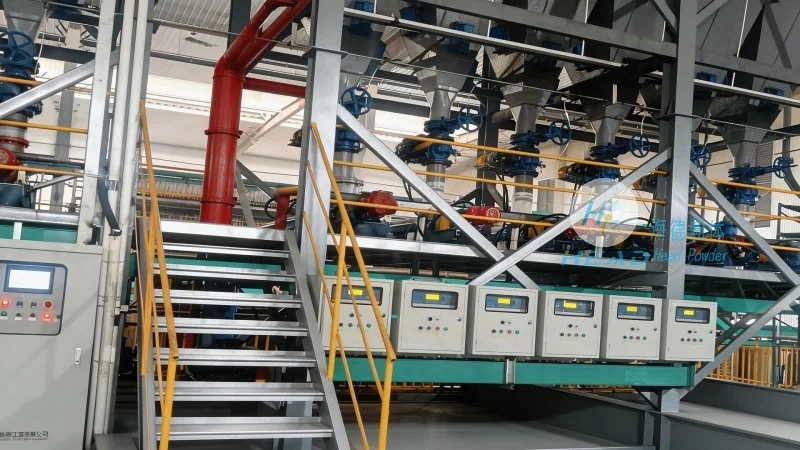
HeadPowder’s dust material conveying systems offer several advantages that set them apart in the market. These include energy efficiency, as modern systems are designed to minimize power consumption while maximizing material throughput. Additionally, the systems are equipped with advanced control systems that allow for real-time monitoring and adjustment, enhancing operational flexibility. Another key feature is the robust construction, which is built to withstand harsh industrial conditions, reducing downtime and maintenance costs. The company also provides comprehensive after-sales support, including installation, training, and maintenance services, ensuring that clients can fully utilize the system’s capabilities.




