

Working Principle and Features of Stone Powder Conveying Systems
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced stone powder conveying systems. These systems are engineered to efficiently transport bulk materials like crushed stone, sand, and other granular substances, playing a crucial role in various industrial applications. The following sections will delve into the working principle and key features of such systems, providing a comprehensive understanding of their functionality and benefits.
Working Principle of Stone Powder Conveying Systems
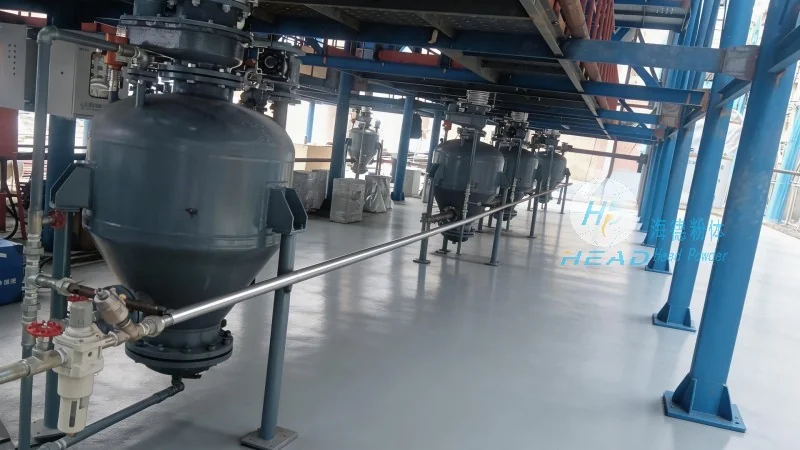
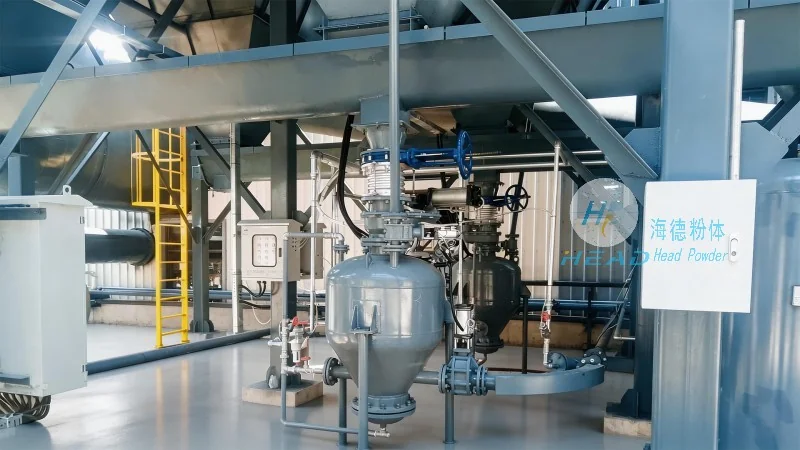
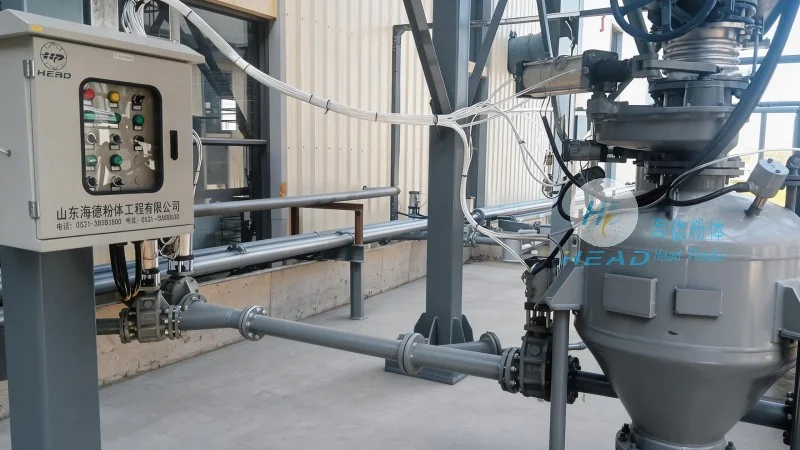
The stone powder conveying system operates through a series of integrated components that work in tandem to ensure smooth material transport. At its core, the system typically includes a hopper for material storage, a feeder to regulate the flow of powder, a conveyor mechanism (such as a screw conveyor, belt conveyor, or pneumatic system), and a control unit to manage the entire process. The hopper collects the stone powder, and the feeder ensures a consistent feed rate, preventing overloading or underfeeding. The conveyor then transports the material to the desired destination, such as a storage silo, processing unit, or packaging area. For pneumatic systems, compressed air is used to create a flow of air and material through pipes, while mechanical systems rely on rotating screws or belts to move the powder. The control unit monitors parameters like pressure, flow rate, and temperature, adjusting the system as needed to maintain optimal performance. This integrated approach ensures that the material is transported safely, efficiently, and with minimal loss or degradation.
Key Features and Advantages of Stone Powder Conveying Systems
HeadPowder's stone powder conveying systems are designed with several key features that enhance their performance and reliability. One of the primary advantages is their high efficiency in material handling, capable of transporting large volumes of stone powder at consistent rates. The systems are built with durable materials, such as stainless steel or high-grade alloys, to withstand the abrasive nature of the materials being conveyed, ensuring long service life and low maintenance costs. Another notable feature is the flexibility in system design, allowing customization to suit specific operational requirements, including different conveyor lengths, heights, and material types. The systems also incorporate advanced control technologies, enabling precise regulation of flow rates and pressure, which minimizes material degradation and reduces energy consumption. Additionally, the systems are equipped with safety features, such as overload protection and emergency stop mechanisms, to ensure safe operation and protect personnel and equipment. These features collectively make the stone powder conveying systems from HeadPowder reliable, efficient, and suitable for a wide range of industrial applications.