Pneumatic conveying, also known as air conveying, is a method used to transport bulk materials like powders and granules through a pipeline using air flow. This technology has become increasingly important in various industries, including agriculture, food processing, and manufacturing, due to its efficiency and flexibility. The core principle involves creating a pressure differential or using vacuum to move materials from one location to another without the need for mechanical components like belts or buckets. This approach not only reduces equipment wear and maintenance costs but also minimizes product contamination, making it ideal for handling sensitive materials such as wheat.
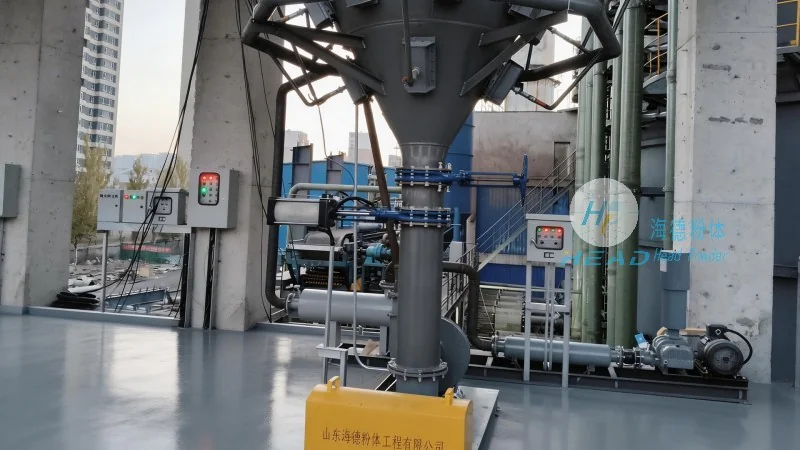
HeadPowder Engineering: A Leader in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a prominent manufacturer specializing in pneumatic conveying systems. With years of experience in the industry, HeadPowder has developed advanced solutions tailored to the unique needs of agricultural and food processing sectors. The company's commitment to innovation and quality has positioned it as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's expertise lies in designing and manufacturing custom pneumatic conveying systems that optimize material transport while ensuring compliance with industry standards and regulations.
Efficient Wheat Handling with Pneumatic Conveying Systems
For wheat processing facilities, pneumatic conveying offers a superior alternative to traditional methods such as bucket elevators or belt conveyors. The ability to transport wheat and other grain products through a closed system using air flow significantly reduces dust generation and product loss. This is particularly crucial in maintaining product quality and meeting stringent hygiene standards required in the food industry. HeadPowder's systems are engineered to handle the specific characteristics of wheat, including its density, moisture content, and flowability, ensuring smooth and continuous operation. The company's engineers work closely with clients to understand their operational requirements and design systems that maximize throughput while minimizing energy consumption.
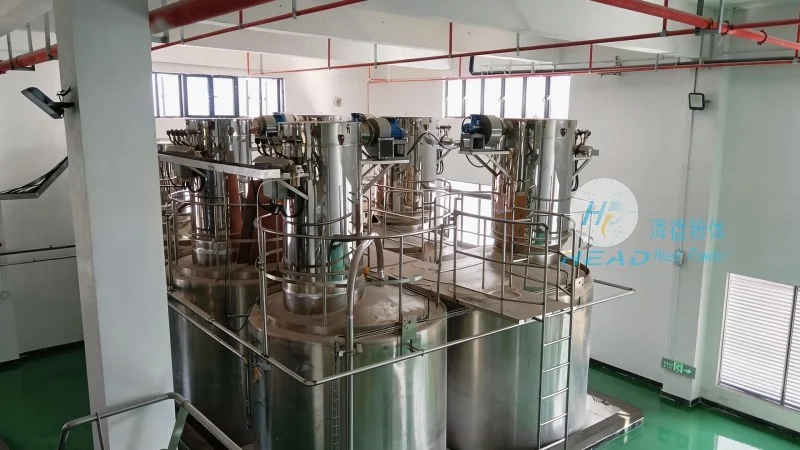
Key Advantages of Using Pneumatic Conveying for Wheat Transport
Implementing pneumatic conveying for wheat handling brings several key advantages. First, it enhances operational efficiency by reducing downtime caused by equipment maintenance and material blockages. Unlike mechanical conveyors, which are prone to wear and tear from abrasive materials, pneumatic systems have fewer moving parts, leading to lower maintenance costs and longer service life. Second, the closed pipeline design prevents dust and grain contamination, ensuring that the final product meets quality and safety standards. This is especially important for wheat destined for human consumption or animal feed. Third, pneumatic conveying systems offer flexibility in layout, allowing for vertical, horizontal, or inclined transport paths as needed. This adaptability makes it easier to integrate the system into existing production lines without major structural modifications. Additionally, the technology supports high-speed material transport, enabling faster processing and increased productivity in wheat processing plants.
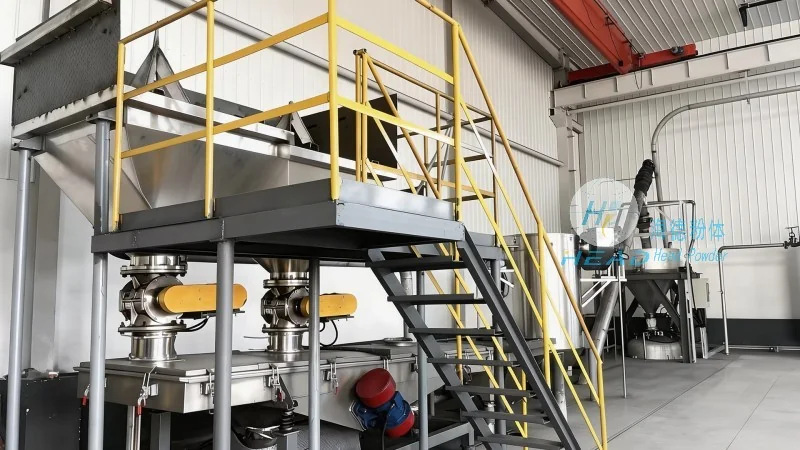
Customized Solutions for Diverse Wheat Processing Needs
HeadPowder Engineering understands that each wheat processing facility has unique requirements. Whether it's handling raw wheat, bran, or flour, the company provides customized pneumatic conveying solutions that address specific challenges. For example, in flour mills, the system can be designed to transport fine flour through a network of pipelines with minimal pressure drop, ensuring consistent flow rates. In grain storage facilities, pneumatic conveying can be used to transfer wheat from silos to processing equipment, reducing the need for manual handling and improving safety. The company's engineers also consider factors such as material moisture content and temperature, as these can affect the conveying efficiency and system performance. By tailoring the system design to the client's specific needs, HeadPowder ensures optimal performance and cost-effectiveness.
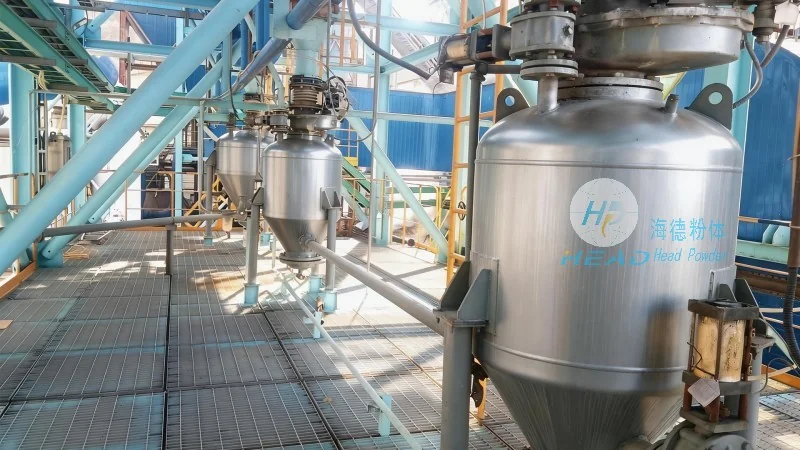
Ensuring Reliability and Durability in Pneumatic Conveying Systems
Reliability is a top priority for HeadPowder when designing pneumatic conveying systems for wheat transport. The company uses high-quality materials and components to construct the pipelines, valves, and other components, ensuring they can withstand the abrasive nature of wheat and other grain products. Stainless steel is commonly used for the internal surfaces of the conveying lines to prevent corrosion and maintain product purity. The system's control panels are equipped with advanced sensors and monitoring tools that provide real-time data on pressure, flow rate, and material level. This allows operators to quickly identify and address any issues, minimizing downtime and maximizing productivity. HeadPowder also offers comprehensive maintenance and support services to ensure the long-term reliability of its systems. Regular inspections and preventive maintenance are recommended to keep the equipment in optimal condition and extend its service life.
Conclusion: The Future of Wheat Handling with Pneumatic Conveying
As the demand for efficient and reliable material handling solutions continues to grow, pneumatic conveying technology remains a preferred choice for wheat processing facilities. HeadPowder Engineering, with its expertise and commitment to quality, is well-positioned to provide the industry with advanced pneumatic conveying systems that meet the evolving needs of wheat handling. By leveraging the benefits of air flow-based transport, businesses can enhance productivity, reduce costs, and maintain product quality. The future of wheat handling lies in innovative solutions like pneumatic conveying, and HeadPowder is at the forefront of this technological advancement.




