HeadPowder, a leading provider of industrial powder handling solutions, specializes in advanced small bag unpacking and conveying systems. Based in Shandong, China, the company has established itself as a trusted partner for businesses requiring efficient and reliable powder transport technologies. This article explores the working principle and key features of their small bag unpacking powder conveying systems, highlighting how these systems enhance operational efficiency and product integrity in various industrial applications.
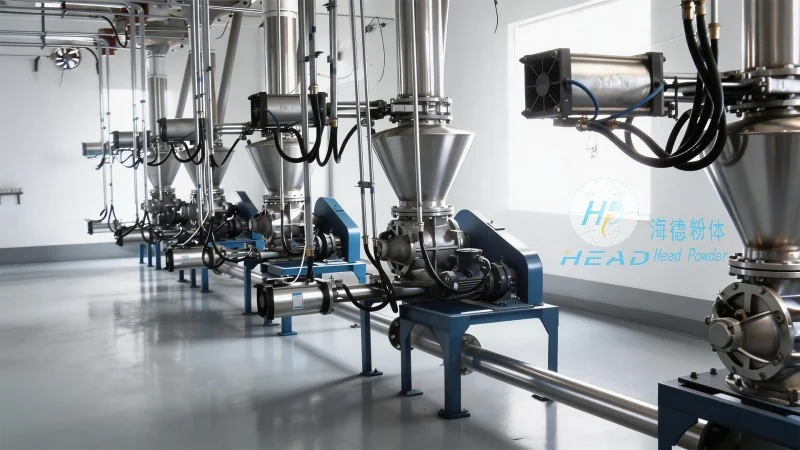
Introduction to Small Bag Unpacking Powder Conveying Systems
Small bag unpacking powder conveying systems are essential equipment for industries dealing with bulk powders, such as chemicals, food, pharmaceuticals, and minerals. These systems are designed to automate the process of transferring powders from sealed bags into a central storage or processing unit, eliminating manual handling and reducing the risk of contamination and material loss. HeadPowder’s systems are engineered to meet the diverse needs of different industries, offering customizable solutions that adapt to specific material properties and production requirements.
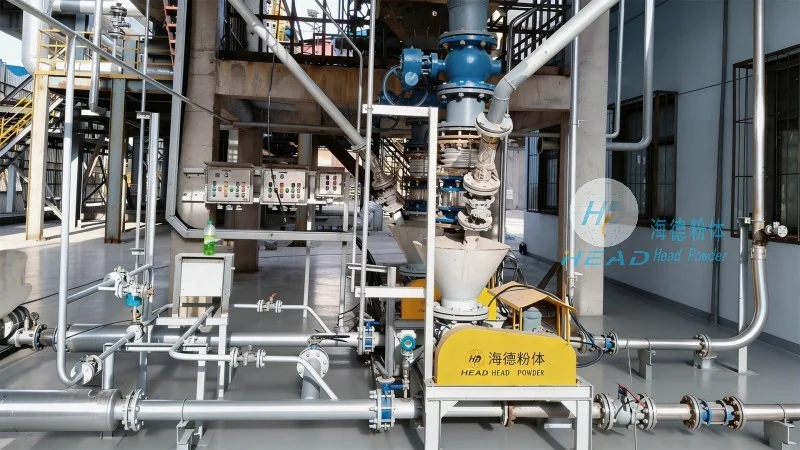
Working Principle of the Small Bag Unpacking Powder Conveying System
The core working principle of HeadPowder’s small bag unpacking powder conveying system involves a series of coordinated steps to ensure seamless material transfer. The process typically begins with the placement of a sealed bag onto a hopper or feeding mechanism. The system then uses a combination of mechanical and pneumatic components to open the bag, discharge the powder into a hopper, and transport it to the next stage of the production line. Key components include a bag opening device, a hopper with a discharge valve, a conveyor system (often a screw or pneumatic conveyor), and a control panel for automated operation. The system operates by first activating the bag opening mechanism, which may involve cutting or tearing the bag seal, followed by the use of a vacuum or pressure system to draw the powder from the bag into the hopper. Once the powder is in the hopper, the discharge valve opens, and the conveyor transports the material to the desired destination, such as a silo, mixer, or processing unit. The entire process is controlled by a programmable logic controller (PLC), which ensures precise timing and consistent performance. This automated approach minimizes human intervention, reduces labor costs, and enhances safety by eliminating direct contact with powders and potential hazards associated with manual bag handling.
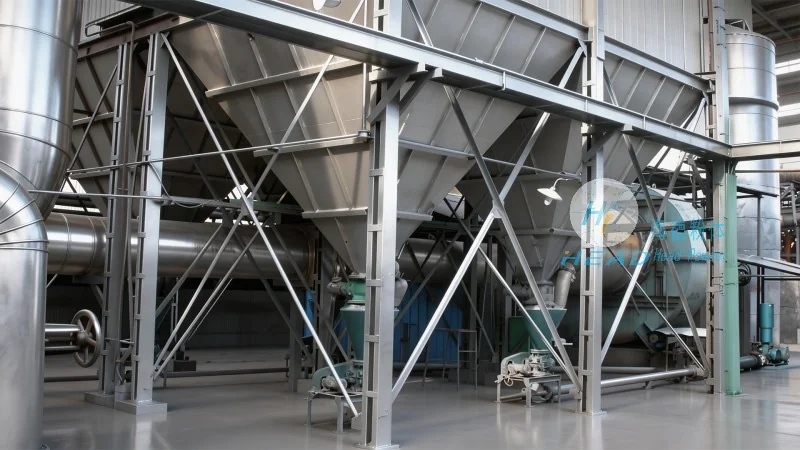
Key Features of the Small Bag Unpacking Powder Conveying System
HeadPowder’s small bag unpacking powder conveying systems are characterized by several advanced features that set them apart from conventional solutions. These features are designed to improve efficiency, reliability, and user experience. First, the system incorporates a robust bag opening mechanism that can handle various bag types, including polyethylene, paper, and composite bags, with minimal damage to the material. This ensures that the powder remains intact and free from contaminants during the opening process. Second, the hopper design is optimized for material flow, featuring a conical or rectangular shape with smooth internal surfaces to prevent powder buildup and caking. The discharge valve is equipped with a sealing mechanism to prevent dust emissions and maintain a clean working environment. Third, the conveying system uses a low-speed, high-capacity design, such as a screw conveyor or pneumatic pipeline, which minimizes product degradation and ensures consistent flow rates. The screw conveyor, for example, provides gentle material handling, reducing the risk of agglomeration or particle breakage, which is critical for sensitive powders. Fourth, the system includes an integrated dust collection and filtration system to capture any airborne particles, ensuring compliance with environmental regulations and maintaining a safe workplace. This feature not only improves air quality but also prevents product loss and contamination. Fifth, the control panel offers user-friendly interfaces, including touchscreens and programmable settings, allowing operators to adjust parameters such as conveyor speed, bag opening time, and discharge rate. This flexibility enables the system to adapt to different production volumes and material characteristics. Finally, the system is constructed with high-quality materials, such as stainless steel and corrosion-resistant components, to withstand harsh industrial environments and ensure long-term durability. These features collectively contribute to a system that is efficient, reliable, and easy to maintain, making it an ideal choice for businesses seeking to optimize their powder handling processes.
Benefits of Implementing Small Bag Unpacking Powder Conveying Systems
The adoption of small bag unpacking powder conveying systems by industrial companies brings numerous benefits that enhance operational performance and profitability. One of the primary advantages is the significant reduction in labor costs. By automating the bag opening and powder transfer process, businesses can eliminate the need for manual labor, which not only reduces labor expenses but also minimizes the risk of workplace injuries associated with handling heavy bags and powders. Another key benefit is the improvement in product quality and consistency. The automated system ensures that powders are handled gently and consistently, reducing the risk of contamination, agglomeration, or particle degradation. This leads to higher product quality and fewer defects, which can enhance customer satisfaction and brand reputation. Additionally, the system enhances operational efficiency by reducing downtime and increasing throughput. The automated process allows for continuous operation, with minimal interruptions for bag changes or maintenance, leading to higher production rates and better resource utilization. Furthermore, the system improves workplace safety by eliminating direct contact with powders and reducing the risk of dust explosions or respiratory issues. The integrated dust collection system and sealed components help maintain a safe working environment, reducing the need for personal protective equipment (PPE) and associated costs. Finally, the system offers long-term cost savings through reduced material loss and lower maintenance requirements. By minimizing product spillage and preventing caking or buildup in the hopper and conveyor, the system reduces waste and extends the lifespan of components, leading to lower operational costs over time. These benefits make small bag unpacking powder conveying systems a valuable investment for businesses looking to streamline their operations and improve overall performance.
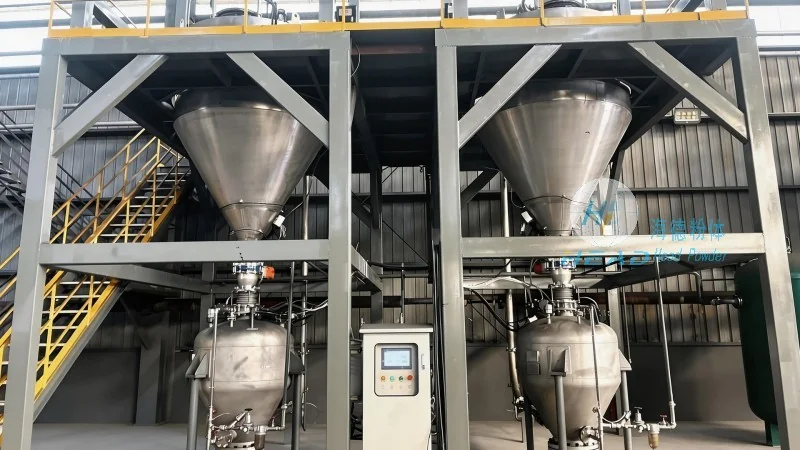
Conclusion
HeadPowder’s small bag unpacking powder conveying systems represent a sophisticated solution for efficient and reliable powder handling in various industrial applications. By combining advanced mechanical and pneumatic components with automated control systems, these systems offer a seamless and safe way to transfer powders from sealed bags into processing units. The key features, including robust bag opening mechanisms, optimized hopper designs, gentle conveying systems, integrated dust collection, and user-friendly controls, ensure that the systems are efficient, reliable, and adaptable to diverse material and production needs. The benefits of implementing these systems, such as reduced labor costs, improved product quality, enhanced operational efficiency, and better workplace safety, make them an attractive choice for businesses seeking to optimize their powder handling processes. With a strong presence in Shandong, China, HeadPowder continues to provide high-quality industrial solutions that meet the evolving needs of the industry, helping businesses achieve greater productivity and profitability.




