

What is a Quartz Stone Powder Pneumatic Conveying System? What Are Its Design Principles?
Quartz stone powder, a widely used material in various industrial applications, often requires efficient and reliable transportation methods to move it from one location to another. This is where a quartz stone powder pneumatic conveying system comes into play. Such systems are engineered to handle the unique properties of quartz stone powder, ensuring safe, efficient, and cost-effective material transport. In this article, we will explore what these systems are and delve into their fundamental design principles.
Understanding Quartz Stone Powder Pneumatic Conveying Systems
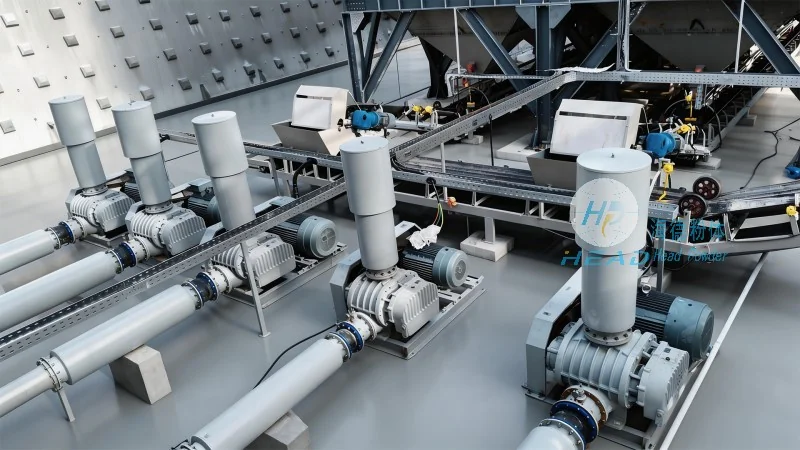
A quartz stone powder pneumatic conveying system is a type of material handling equipment that uses compressed air or other gas to transport dry powders, including quartz stone powder, through a pipeline network. The system typically consists of a blower or compressor to generate the necessary air pressure, a hopper or feeder to introduce the powder into the system, and a series of pipes and valves to direct the material flow. The primary goal of such a system is to move the powder from a source point to a destination point without the need for mechanical components like conveyors or buckets, which can be prone to wear and maintenance issues.
The Core Components of a Pneumatic Conveying System
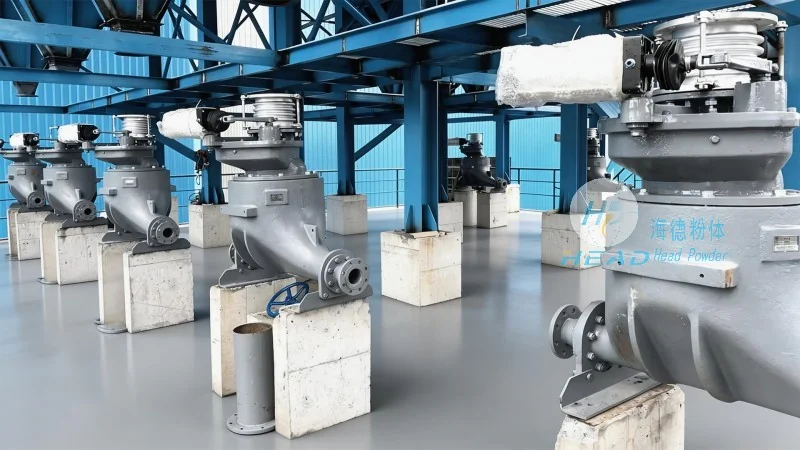
At the heart of any quartz stone powder pneumatic conveying system are several key components that work in tandem to ensure optimal performance. The first is the air source, which can be a rotary lobe blower or a positive displacement blower, depending on the system's requirements. These devices generate the high-pressure air needed to move the powder through the system. Next, the material feed system, often a hopper or a rotary valve, is responsible for introducing the quartz stone powder into the pipeline. The hopper is designed to hold a sufficient quantity of powder and can be equipped with a level indicator to monitor the material volume. The rotary valve, on the other hand, provides a controlled and consistent feed rate, preventing overloading or underfeeding of the system.
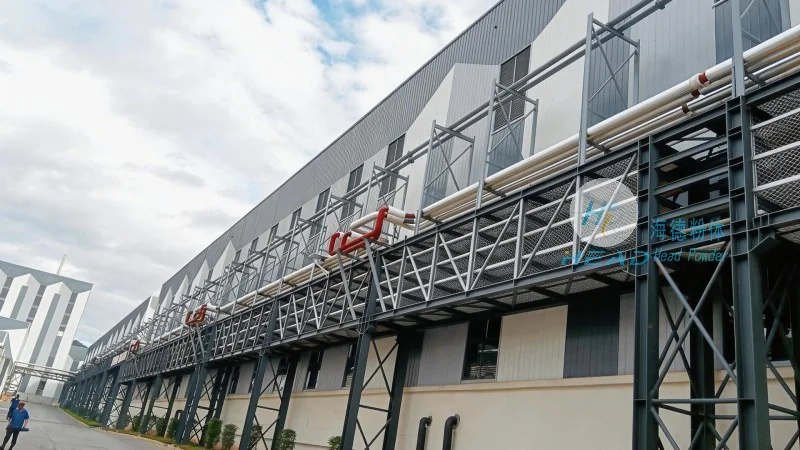
Following the feed system are the conveying lines, which are typically made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of quartz stone powder. The pipeline network includes elbows, tees, and other fittings that direct the flow of powder and air. To control the flow and pressure within the system, various valves are used, such as butterfly valves, gate valves, or check valves. These valves allow operators to adjust the system's performance based on the specific needs of the application.
Design Principles for Efficient Pneumatic Conveying
The design of a quartz stone powder pneumatic conveying system is governed by several critical principles aimed at maximizing efficiency, minimizing energy consumption, and ensuring the longevity of the equipment. One of the most important principles is the selection of the appropriate air velocity. The air velocity must be high enough to keep the powder particles suspended in the air stream but not so high that it causes excessive wear on the system components or leads to high energy consumption. Typically, the air velocity is maintained between 20 to 30 meters per second for most quartz stone powder applications.
Another key design principle is the system's pressure drop. The pressure drop across the conveying line is a measure of the energy required to move the powder through the system. A well-designed system minimizes this pressure drop by using smooth, straight pipes and avoiding unnecessary bends or obstructions. This reduces the load on the air source and lowers operational costs. The system's design also considers the particle size and density of the quartz stone powder, as these factors influence the required air velocity and pressure. Larger or denser particles may require higher air velocities to ensure proper suspension.
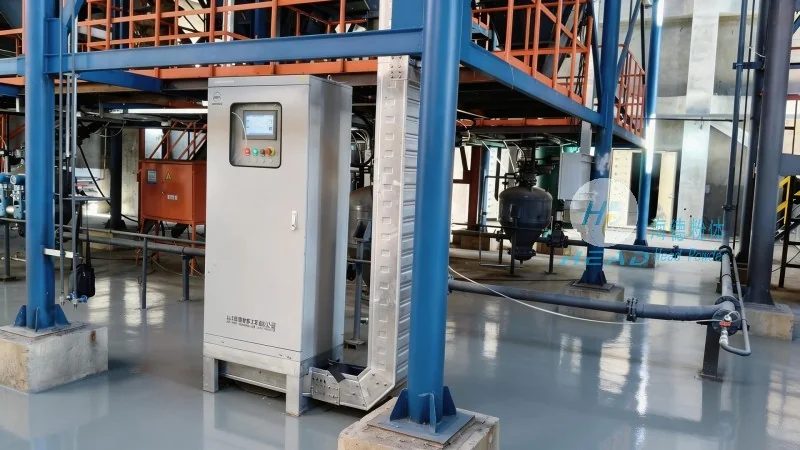
Furthermore, the system's layout and configuration are critical to its performance. The distance between the feed point and the discharge point, the number of bends and fittings, and the overall pipeline length all impact the system's efficiency. A well-planned layout minimizes the number of bends and uses larger diameter pipes where necessary to reduce pressure losses. The use of pulse jet or other cleaning mechanisms is also considered in the design to prevent clogging, which is a common issue with abrasive materials like quartz stone powder.
Applications and Benefits of Quartz Stone Powder Pneumatic Conveying Systems
Quartz stone powder pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. These systems are commonly employed in the construction industry for transporting quartz stone powder used in concrete and mortar production. They are also used in the pharmaceutical and food industries, where the need for a clean and hygienic material handling system is paramount. In the chemical industry, such systems are used to transport quartz stone powder used as a filler or abrasive in various products.
The benefits of using a pneumatic conveying system for quartz stone powder are numerous. First, it offers a dust-free operation, which is crucial in environments where dust can be a health hazard or cause equipment damage. Second, the system is compact and can be installed in tight spaces, making it suitable for facilities with limited floor space. Third, it reduces maintenance costs compared to traditional mechanical conveyors, as there are fewer moving parts and less wear and tear. Finally, the system can be easily integrated with other equipment, such as mixers or processing units, to create a seamless production line.
Conclusion and Company Overview
In conclusion, a quartz stone powder pneumatic conveying system is a sophisticated and efficient solution for transporting quartz stone powder in various industrial applications. The design principles behind these systems focus on optimizing air velocity, minimizing pressure drop, and ensuring the proper handling of the material's properties. By understanding these principles and selecting the right components, industries can achieve reliable and cost-effective material transport.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in designing and manufacturing high-quality quartz stone powder pneumatic conveying systems. With years of experience and a commitment to quality, the company provides tailored solutions to meet the specific needs of its clients. HeadPowder's systems are engineered to deliver superior performance, durability, and efficiency, ensuring that clients can rely on them for years to come. Based in Shandong, China, HeadPowder serves a global market, providing innovative solutions for material handling challenges in various industries.