When it comes to transporting fine coal powder, the choice of conveying method is critical for efficiency, safety, and operational reliability. Pneumatic conveying stands out as a highly effective solution, offering unique advantages that address the challenges posed by fine particulate materials. This article explores the significance of pneumatic conveying in the context of fine coal powder transportation, highlighting its benefits and practical applications.
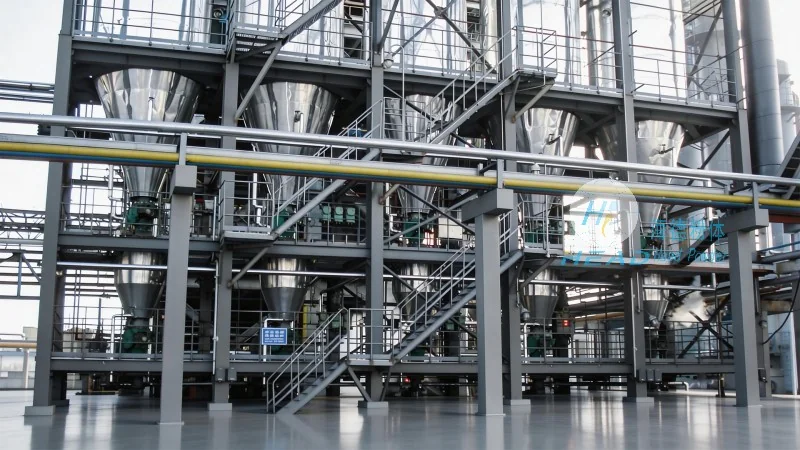
Pneumatic Conveying Technology: An Overview
Pneumatic conveying systems utilize air or other gases to transport bulk materials like fine coal powder through a pipeline network. Unlike traditional mechanical methods such as belt conveyors or screw conveyors, pneumatic systems eliminate the need for physical contact with the material, reducing wear and tear on equipment. This non-contact approach is particularly advantageous for fine coal powder, which is prone to agglomeration and can cause blockages in traditional conveyors.
Key Advantages of Pneumatic Conveying for Fine Coal Powder
One of the primary benefits of pneumatic conveying is its ability to handle fine coal powder with high efficiency and minimal loss. The system can transport materials over long distances with minimal energy consumption, making it cost-effective for industrial applications. Additionally, pneumatic conveying reduces the risk of dust contamination and environmental pollution, as the material is contained within the pipeline system. This is crucial for maintaining compliance with environmental regulations and ensuring workplace safety.
How Pneumatic Conveying Enhances Material Handling
For fine coal powder, pneumatic conveying offers superior control over material flow. The system can adjust the conveying rate and pressure to match the specific characteristics of the coal powder, ensuring consistent and reliable delivery to processing units. This flexibility is essential in industrial settings where variations in material properties or processing demands may occur. Furthermore, pneumatic conveying minimizes material degradation, as the fine particles are not subjected to mechanical stress or friction that can cause attrition.
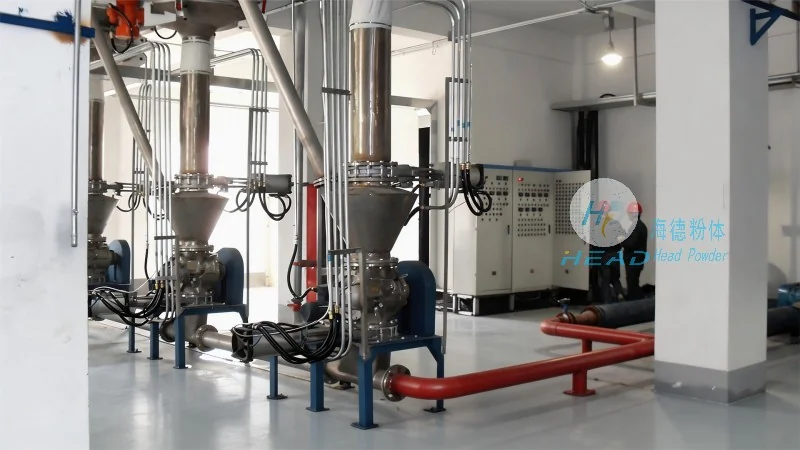
Applications in Coal Processing and Power Generation
In the coal processing industry, pneumatic conveying is widely used to transport fine coal powder from storage silos to grinding mills, boilers, or other processing equipment. The ability to handle fine particles without clogging or degradation makes it ideal for power generation facilities, where consistent fuel supply is critical for efficient operation. Companies like Shandong HeadPowder Engineering Co., Ltd. specialize in designing and implementing pneumatic conveying systems tailored to the unique needs of coal processing plants, ensuring optimal performance and reliability.
Customized Solutions for Diverse Coal Powder Types
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, provides customized pneumatic conveying solutions for various types of fine coal powder. Whether dealing with low-rank coal, bituminous coal, or other coal varieties, their systems are engineered to handle the specific properties of each material. The company’s expertise in material handling technology ensures that the conveying systems are optimized for maximum efficiency, minimal maintenance, and long-term durability. By leveraging advanced engineering and material science, headpowder delivers solutions that meet the demanding requirements of modern coal processing operations.
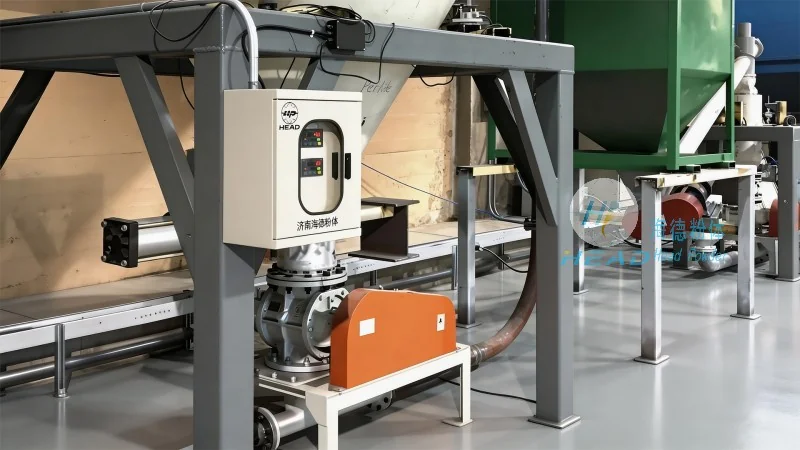
Ensuring Safety and Compliance in Pneumatic Conveying
When transporting fine coal powder, safety is a top priority. Pneumatic conveying systems are designed with safety features such as dust suppression, explosion-proof components, and pressure relief valves to mitigate risks. These measures comply with international safety standards and regulations, providing peace of mind to operators and stakeholders. Shandong HeadPowder Engineering Co., Ltd. adheres to strict safety protocols in the design, installation, and maintenance of their systems, ensuring that clients operate within legal and safety frameworks.
Long-Term Benefits and Cost Efficiency
Investing in pneumatic conveying for fine coal powder transportation yields long-term benefits beyond initial setup costs. The reduced maintenance requirements, lower energy consumption, and increased operational efficiency translate into significant cost savings over the system's lifespan. Additionally, the extended equipment life and minimized material loss contribute to overall profitability for coal processing facilities. Headpowder's commitment to quality and innovation ensures that their pneumatic conveying systems provide sustainable returns on investment, supporting the growth and sustainability of their clients' operations.
Conclusion: The Essential Role of Pneumatic Conveying
In conclusion, pneumatic conveying plays a vital role in the efficient and safe transportation of fine coal powder. Its ability to handle fine particulate materials with precision, control, and minimal environmental impact makes it an indispensable technology in the coal industry. Companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder) continue to advance this technology, providing tailored solutions that enhance operational performance and support the sustainable development of coal processing and power generation. By leveraging the advantages of pneumatic conveying, industries can achieve higher productivity, lower costs, and improved safety, ensuring a competitive edge in today's market.




