When it comes to managing the transportation of sorghum distillers grains, industrial facilities often face significant challenges related to material flow, hygiene, and operational efficiency. Traditional methods such as manual handling or mechanical conveyors may struggle with the unique properties of this byproduct, leading to inefficiencies and potential contamination risks. In response to these industry needs, advanced airlock conveyor systems have emerged as a reliable solution, offering a hygienic, efficient, and flexible approach to handling sorghum distillers grains.
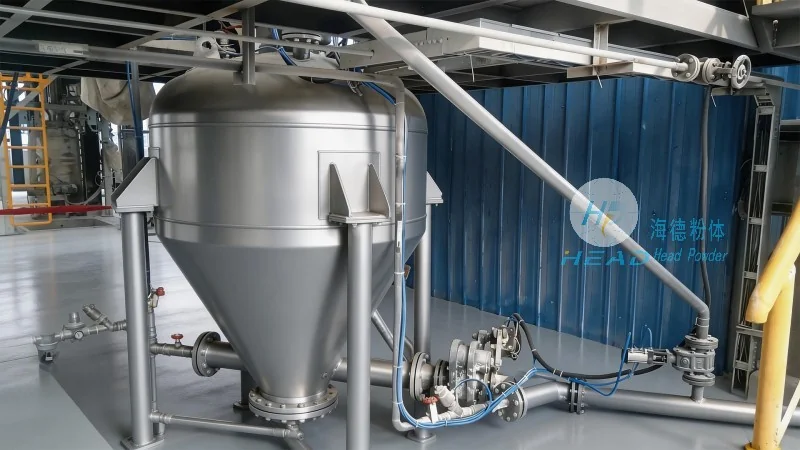
Understanding the Challenges of Sorghum Distillers Grains Transportation
Sorghum distillers grains are a high-moisture, fibrous byproduct generated during the production of ethanol from sorghum. These materials are known for their sticky and abrasive nature, which can clog traditional conveyor systems and compromise the integrity of the processing line. Additionally, maintaining hygiene standards in food and beverage applications requires equipment that prevents cross-contamination and ensures easy cleaning. Traditional mechanical conveyors may not meet these stringent requirements, making them less suitable for handling sorghum distillers grains in modern production environments.
Introducing Airlock Conveyor Systems for Optimal Performance
HeadPowder Engineering Co., Ltd., a leading provider of industrial conveyor solutions, specializes in designing and manufacturing airlock conveyor systems tailored to the specific demands of sorghum distillers grains handling. Our airlock conveyor systems utilize a combination of air pressure and mechanical seals to create airtight, dust-free transfer points, ensuring that the material is moved efficiently while maintaining strict hygiene standards. The system's design minimizes material contact with metal surfaces, reducing the risk of contamination and facilitating thorough cleaning processes.
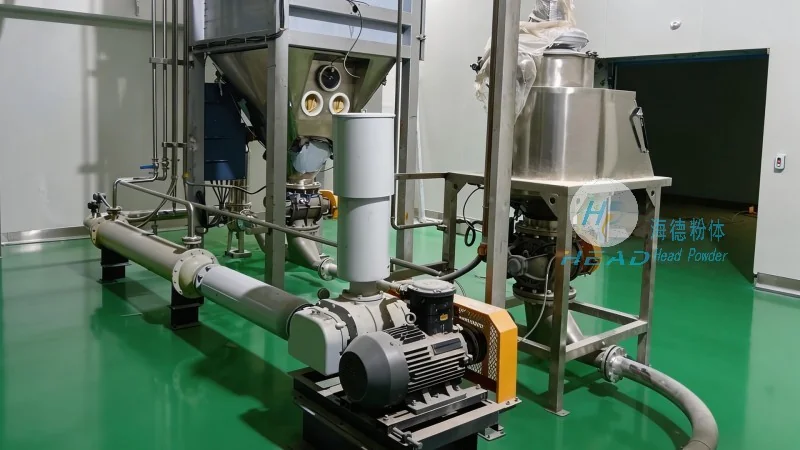
Key Features and Benefits of Our Airlock Conveyor Systems
Our airlock conveyor systems for sorghum distillers grains handling are equipped with several key features that enhance performance and reliability. The airtight seals prevent dust and airborne particles from escaping, creating a clean and safe working environment. The adjustable air pressure control allows for precise material flow regulation, accommodating varying moisture levels and bulk densities of the grains. Additionally, the modular design enables easy integration into existing production lines, reducing downtime during installation and maintenance. These features collectively contribute to improved operational efficiency, reduced maintenance costs, and enhanced product quality.
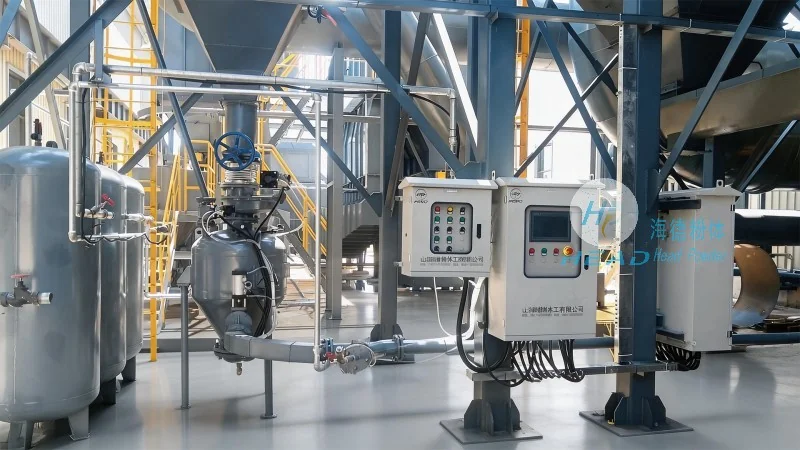
Customization and Application Flexibility
At HeadPowder Engineering Co., Ltd., we understand that each industrial facility has unique requirements. Therefore, our airlock conveyor systems are customizable to meet specific operational needs, including different material capacities, transfer heights, and integration with existing equipment. Whether used in ethanol production plants, feed mills, or other processing facilities, our systems can be adapted to handle varying volumes of sorghum distillers grains. The flexibility of our design ensures that the equipment can be optimized for the specific workflow and production goals of each client.
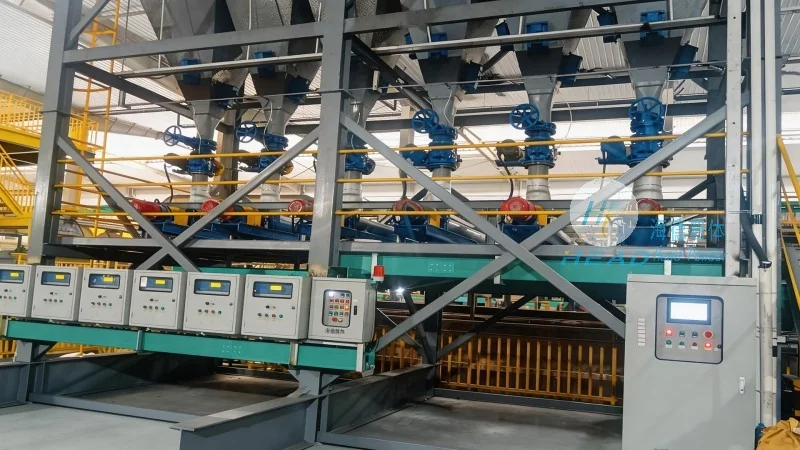
Reliability and Durability in Industrial Settings
Constructed with high-quality materials and robust engineering, our airlock conveyor systems are built to withstand the demanding conditions of industrial environments. The components are designed to resist corrosion, wear, and abrasion, ensuring long-term performance and minimal downtime. Regular maintenance is simplified due to the system's modular design, allowing for quick replacement of parts without extensive disassembly. This reliability is crucial for maintaining consistent production output and minimizing operational disruptions in facilities that rely on efficient sorghum distillers grains handling.
Conclusion: Enhancing Efficiency with Advanced Technology
In conclusion, airlock conveyor systems from HeadPowder Engineering Co., Ltd. offer an effective solution to the challenges of sorghum distillers grains transportation. By combining hygienic design, efficient material handling, and customizable features, our systems help industrial facilities improve operational efficiency, maintain product quality, and reduce maintenance costs. With our commitment to quality and customer satisfaction, HeadPowder Engineering Co., Ltd. provides reliable airlock conveyor systems that meet the evolving needs of the industry. Based in Shandong, China, we serve clients globally, delivering innovative solutions for efficient sorghum distillers grains handling.




