HeadPowder, a leading provider in the field of industrial powder handling solutions, specializes in equipment designed for the efficient transport and management of desulfurization and denitrification agents. These agents are critical components in modern industrial processes, particularly in power generation and environmental protection sectors, where precise control over powder flow is essential for optimal performance and compliance with environmental regulations.
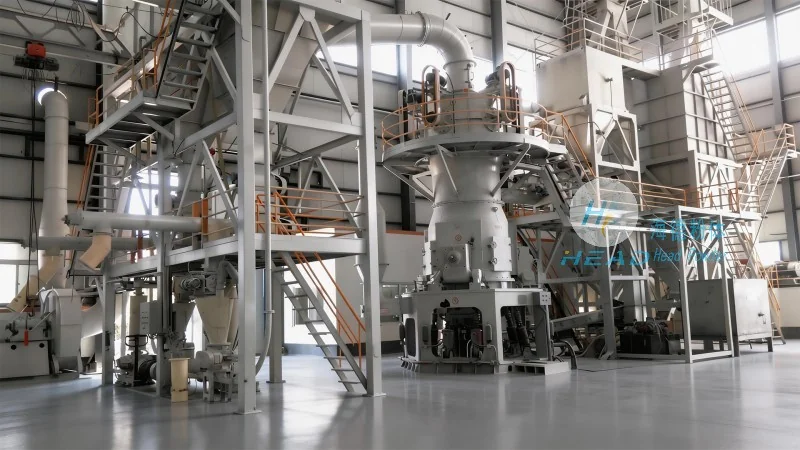
Overview of Powder Handling Equipment for Desulfurization and Denitrification Agents
At Shandong HeadPowder Engineering Co., Ltd., our powder handling equipment is engineered to meet the demanding requirements of handling fine powders used in desulfurization and denitrification systems. The equipment is designed to ensure reliable, low-dust, and energy-efficient operation, addressing the unique challenges associated with transporting these reactive materials. The company, headquartered in Shandong, China, has built a reputation for delivering high-quality, customized solutions tailored to the specific needs of clients in various industrial applications.
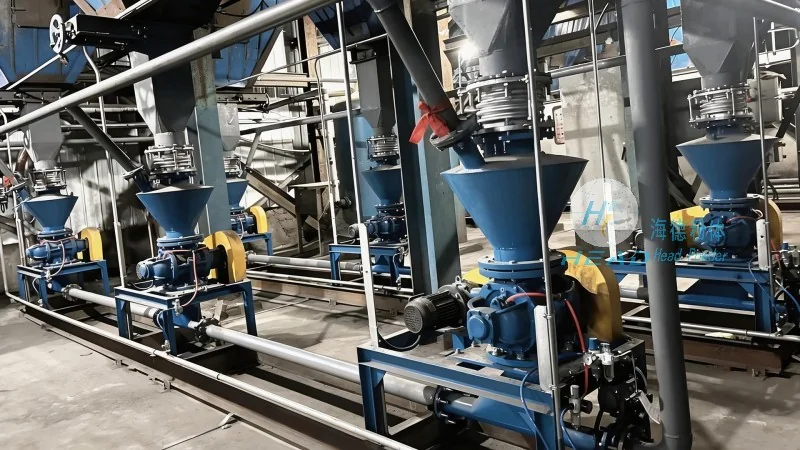
Key Components and Their Roles in the Equipment
The core components of our powder handling equipment include feeders, conveyors, and control systems, each playing a crucial role in the overall operation. The feeders are responsible for accurately metering the powder, ensuring a consistent flow rate that matches the process requirements. This precision is vital to maintain the efficiency of the desulfurization and denitrification reactions, as fluctuations in powder feed can impact the quality of emissions control. The conveyors, typically using pneumatic or mechanical systems, transport the powder from the storage silos to the injection points in the industrial processes. Pneumatic conveyors, for instance, use compressed air to move the fine powder through pipelines, minimizing particle degradation and dust generation. Mechanical conveyors, such as screw or belt conveyors, are also employed for bulk handling, offering robust solutions for larger throughput applications.
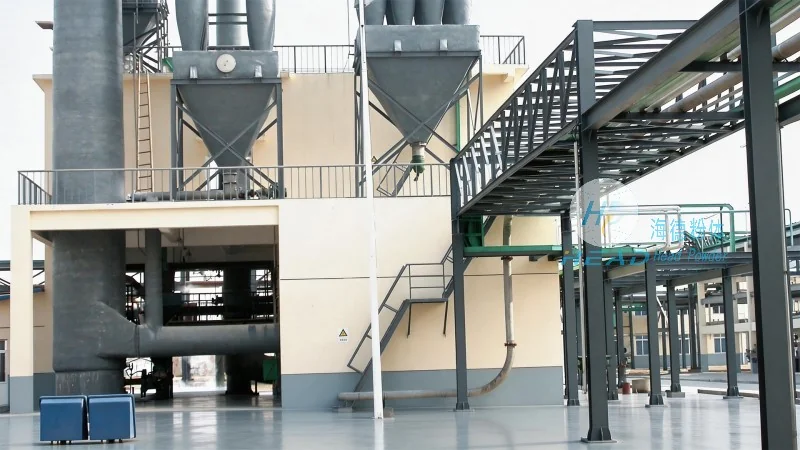
Working Principle of the Powder Handling Process
The operation of the powder handling equipment for desulfurization and denitrification agents follows a systematic process that begins with material storage and ends with precise injection. Initially, the desulfurization and denitrification agents are stored in bulk storage silos, where they are kept under controlled conditions to prevent caking or moisture absorption. From the silos, the powder is drawn into the feeder system, which uses a rotary or vibratory mechanism to discharge the material into the conveyor system. The feeder's design ensures that the powder is released at a controlled rate, preventing overloading or underfeeding of the downstream equipment. The conveyor then transports the powder to the injection point, where it is mixed with other process fluids or gases before being introduced into the main industrial process. This entire process is monitored and controlled by a sophisticated control system that adjusts the flow rates based on real-time process parameters, ensuring optimal performance and minimizing waste.
Operation Process: From Storage to Injection
The operational workflow of our powder handling equipment involves several key steps that ensure smooth and efficient operation. The process starts with the preparation of the powder in the storage silos, where the material is pre-screened to remove any large particles or contaminants that could damage the equipment or affect the process. Once the material is ready, the feeder system activates, and the powder is metered at the desired rate. The conveyor system then transports the powder through the pipeline network, which is typically equipped with filters and valves to regulate the flow and maintain system integrity. At the injection point, the powder is mixed with the process gas or liquid, and the mixture is then introduced into the main process, such as a boiler or flue gas treatment system. The control system continuously monitors the flow rates, pressure, and temperature of the system, making adjustments as needed to maintain stable operation. This closed-loop control system ensures that the powder is delivered accurately and consistently, supporting the overall efficiency of the desulfurization and denitrification process.
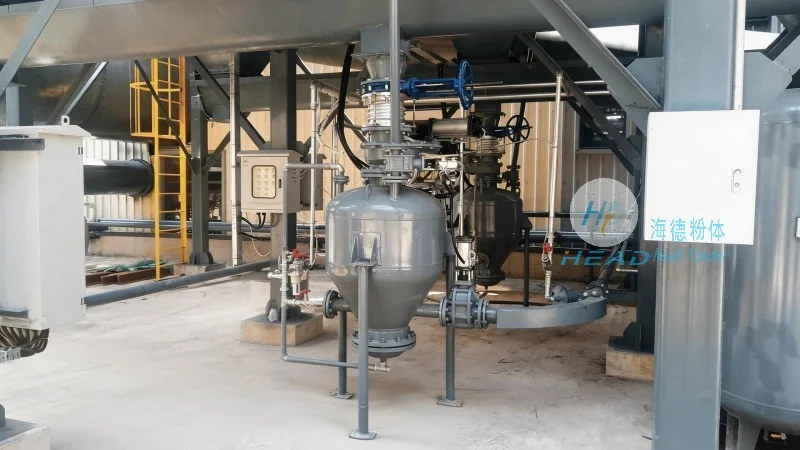
Advantages of Our Powder Handling Solutions
Our powder handling equipment for desulfurization and denitrification agents offers several advantages that make it an ideal choice for industrial applications. Firstly, the equipment is designed to minimize dust generation, which is critical for maintaining a safe working environment and complying with environmental regulations. The use of enclosed systems and efficient filtration reduces the risk of airborne particles, protecting both personnel and the surrounding environment. Secondly, the equipment is energy-efficient, with optimized designs that reduce power consumption while maintaining high throughput. This not only lowers operational costs but also contributes to a more sustainable operation. Thirdly, the equipment is highly reliable, with robust construction and minimal maintenance requirements, ensuring continuous operation with minimal downtime. The company's commitment to quality and customization ensures that each solution is tailored to the specific needs of the client, providing a perfect fit for their industrial processes.




