HeadPowder, a leading provider of industrial material handling solutions, specializes in advanced pneumatic conveying systems designed for efficient and reliable transportation of bulk materials. This article explores the fundamental principles of tonne bag material pneumatic conveying equipment and highlights the key working scene characteristics that make it an essential solution across various industries.
Understanding the Core Principles of Tonne Bag Material Pneumatic Conveying
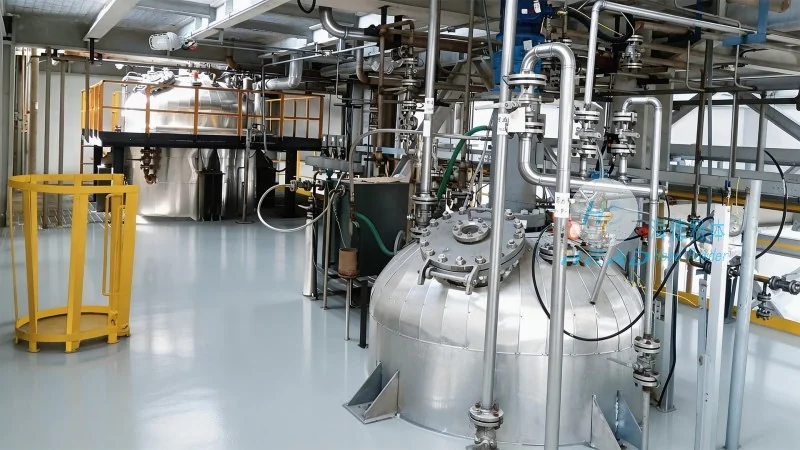
Tonne bag material pneumatic conveying equipment operates on the principle of using air or gas to transport bulk materials from a source to a destination. The system typically consists of a hopper, a conveying line, a control system, and a discharge mechanism. There are two primary types of pneumatic conveying systems: suction (or vacuum) systems and pressure systems. Suction systems create a negative pressure in the conveying line to draw material from the source, while pressure systems use positive pressure to push material through the line. For tonne bag applications, suction systems are often preferred due to their ability to handle materials with higher moisture content and lower flow rates, making them suitable for a wide range of bulk materials including powders, granules, and even fine particles. The suction system works by using a vacuum pump to create a low-pressure environment in the hopper and conveying line. As the material is drawn into the hopper, it is then carried by the air flow through the line to the discharge point. This method is particularly effective for materials that are difficult to handle with positive pressure, such as those with high dust generation or those that are prone to caking.
Key Working Scene Characteristics of Tonne Bag Pneumatic Conveying Equipment
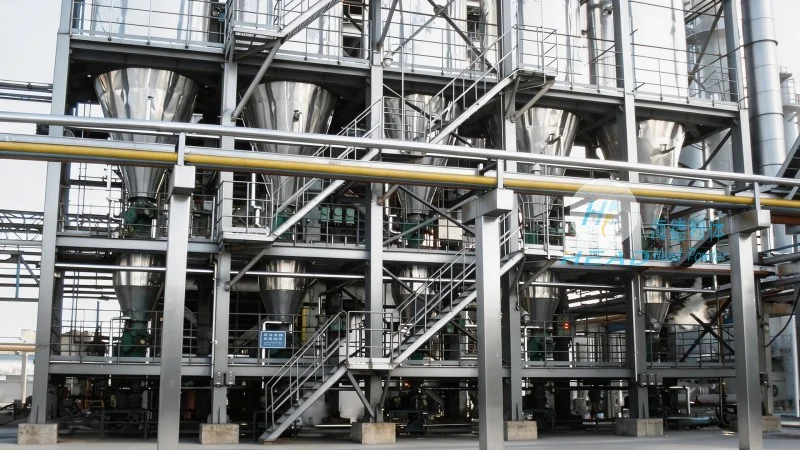
The working scene characteristics of tonne bag material pneumatic conveying equipment are tailored to meet the specific demands of different industrial environments. These characteristics include high efficiency in material transfer, minimal product contamination, and the ability to handle various material properties such as particle size, density, and moisture content. The equipment is designed to integrate seamlessly with existing production lines, ensuring smooth and continuous material flow. In addition, the system offers flexibility in terms of layout and installation, allowing it to be adapted to different facility sizes and configurations. This adaptability is crucial for industries where space is limited or where the production process requires a customized material handling solution. The system's ability to maintain consistent flow rates and pressure levels is also a key characteristic, ensuring that the material is transported at optimal speeds without causing blockages or damage to the equipment.
Applications Across Diverse Industrial Sectors
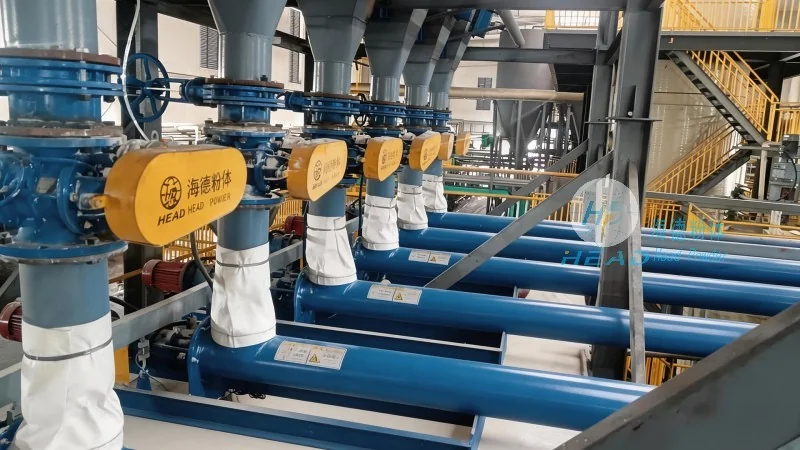
HeadPowder's tonne bag material pneumatic conveying equipment is widely used across multiple industrial sectors, including chemical processing, pharmaceutical manufacturing, food and beverage production, and mining. In the chemical industry, the equipment is essential for transporting raw materials and finished products, ensuring that hazardous materials are handled safely and efficiently. The chemical industry often deals with materials that are corrosive or reactive, and the pneumatic conveying system's enclosed design prevents exposure and contamination. In pharmaceutical manufacturing, the system's ability to maintain sterile conditions and prevent product contamination is critical, making it a preferred choice for handling sensitive materials like active pharmaceutical ingredients (APIs). The hygienic design of the equipment, including smooth surfaces and easy-to-clean components, meets the stringent requirements of the pharmaceutical industry. The food and beverage industry benefits from the equipment's hygienic design and ability to handle food-grade materials without compromising quality. The system is often used to transport ingredients like flour, sugar, and spices, ensuring that the materials remain fresh and free from contamination. In mining operations, the system is used to transport bulk ores and minerals from storage to processing facilities, improving operational efficiency and reducing labor costs. The mining industry requires robust and durable equipment to handle abrasive materials, and HeadPowder's pneumatic conveying systems are built to withstand these conditions.
Advantages of Choosing HeadPowder's Pneumatic Conveying Solutions
When selecting a pneumatic conveying system for tonne bag material handling, several factors should be considered. HeadPowder's solutions offer several advantages that make them a top choice for businesses. The equipment is engineered for durability and long-term performance, with components designed to withstand the rigors of continuous operation. The system's energy efficiency reduces operational costs, making it a cost-effective solution for businesses looking to optimize their material handling processes. For example, the suction system uses less energy compared to pressure systems, as it relies on the vacuum pump to create the necessary pressure difference. Additionally, the company provides comprehensive support, including installation, maintenance, and technical assistance, ensuring that clients receive reliable and consistent service. HeadPowder's technical team offers expert advice on system design and configuration, helping clients choose the most suitable solution for their specific material and application requirements. The company also offers customization options, allowing businesses to tailor the equipment to their unique needs, such as adding additional hoppers or modifying the discharge mechanism.
Conclusion and Company Information
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted name in the field of industrial material handling. The company's expertise in designing and manufacturing tonne bag material pneumatic conveying equipment ensures that clients receive tailored solutions that meet their specific needs. By understanding the core principles and working scene characteristics of these systems, businesses can make informed decisions about implementing efficient material handling solutions. HeadPowder's commitment to innovation and customer satisfaction is reflected in the high reliability and performance of their pneumatic conveying equipment. The company's focus on quality and durability ensures that clients invest in a long-lasting solution that delivers consistent results. With a strong presence in the market and a reputation for excellence, HeadPowder continues to be a leader in providing reliable and effective pneumatic conveying solutions for various industrial applications.




