HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems for coke powder. This article explores the fundamental principles behind coke powder pneumatic conveying and highlights the key characteristics of its operational scenarios, providing a comprehensive overview for industry professionals and potential clients.
Understanding the Core Principles of Coke Powder Pneumatic Conveying
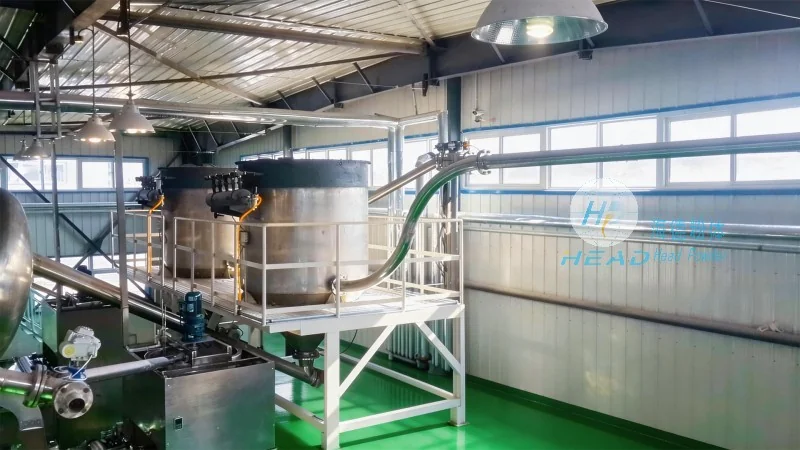
Coke powder pneumatic conveying relies on the fundamental principle of transporting solid particles through a pipeline using a pressurized or suctioned air stream. The process involves several critical components and mechanisms that work in tandem to ensure efficient and reliable material movement. At its core, the system utilizes a combination of air pressure, velocity, and particle size characteristics to achieve seamless transport. The primary components include a material feeder, a conveying line, a separation system, and a dust collection unit. The material feeder, often a rotary valve or a screw feeder, introduces coke powder into the system at a controlled rate. This is followed by the conveying line, which can be either a positive pressure system (where air is blown into the line to push the material) or a negative pressure system (where air is drawn out to pull the material). The separation system, typically a cyclone or a bag filter, separates the coke powder from the air stream, ensuring that the material is collected efficiently while the air is discharged or recycled. The dust collection unit further enhances the system's efficiency by capturing any fine particles that may escape the separation process.
Key Operational Features and Application Scenarios
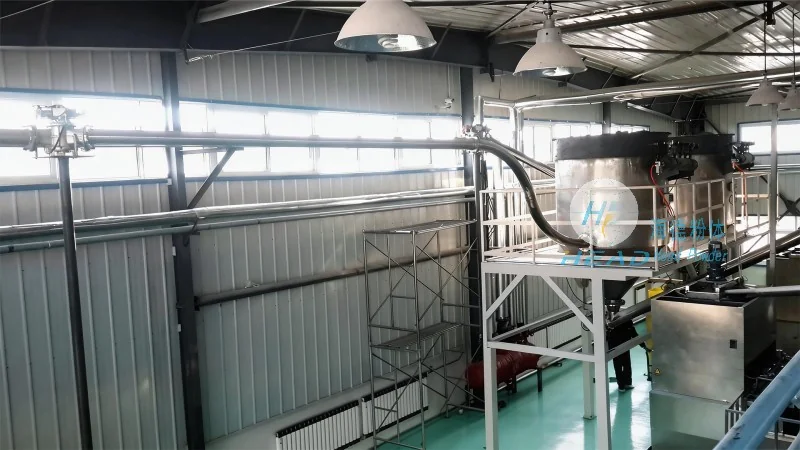
The operational characteristics of coke powder pneumatic conveying systems are tailored to meet the specific demands of various industrial applications. These systems are particularly well-suited for industries that require the transport of fine, dry powders over medium to long distances. The key features include high efficiency in material handling, minimal maintenance requirements, and the ability to operate in a closed system, which helps in controlling dust and maintaining environmental standards. In the steel industry, for example, coke powder is a critical raw material used in blast furnaces. Pneumatic conveying systems are used to transport coke powder from storage silos to the furnace, ensuring a continuous and controlled supply. The system's ability to handle high volumes and maintain consistent flow rates is essential for maintaining the efficiency of the blast furnace operation. In the chemical industry, coke powder is used as a fuel or a raw material in various processes. Pneumatic conveying systems are employed to transport coke powder from storage facilities to processing units, such as reactors or reactors. The system's flexibility in handling different particle sizes and moisture content makes it suitable for diverse chemical applications. Additionally, in the cement industry, coke powder can be used as a fuel in kilns. Pneumatic conveying systems are used to transport coke powder from storage to the kiln, ensuring a steady fuel supply. The system's ability to operate in high-temperature environments and handle abrasive materials is crucial for cement production. The operational scenarios also vary based on the distance and the volume of material to be transported. For short distances and low volumes, a simple suction system may be sufficient. However, for long distances and high volumes, a positive pressure system with a larger conveying line and more powerful air compressors is required. The choice of system depends on factors such as the particle size distribution, the moisture content of the coke powder, and the required flow rate. HeadPowder's expertise lies in designing and implementing customized pneumatic conveying systems that meet the specific needs of each application, ensuring optimal performance and reliability.
Advantages and Challenges in Coke Powder Pneumatic Conveying
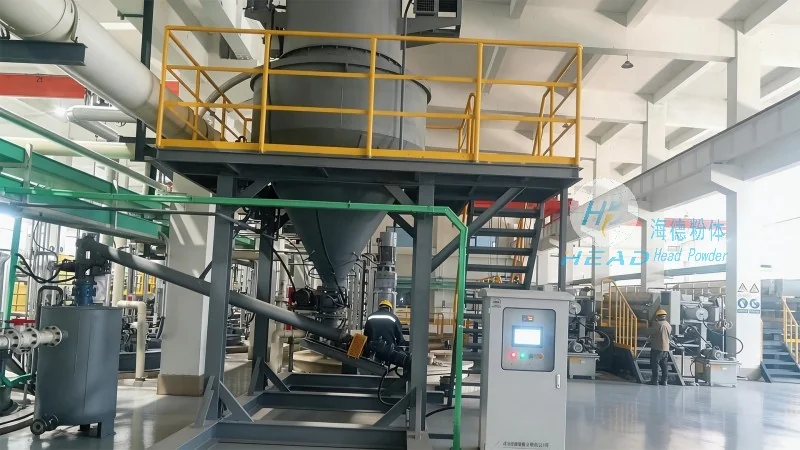
Despite its benefits, coke powder pneumatic conveying systems also present certain challenges that must be addressed to ensure their effective operation. One of the primary challenges is the potential for particle segregation and agglomeration, which can lead to blockages in the conveying line. This issue is particularly relevant for coke powder, which can have a wide range of particle sizes and densities. To mitigate this, HeadPowder employs advanced feeding mechanisms and material handling techniques that ensure a uniform flow of material. Another challenge is the risk of dust explosions, which can occur if the system is not properly designed or maintained. HeadPowder's systems incorporate explosion-proof designs and dust collection systems to minimize this risk. Additionally, the system's energy consumption is a consideration, as pneumatic conveying can be energy-intensive, especially for long-distance transport. However, modern systems use high-efficiency air compressors and optimized line designs to reduce energy consumption. The advantages of coke powder pneumatic conveying, however, far outweigh these challenges. The system offers significant benefits, including reduced labor costs, improved safety by eliminating manual handling of powders, and increased production efficiency. The closed system design also helps in maintaining a clean and safe working environment, which is crucial in industries where dust control is a regulatory requirement. HeadPowder's commitment to quality and innovation has enabled them to develop systems that address these challenges effectively, providing reliable and efficient solutions for coke powder transport.




