Copper sulfate, a widely used chemical in industrial processes, often requires efficient and safe handling during transportation. Pneumatic conveying systems have emerged as a reliable solution for moving copper sulfate powder, offering advantages over traditional methods such as reduced dust exposure and improved operational efficiency. This article explores the working principle and key features of copper sulfate powder pneumatic conveying equipment, highlighting how such systems enhance material handling in industrial settings.
Understanding the Working Principle of Copper Sulfate Powder Pneumatic Conveying Systems
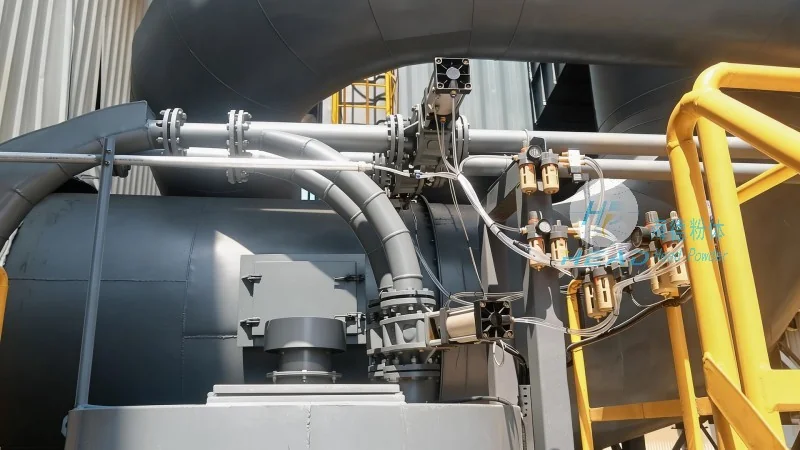
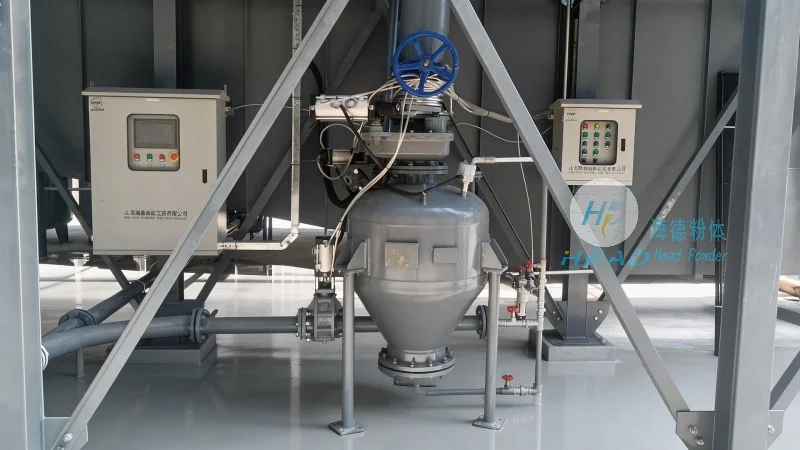
Pneumatic conveying equipment for copper sulfate powder operates by utilizing air or gas to transport dry powder materials through a pipeline. The system typically follows a sequence of stages, each designed to ensure effective and controlled movement of the powder. The core components include a feeding device, a conveying pipeline, a separation unit, and a dust collection system. In a typical positive pressure system, compressed air is introduced at the material inlet, creating a pressure differential that propels the copper sulfate powder through the pipeline. The feeding mechanism, often a rotary valve or a star feeder, controls the flow rate of the powder, ensuring a consistent and controlled discharge into the conveying line. As the powder travels through the pipeline, it is suspended by the air flow, preventing clogging and maintaining a smooth flow. At the discharge end, a separation unit, such as a cyclone or a bag filter, separates the powder from the air stream, allowing the copper sulfate to be collected in a receiving hopper or container. The air, now free of powder, is then discharged to the atmosphere or recirculated, depending on the system design. This process effectively transports copper sulfate powder over long distances with minimal loss and contamination.
Key Features of Copper Sulfate Powder Pneumatic Conveying Equipment
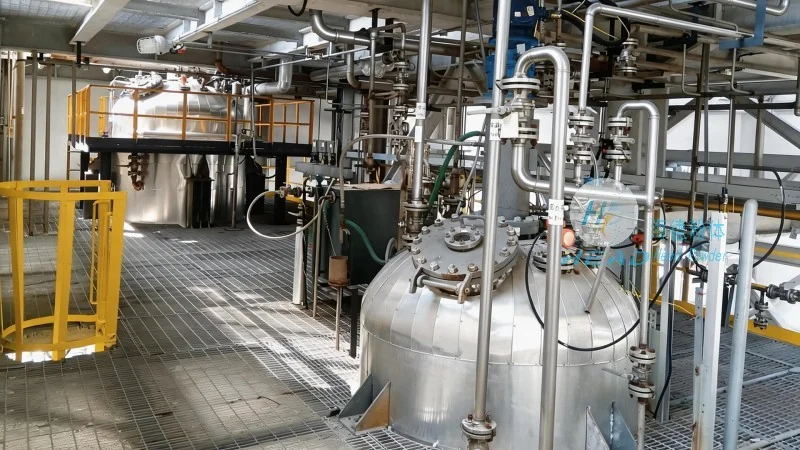
The copper sulfate powder pneumatic conveying equipment offered by Shandong HeadPowder Engineering Co., Ltd. is engineered to address the unique challenges of handling this chemical. One of the primary features is its high efficiency in material transport, which minimizes downtime and increases overall productivity. The system is designed to handle varying particle sizes and moisture content of copper sulfate, ensuring consistent performance even under different operating conditions. Additionally, the equipment incorporates advanced dust control measures, reducing the risk of respiratory hazards and environmental contamination. This is achieved through integrated dust collection systems that capture fine particles, ensuring compliance with industrial safety and environmental regulations. Another notable feature is the flexibility of the system, which can be customized to suit specific plant layouts and operational requirements. The modular design allows for easy integration with existing production lines, minimizing installation time and costs. Furthermore, the equipment is built with durable materials, such as stainless steel, to withstand the corrosive nature of copper sulfate and the abrasive effects of repeated use. This ensures long-term reliability and reduces maintenance requirements, contributing to lower operational costs over the equipment's lifespan.
Benefits of Using Pneumatic Conveying for Copper Sulfate Powder Handling
Implementing copper sulfate powder pneumatic conveying equipment brings several significant benefits to industrial operations. Firstly, it enhances safety by reducing direct human contact with the powder, minimizing exposure to dust and potential health risks. The enclosed system also prevents the spread of dust in the workplace, creating a cleaner and healthier environment for employees. Secondly, the system improves operational efficiency by automating the material handling process, reducing the need for manual labor and associated errors. The consistent flow rate and controlled discharge help maintain stable production rates, leading to higher output and better quality control. Thirdly, the equipment contributes to cost savings by minimizing material loss and reducing the need for additional cleaning or maintenance. The efficient separation of powder from air reduces the amount of waste and the frequency of filter changes, lowering operational expenses. Lastly, the system's adaptability allows it to be integrated into existing facilities without major modifications, making it a cost-effective solution for upgrading or expanding material handling capabilities. These benefits collectively make copper sulfate powder pneumatic conveying equipment a preferred choice for industries seeking reliable, efficient, and safe material transport solutions.
Conclusion
In conclusion, the working principle and features of copper sulfate powder pneumatic conveying equipment, as exemplified by the solutions from Shandong HeadPowder Engineering Co., Ltd., represent a significant advancement in industrial material handling. By leveraging pneumatic technology, these systems effectively address the challenges of transporting copper sulfate powder, offering high efficiency, enhanced safety, and cost-effectiveness. The integration of advanced components and customizable designs ensures that the equipment meets the specific needs of various industrial applications, from small-scale operations to large-scale production facilities. As industries continue to prioritize efficiency and safety in material handling, pneumatic conveying systems remain a vital component in optimizing processes and ensuring compliance with regulatory standards. The expertise and products of Shandong HeadPowder Engineering Co., Ltd. provide reliable solutions for businesses seeking to enhance their copper sulfate powder handling capabilities, contributing to improved productivity and operational excellence.




