Understanding the working principle and features of fertilizer powder conveying systems is crucial for optimizing material handling in agricultural and industrial applications. These systems are designed to efficiently transport bulk fertilizer powders from storage to processing or distribution points, ensuring consistent performance and reliability.
Introduction to Fertilizer Powder Conveying Systems
Fertilizer powder conveying systems are specialized equipment used in the agricultural and chemical industries to move bulk solid materials, such as nitrogen, phosphorus, and potassium fertilizers, through various stages of production and distribution. The primary goal of these systems is to provide a safe, efficient, and cost-effective method for handling powders that are often abrasive, dusty, or prone to caking. By leveraging advanced engineering and material handling technologies, these systems address the unique challenges associated with fertilizer powders, including their fine particle size, variable flow properties, and potential for dust generation.
Working Principle of the Fertilizer Powder Conveying System
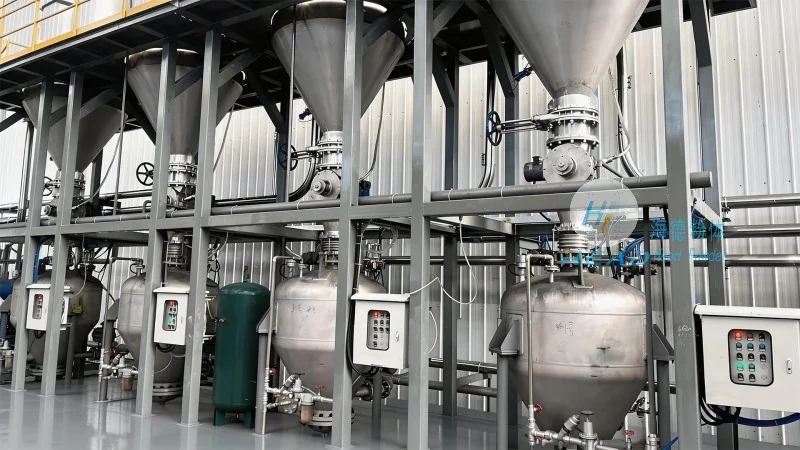
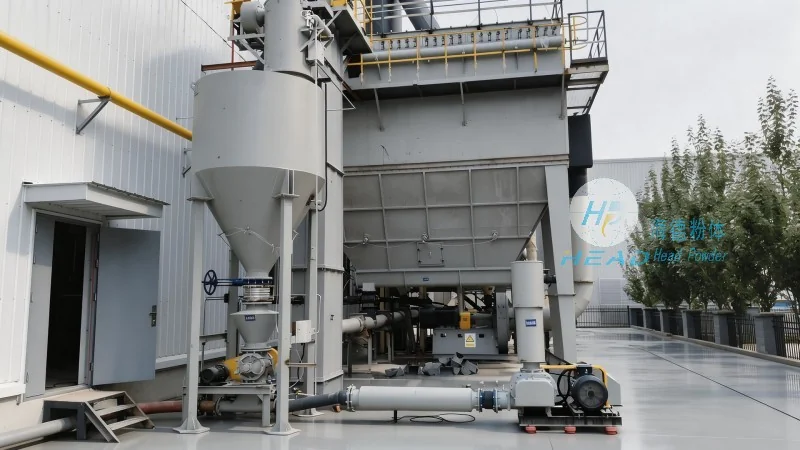
The core working principle of a typical fertilizer powder conveying system involves the use of mechanical components to move material through a pipeline or conveyor. The system typically includes a hopper for material storage, a feeding mechanism to control the flow rate, a conveyor (such as a screw, pneumatic, or belt conveyor), and a control system to regulate operation. The process begins with the fertilizer powder being fed from the storage hopper into the conveyor. Depending on the system design, the material may be transported via a rotating screw (screw conveyor) that pushes the powder forward, or via an air stream in a pneumatic conveyor that carries the particles through the pipeline. The control system monitors parameters like pressure, flow rate, and temperature to ensure smooth operation and prevent blockages or overloading. This integrated approach allows for precise control over the conveying process, minimizing material loss and maximizing system efficiency.
Key Features of the Fertilizer Powder Conveying System
Modern fertilizer powder conveying systems are equipped with several key features that enhance performance and reliability. One of the most important features is the ability to handle a wide range of powder characteristics, including different particle sizes, moisture contents, and bulk densities. This versatility is achieved through adjustable feeding mechanisms and variable-speed conveyors that can adapt to varying material properties. Another critical feature is dust control, which is essential for maintaining a safe working environment and complying with environmental regulations. Advanced systems incorporate dust collection and filtration systems, such as cyclones or baghouses, to capture and remove airborne particles. Additionally, the systems are designed for easy maintenance and cleaning, with removable components that allow for quick removal of caked or adhered material. This reduces downtime and ensures consistent operation over extended periods. Energy efficiency is also a key consideration, with many systems incorporating variable frequency drives (VFDs) to adjust motor speed and power consumption based on the load, thereby reducing operational costs.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
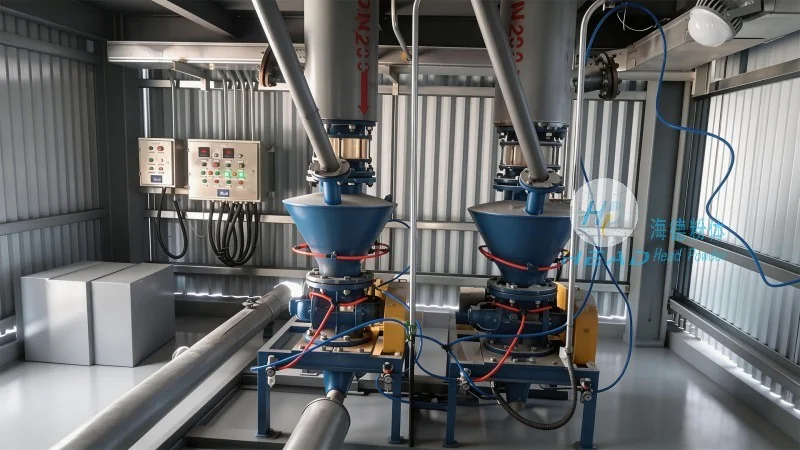
HeadPowder, a leading manufacturer of fertilizer powder conveying systems, is dedicated to providing high-quality, reliable equipment for the agricultural and chemical industries. With its headquarters in Shandong, China, the company has established itself as a trusted partner for businesses seeking efficient and durable material handling solutions. HeadPowder's products are engineered to meet the specific needs of fertilizer producers, ensuring optimal performance in diverse operational conditions. The company's commitment to innovation and customer satisfaction has made it a preferred choice for clients worldwide, who rely on its systems to enhance productivity and reduce operational costs.
Conclusion
In summary, fertilizer powder conveying systems play a vital role in the efficient handling of bulk fertilizers, combining advanced engineering with practical features to address the unique challenges of powder materials. By understanding the working principle and key features of these systems, users can make informed decisions when selecting equipment that best suits their operational requirements. With companies like Shandong HeadPowder Engineering Co., Ltd. leading the way in design and manufacturing, the industry continues to advance, providing reliable solutions for the agricultural sector's material handling needs.




