Understanding the working principle and features of sodium phosphate pneumatic conveying systems is crucial for industries that handle this chemical efficiently and safely. This article provides an in-depth look at how these systems operate and the key characteristics that make them effective in material handling applications.
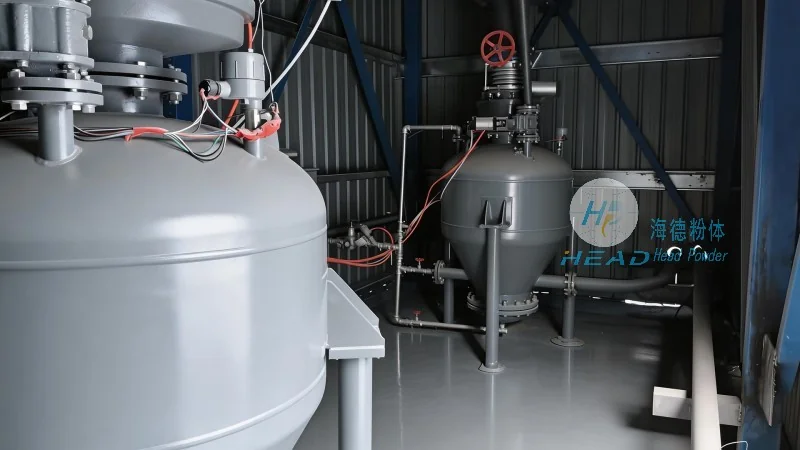
Introduction to Sodium Phosphate Pneumatic Conveying Systems
Sodium phosphate is a widely used chemical in various industrial processes, including food processing, pharmaceuticals, and chemical manufacturing. The efficient transport of sodium phosphate powder from one location to another is essential for maintaining production efficiency and minimizing downtime. Pneumatic conveying systems offer a reliable solution for this purpose, particularly when dealing with fine powders like sodium phosphate.
Working Principle of the Pneumatic Conveying System
The core of a sodium phosphate pneumatic conveying system is its ability to use air or gas to transport solid particles. The system typically consists of a hopper, a conveyor line, and a receiver. The process begins when the sodium phosphate powder is fed into the hopper. From there, the material is drawn into the conveyor line by a vacuum or pressure source, depending on the system design. The air or gas acts as a medium, carrying the powder particles through the pipeline to the destination receiver. This method eliminates the need for mechanical components like belts or screws, reducing maintenance requirements and potential points of failure.
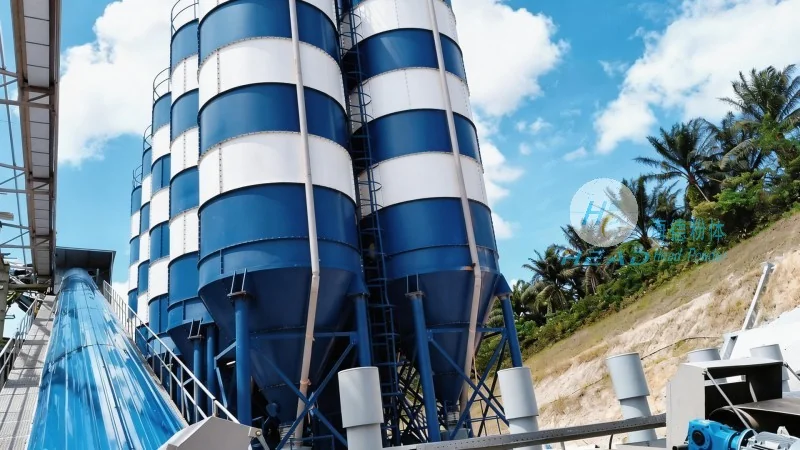
Key Features and Advantages of the System
Several features distinguish sodium phosphate pneumatic conveying systems from other material handling methods. Firstly, the system is highly flexible, allowing for changes in the conveying route without major modifications. This adaptability is particularly valuable in dynamic production environments where layouts may change. Secondly, the system offers excellent containment, preventing dust and powder emissions that could pose health or environmental risks. This is achieved through sealed pipelines and proper filtration systems, ensuring compliance with safety regulations. Thirdly, the system provides consistent and reliable material flow, which is critical for maintaining production rates and product quality. The absence of mechanical parts also reduces the risk of contamination, making it suitable for applications where product purity is paramount.
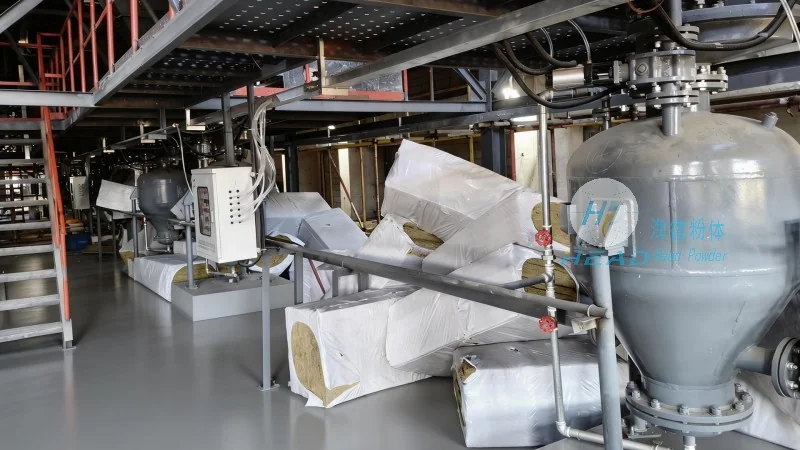
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of pneumatic conveying equipment, specializes in providing customized solutions for handling sodium phosphate and other fine chemicals. With years of experience in the industry, the company has developed advanced systems that meet the specific needs of various applications. The company's headquarters is located in Shandong, China, where it maintains a strong commitment to quality and innovation. HeadPowder's products are designed to enhance operational efficiency while ensuring safety and compliance with industry standards.
Conclusion
In summary, sodium phosphate pneumatic conveying systems operate by using air to transport powder, offering advantages such as flexibility, containment, and reliability. These features make them an ideal choice for industries dealing with sodium phosphate. HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of such systems, delivering high-quality solutions tailored to customer requirements.




