For industrial applications requiring efficient and safe transportation of dry cobblestone powders, specialized conveying systems are essential. These systems are designed to handle the unique properties of cobblestone powders, including their abrasive nature and tendency to generate dust. Understanding the structure and operational principles of such systems is crucial for optimizing performance and ensuring compliance with safety standards.
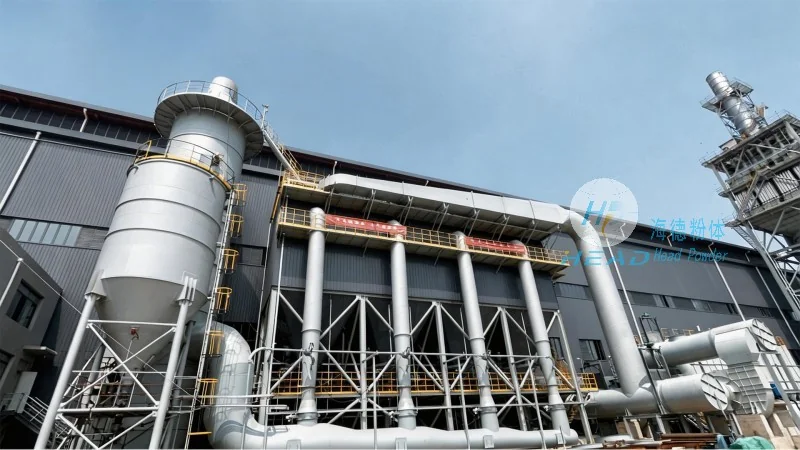
About Dry Cobblestone Powder Conveying Systems
Dry cobblestone powder conveying systems are engineered to transport granular materials like cobblestone powders from one location to another. Unlike liquid or gas transport, these systems rely on mechanical means to move the solid particles. The primary goal is to maintain the integrity of the powder while minimizing degradation, caking, or dust generation. Such systems are widely used in industries such as construction, mining, and chemical processing, where the consistent supply of raw materials is critical to production efficiency.
Key Structural Components of the Conveying System
The dry cobblestone powder conveying system typically consists of several interrelated components. The feed hopper is the first component, responsible for receiving and storing the powder before it enters the system. It is designed to prevent material buildup and ensure a uniform flow into the subsequent parts. The conveyor itself, often a pneumatic or mechanical type, is the core of the system. Pneumatic conveyors use air pressure to move the powder through a pipeline, while mechanical conveyors rely on screw, belt, or bucket mechanisms. The pipeline network connects the feed point to the discharge point, and its design must account for the material's abrasiveness, requiring materials like stainless steel or special alloys to resist wear. The drive unit, which can be electric or hydraulic, provides the necessary force to move the powder through the system. Finally, the control system monitors parameters like pressure, flow rate, and temperature, allowing for real-time adjustments to maintain optimal operation.
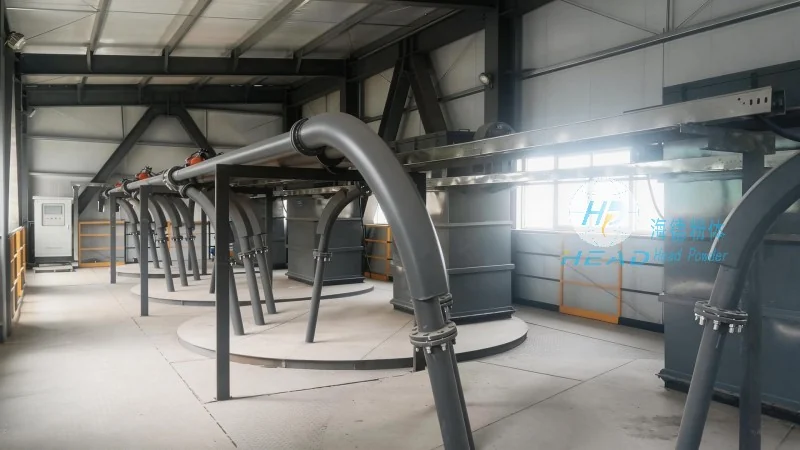
Principle of Operation
The operational principle of dry cobblestone powder conveying systems varies based on the chosen method. The most common approach is pneumatic conveying, where the powder is suspended in a stream of air and transported through the pipeline. This method is effective for both low and high concentrations of powder, with the air-to-powder ratio adjusted to ensure efficient flow. Another method is mechanical conveying, which uses rotating components like screws or belts to push the powder forward. This approach is suitable for high-volume applications and materials with higher moisture content. The principle of operation also involves maintaining a consistent pressure gradient along the pipeline to prevent backflow and ensure continuous movement of the material. Proper sealing at all joints and components is essential to prevent dust leakage and maintain system efficiency.
Advantages of Using Dry Cobblestone Powder Conveying Systems
Implementing dry cobblestone powder conveying systems offers several advantages over traditional methods. One of the most significant benefits is the reduction of dust exposure, which enhances workplace safety and compliance with environmental regulations. By containing the powder within a sealed system, the risk of inhalation or contamination is minimized. Additionally, these systems provide precise control over the flow rate and pressure, allowing for accurate dosing and process control. The high efficiency of pneumatic conveyors results in lower energy consumption compared to manual or bucket elevator systems. Furthermore, the compact design of modern conveying systems saves space in industrial facilities, making them suitable for both new installations and retrofitting existing plants. The durability of the components, especially those made from wear-resistant materials, ensures long-term reliability and reduces maintenance costs.
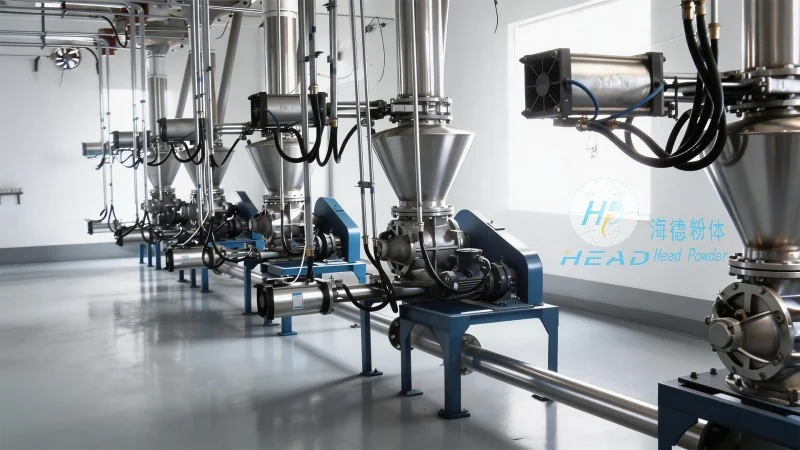
Application Scenarios
Dry cobblestone powder conveying systems are applied in a wide range of industrial scenarios. In the construction industry, they are used to transport raw materials such as gravel, sand, and cement additives from storage silos to mixing plants. The consistent supply of these materials is crucial for maintaining production schedules and ensuring the quality of concrete or mortar products. In the mining sector, the systems are employed to move crushed ore or tailings from processing units to storage or disposal sites. This helps streamline the extraction and processing workflow, improving overall operational efficiency. In the chemical industry, dry powder conveyors are used to transport catalysts, pigments, or other additives to reactors or mixing tanks. The ability to handle fine powders without clogging or agglomeration is essential for maintaining the purity and effectiveness of the final products. Each application leverages the system's ability to handle abrasive and dusty materials while ensuring safe and efficient material transfer.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of advanced powder conveying solutions. Headquartered in Shandong, China, the company has established itself as a trusted provider of high-quality conveying systems tailored to the needs of various industries. With a team of experienced engineers and technicians, headpowder specializes in designing and manufacturing custom solutions that meet specific operational requirements. The company's products are known for their durability, reliability, and energy efficiency, reflecting a commitment to excellence in powder handling technology. By focusing on innovation and customer satisfaction, headpowder has become a key player in the global market for dry powder conveying equipment.
Conclusion
Dry cobblestone powder conveying systems represent a sophisticated solution for the challenges of transporting abrasive and dusty materials. Through their well-designed structural components and operational principles, these systems ensure efficient, safe, and reliable material transfer in industrial settings. As industries continue to demand higher productivity and stricter environmental standards, the importance of advanced conveying technology will only grow. For businesses seeking to optimize their material handling processes, partnering with a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. can provide the expertise and equipment needed to achieve operational excellence and maintain a competitive edge in the market.




