Understanding the efficient and reliable transportation of maltose powder is crucial for industries that rely on consistent quality and process stability. This overview delves into the core components, operational principles, and structural design of maltose powder conveying systems, highlighting the technical advancements that enhance performance and safety in handling this specific type of bulk material.
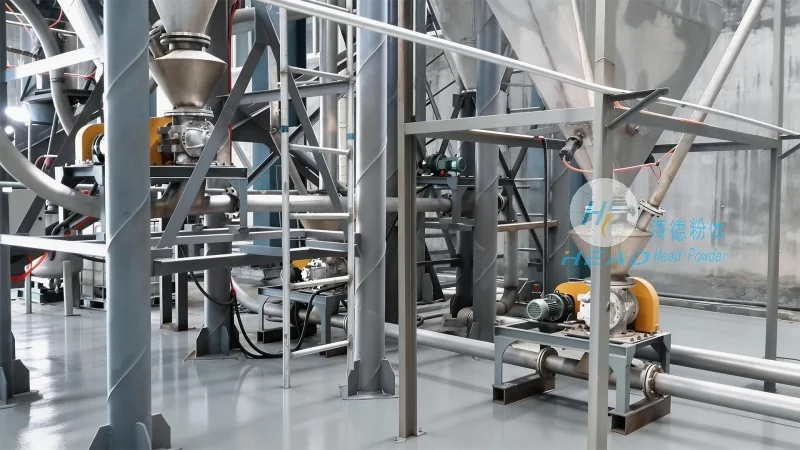
Key Components of Maltose Powder Conveying Systems
Maltose powder conveying systems typically consist of several critical components that work in unison to ensure smooth material movement. These include feed hoppers, which are designed to hold and regulate the flow of maltose powder, ensuring a consistent feed rate. The conveying mechanism, often a screw or pneumatic system, is the heart of the operation, responsible for transporting the powder from the source to the destination. Additionally, control valves and sensors are integrated to monitor and adjust the flow, maintaining optimal conditions for the material. The system may also feature cleaning mechanisms to prevent clogging and maintain hygiene, which is essential for food-grade applications like maltose processing.
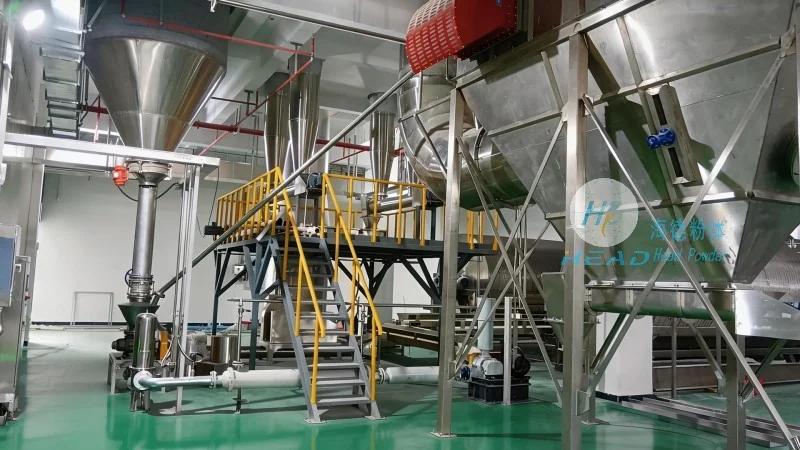
Structural Design and Operational Principles
The structural design of maltose powder conveying systems is tailored to address the unique properties of maltose powder, such as its hygroscopic nature and potential for bridging or caking. The equipment is constructed from materials that are resistant to corrosion and easy to clean, often stainless steel or specialized polymers, to meet sanitary standards. The operational principle revolves around creating a controlled environment where the powder is moved without degradation. For example, pneumatic conveying systems use air pressure to transport the powder, minimizing friction and heat generation, which helps preserve the quality of maltose. In contrast, mechanical screw conveyors rely on rotating screws to push the powder forward, providing a continuous and low-maintenance option. Both systems are designed to handle the bulk density and flow characteristics of maltose powder effectively, ensuring that the material reaches its destination without loss or contamination.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer specializing in bulk material handling solutions, including maltose powder conveying systems. With a strong focus on innovation and customer satisfaction, the company has developed advanced technologies to meet the specific needs of the food and pharmaceutical industries. HeadPowder's products are engineered to ensure high efficiency, low maintenance, and compliance with industry standards, making them a trusted choice for businesses that require reliable and hygienic powder handling. The company's commitment to quality and technical expertise has established it as a key player in the material handling sector, particularly in applications involving sensitive materials like maltose.
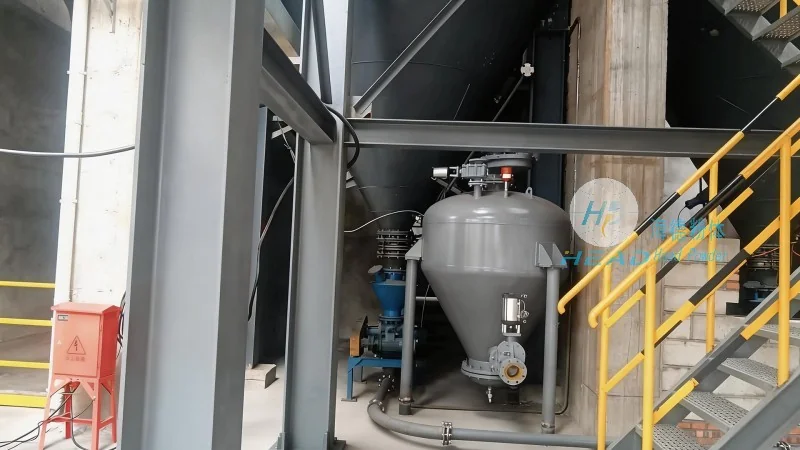
Applications and Industry Impact
Maltose powder conveying systems are widely used in various industries, including food processing, pharmaceutical manufacturing, and chemical production. In food processing, these systems are essential for transporting maltose from storage to production lines, ensuring that the material is handled hygienically and efficiently. In pharmaceutical applications, the systems must meet stringent regulatory requirements, such as those from the FDA, to ensure that the powder is not contaminated and that the process is consistent. The impact of these systems extends beyond individual operations, contributing to overall productivity and cost savings for companies. By reducing downtime and improving material flow, maltose powder conveying systems help businesses maintain competitive advantages in their respective markets.




