Efficient material handling is a critical aspect of modern industrial operations, and the automatic bulk bag unloading pneumatic conveying system has emerged as a sophisticated solution to streamline the process of handling bulk materials. This system combines advanced technology with robust engineering to provide a reliable and efficient method for transferring powders and granules from bulk bags into processing equipment or storage tanks. Understanding its working principle and key features is essential for industries that rely on consistent and safe material transfer.
Working Principle of the Automatic Bulk Bag Unloading Pneumatic Conveying System
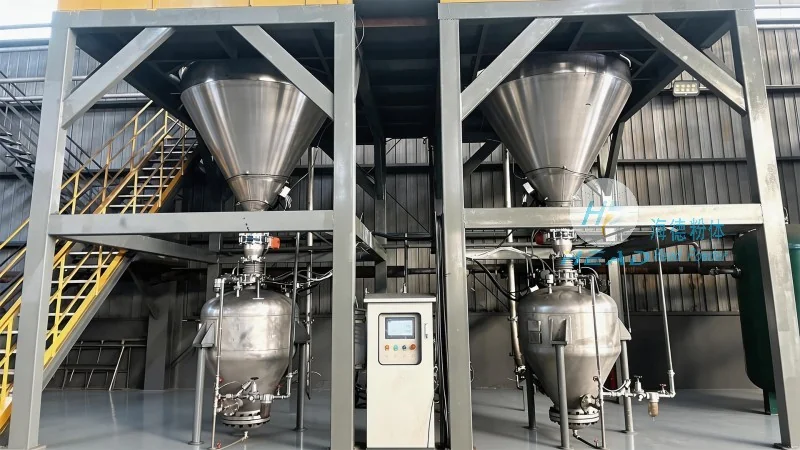
The system operates on the principle of pneumatic conveying, which utilizes air or gas to transport bulk materials through a pipeline network. The process begins with the placement of a bulk bag (also known as a super sack or FIBC) onto a specialized unloading station. The station is equipped with a hopper that is designed to receive the material from the bag. As the material is discharged from the bag, it falls into the hopper, where it is then drawn into the conveying system by a vacuum or pressure source.
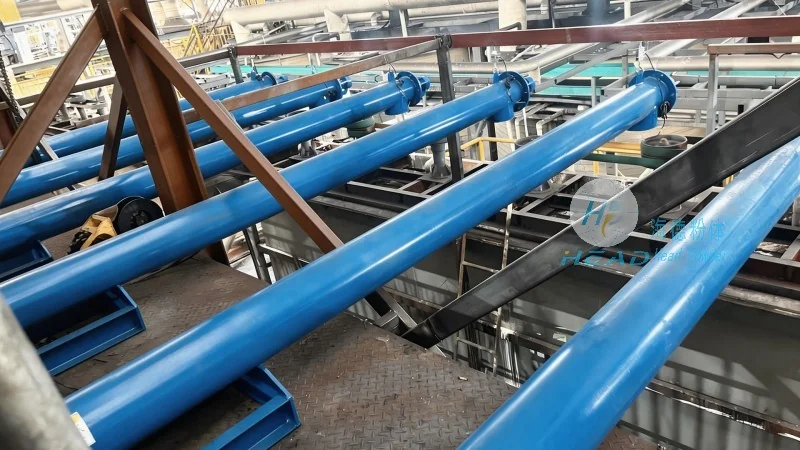
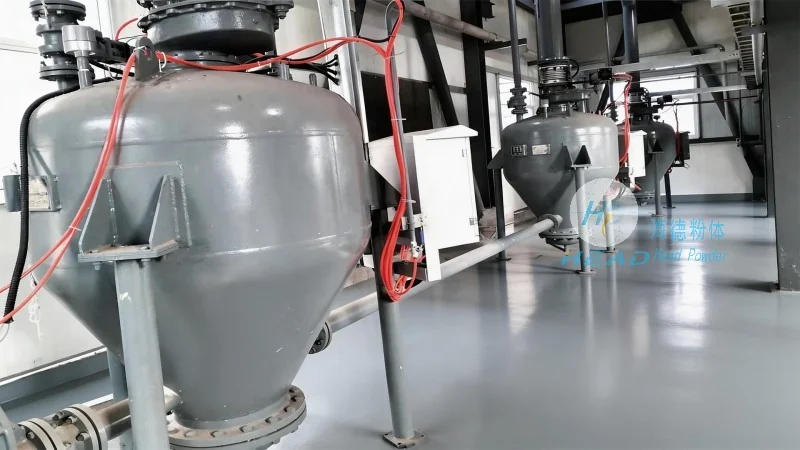
Once the material enters the conveying line, it is carried by the air flow through the pipeline. The system typically includes a series of components such as a rotary valve, a filter, and a silencer to ensure smooth and controlled transport. The rotary valve acts as a control mechanism, regulating the flow of material into the conveying line. The filter is used to capture any dust or particles that may be present in the material, protecting the equipment and maintaining air quality. The silencer reduces the noise generated by the system, making it suitable for use in various industrial environments.
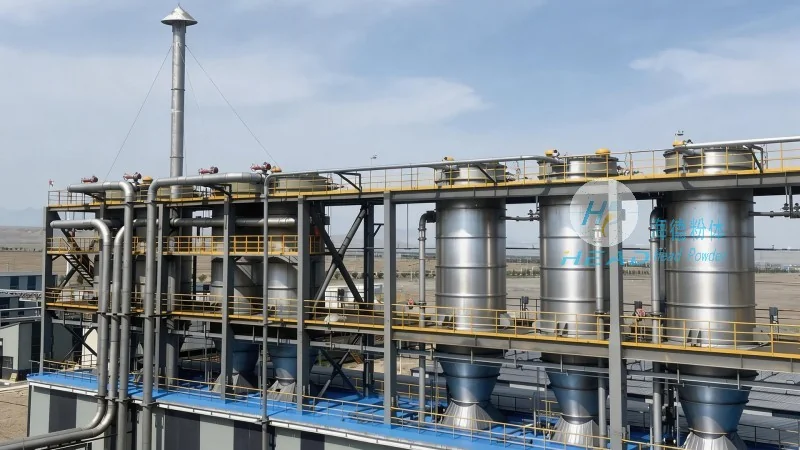
The material is then transported to the destination point, which could be a storage silo, a processing unit, or another container. At the destination, a rotary valve or a discharge valve is used to release the material into the receiving vessel. The system is designed to maintain a consistent flow rate and pressure, ensuring that the material is transferred safely and efficiently without any blockages or spills.
Key Features of the Automatic Bulk Bag Unloading Pneumatic Conveying System
The automatic bulk bag unloading pneumatic conveying system offers several key features that make it an ideal choice for industrial applications. One of the primary features is its ability to handle a wide range of materials, including powders, granules, and even fine particles. The system is designed to accommodate various bulk bag sizes and types, making it versatile and adaptable to different material handling needs.
Another important feature is the system's high efficiency and reliability. The pneumatic conveying method ensures that the material is transferred quickly and with minimal loss, reducing the risk of contamination and improving overall process efficiency. The system is also equipped with safety features such as pressure relief valves and emergency shut-off mechanisms to prevent accidents and ensure operator safety.
The system is also designed for easy maintenance and operation. The components are arranged in a modular fashion, allowing for easy access and replacement of parts. The control system is user-friendly, with intuitive interfaces that enable operators to monitor and control the system's performance. Additionally, the system is equipped with sensors and alarms that provide real-time feedback on the material flow and system status, enabling quick troubleshooting and maintenance.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial material handling equipment. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries that require reliable and efficient material transfer solutions. HeadPowder specializes in the design, manufacturing, and installation of pneumatic conveying systems, bulk bag unloading equipment, and other related products.
HeadPowder's team of experienced engineers and technicians work closely with clients to understand their specific material handling needs and provide customized solutions that meet their requirements. The company adheres to strict quality standards and uses advanced manufacturing techniques to ensure that its products are durable, efficient, and reliable. HeadPowder's products are widely used in various industries, including food and beverage, pharmaceuticals, chemicals, and mining.
HeadPowder is committed to providing excellent customer service and support. The company offers comprehensive after-sales services, including installation, training, and maintenance, to ensure that its clients can maximize the performance and lifespan of their equipment. With its headquarters in Shandong, China, HeadPowder serves clients both domestically and internationally, delivering high-quality products and services to meet the evolving needs of the industrial sector.




