Activated carbon, widely used in industrial processes for filtration, adsorption, and purification, presents unique challenges during material handling and transportation. Traditional methods such as manual loading, belt conveyors, or bucket elevators often struggle with dust generation, material degradation, and inefficiencies, especially when dealing with fine powders or bulk quantities. These challenges can lead to operational bottlenecks, increased maintenance costs, and environmental concerns related to dust emissions.
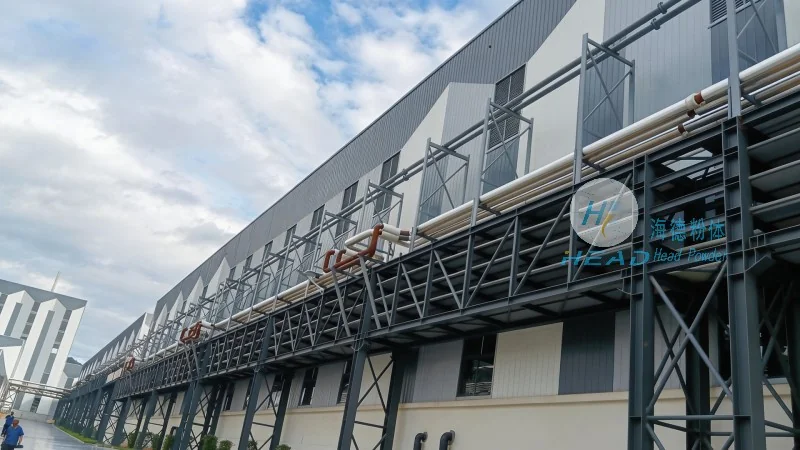
Recognizing these limitations, advanced pneumatic conveying systems have emerged as a reliable solution for activated carbon transport. Pneumatic conveying leverages air pressure to move bulk materials through pipelines, offering a closed-loop system that minimizes dust exposure and ensures consistent flow rates. This technology is particularly advantageous for activated carbon due to its fine particle size and the need for hygienic, dust-free handling in applications like water treatment, air purification, and chemical processing.
HeadPowder's Pneumatic Conveying Solutions: Tailored for Activated Carbon
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems optimized for activated carbon. The company's expertise lies in understanding the specific properties of activated carbon—such as its low bulk density, tendency to agglomerate, and sensitivity to moisture—and tailoring systems to address these challenges effectively. HeadPowder's solutions are engineered to ensure high efficiency, low maintenance, and compliance with industrial standards for safety and environmental protection.
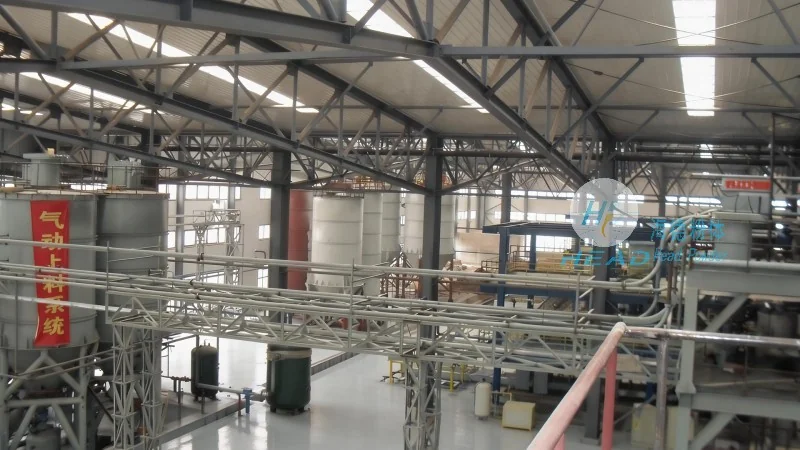
Key features of HeadPowder's pneumatic conveying systems include: a) Customizable pipeline configurations to accommodate varying plant layouts; b) Advanced control systems for precise flow regulation and pressure management; c) Durable materials of construction, such as stainless steel or corrosion-resistant alloys, to withstand the abrasive nature of activated carbon; d) Integrated dust collection and filtration units to maintain air quality and meet regulatory requirements. These features collectively enhance the reliability and longevity of the conveying process, reducing downtime and operational costs for clients.
Benefits of Adopting Pneumatic Conveying for Activated Carbon
Implementing pneumatic conveying systems for activated carbon offers numerous benefits that address the pain points of traditional handling methods. Firstly, the closed-loop design significantly reduces dust generation, improving workplace safety and compliance with environmental regulations. This is critical in industries where air quality is a priority, such as water treatment facilities or pharmaceutical plants. Secondly, the system's ability to handle fine powders without degradation ensures that the activated carbon's adsorption capacity remains intact, preserving its effectiveness in downstream processes.
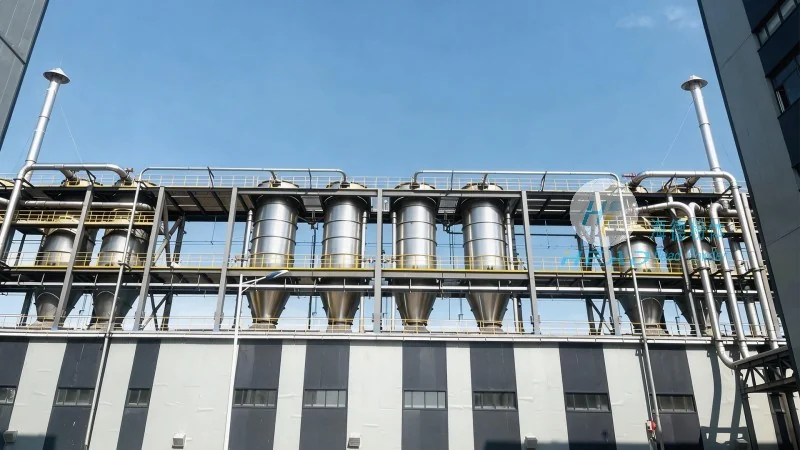
Thirdly, pneumatic conveying provides consistent and controlled material flow, which is essential for maintaining process stability in continuous operations. Unlike mechanical conveyors that may experience blockages or uneven flow, pneumatic systems deliver a steady stream of material, minimizing fluctuations in production output. This reliability translates to improved operational efficiency and reduced waste. Additionally, the compact design of pneumatic conveying systems allows for space-saving installations, making them suitable for both new plant constructions and retrofitting existing facilities.
Case Studies and Real-World Applications
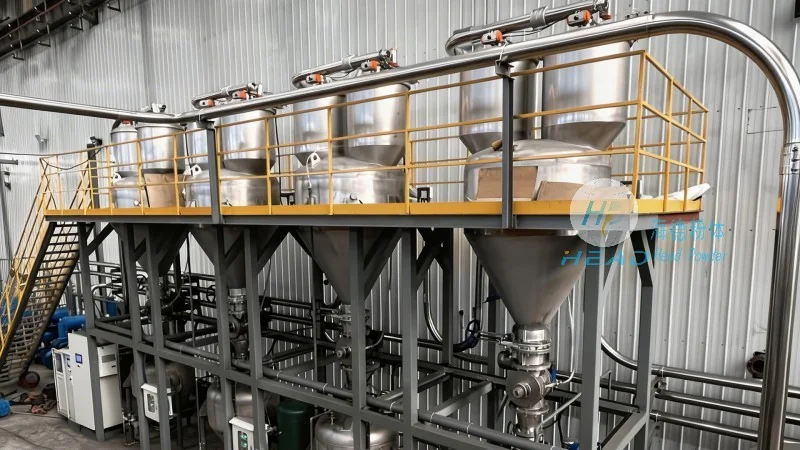
HeadPowder has successfully implemented pneumatic conveying solutions for activated carbon in various industrial settings. For example, a water treatment plant in China adopted a HeadPowder system to transport activated carbon from storage silos to filtration units. The system reduced dust emissions by 90% compared to traditional methods and increased material throughput by 25%, resulting in lower operational costs and improved water purification efficiency. Another client, a chemical processing facility, utilized HeadPowder's system to handle activated carbon in a closed-loop system for air purification, achieving a 95% reduction in airborne particulate matter and meeting stringent environmental standards.
Conclusion: The Future of Activated Carbon Handling
As industries continue to demand more efficient and sustainable material handling solutions, pneumatic conveying systems remain a top choice for activated carbon transport. HeadPowder Engineering, with its commitment to innovation and customer-centric design, continues to lead the way in providing reliable, high-performance systems that address the unique challenges of activated carbon. By leveraging advanced technology and tailored engineering, HeadPowder ensures that clients can optimize their operations, enhance safety, and achieve long-term success in their industrial processes.




