For industrial applications requiring efficient material handling, bulk bin pneumatic conveying systems offer a reliable solution. This article explores the working principle and key features of such systems, highlighting how they enhance operational efficiency and material transport in various industries.
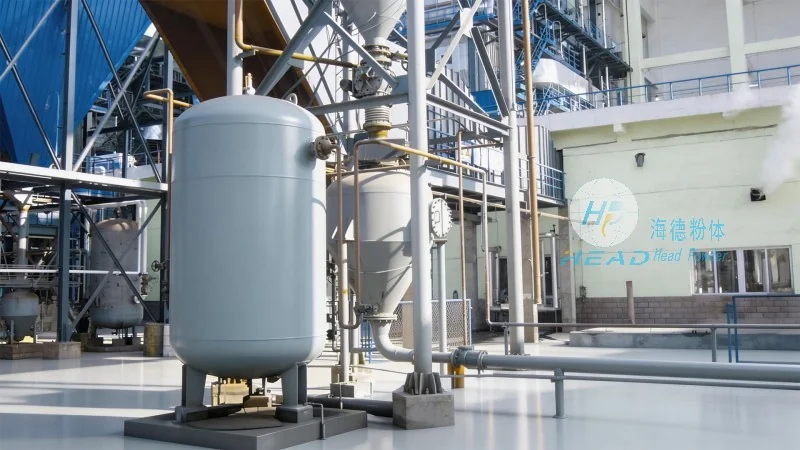
Working Principle of Bulk Bin Pneumatic Conveying Systems
Bulk bin pneumatic conveying systems operate by using compressed air to transport bulk materials from a storage bin to a processing or destination point. The process typically involves several key components: a bulk bin (storage hopper), a conveyor line, a blower or air compressor, and a control system. When material is needed, the control system activates the blower, which generates a high-velocity air stream. This air stream draws material from the bin through a hopper or feeder, creating a slurry of material and air. The mixture travels through the conveyor line to the discharge point, where the air is separated from the material, often using a cyclone or filter, and the material is deposited. The air is then recirculated back to the blower, completing the cycle. This method eliminates the need for mechanical components like belts or screws, reducing maintenance and increasing safety.
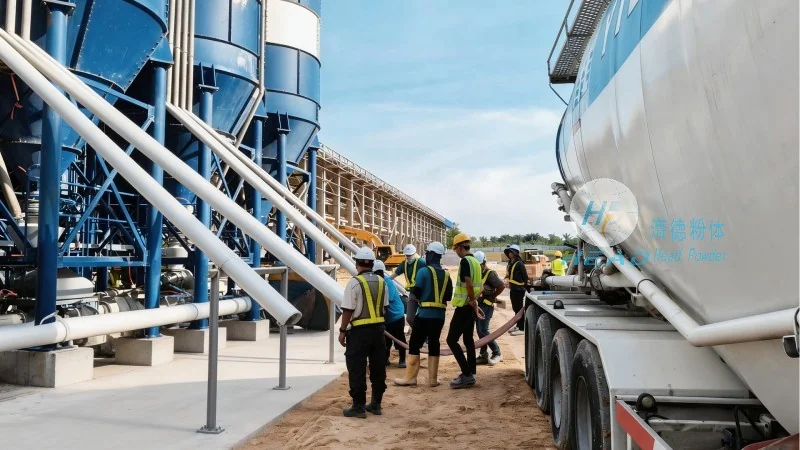
Key Features and Advantages of Bulk Bin Pneumatic Conveying Systems
HeadPowder's bulk bin pneumatic conveying systems are designed with several distinct features that set them apart in the industry. One primary advantage is the ability to handle a wide range of materials, from fine powders to bulk solids, with minimal degradation. The systems are also highly flexible, allowing for vertical, horizontal, or combined transport paths, adapting to the layout of the facility. Another critical feature is the low maintenance requirement, as there are no moving parts in direct contact with the material, which reduces wear and tear. Additionally, these systems offer excellent dust control, as the material is contained within the air stream, preventing airborne dust and improving workplace safety. The compact design of the bulk bin and conveyor line also saves space, making them suitable for both new installations and retrofitting into existing facilities. Furthermore, the systems are energy-efficient, with the air being recirculated, reducing overall operational costs.
Typical Applications in Industrial Settings
Bulk bin pneumatic conveying systems are widely used in various industries, including food processing, pharmaceuticals, chemicals, and mining. In food processing, they efficiently transport ingredients like flour, sugar, and spices from storage bins to production lines, ensuring hygiene and preventing contamination. In the pharmaceutical industry, the systems handle sensitive powders, maintaining strict contamination control and meeting regulatory standards. Chemical manufacturers benefit from the ability to transport hazardous materials safely, as the enclosed system prevents exposure to personnel. Mining operations use these systems to move bulk minerals from storage bins to processing equipment, improving material flow and reducing downtime. The versatility of the system makes it adaptable to different material types and operational needs, providing a consistent and reliable solution for material handling.
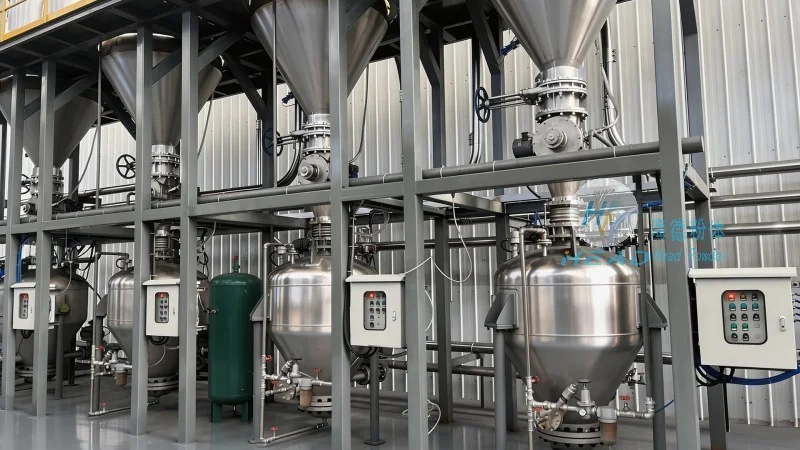
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of bulk bin pneumatic conveying systems, is dedicated to providing high-quality, efficient material handling solutions. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's systems are engineered to meet the specific needs of each client, ensuring optimal performance and reliability. The company's headquarters is located in Shandong, China, where it leverages advanced technology and skilled expertise to develop cutting-edge solutions. By combining years of experience with modern engineering, HeadPowder delivers systems that enhance productivity and safety in industrial applications.




