

What is Dust-Free Measuring Material Pneumatic Conveying? What Are Its Design Principles?
This section introduces the concept of dust-free pneumatic conveying systems designed for measuring and transporting materials. These systems are engineered to handle powders and granules with precision, ensuring minimal contamination and efficient material flow. The technology is widely used in industries where material purity is critical, such as pharmaceuticals, food processing, and chemical manufacturing. By maintaining a closed environment, these systems prevent dust dispersion, making them ideal for applications where product integrity and operator safety are paramount.
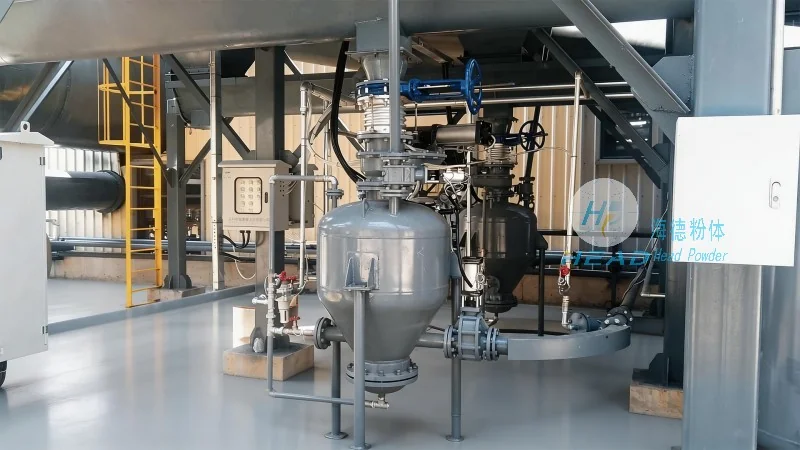
Understanding the Core Function of Dust-Free Pneumatic Conveying Systems
The primary function of dust-free pneumatic conveying is to transport bulk materials through a closed system using air or other gases. Unlike traditional methods, these systems maintain a controlled environment to prevent dust dispersion, making them ideal for applications where product integrity and operator safety are paramount. The system typically involves a hopper, a conveying line, and a receiver, all sealed to minimize particle release. This design ensures that the material remains contained throughout the entire conveying process, reducing the risk of contamination and environmental impact.
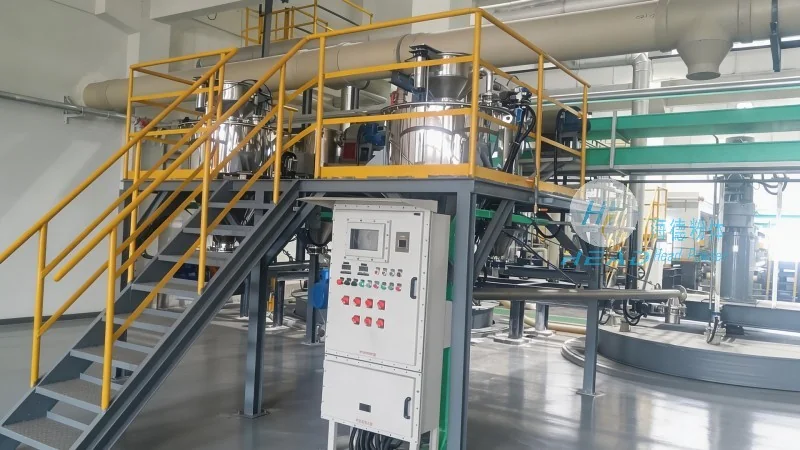
Design Principles Behind Dust-Free Material Handling Solutions
The design of dust-free pneumatic conveying systems follows several key principles to ensure efficiency and reliability. One critical principle is the use of positive pressure or negative pressure to move materials. Positive pressure systems push air and material through the line, while negative pressure systems draw material into the line. The choice depends on the material's properties, such as density and flowability. Another principle is the incorporation of filters and cyclones to separate material from air, ensuring that only clean air is released back into the environment. This separation process is essential for maintaining the purity of the conveyed material and complying with environmental regulations.
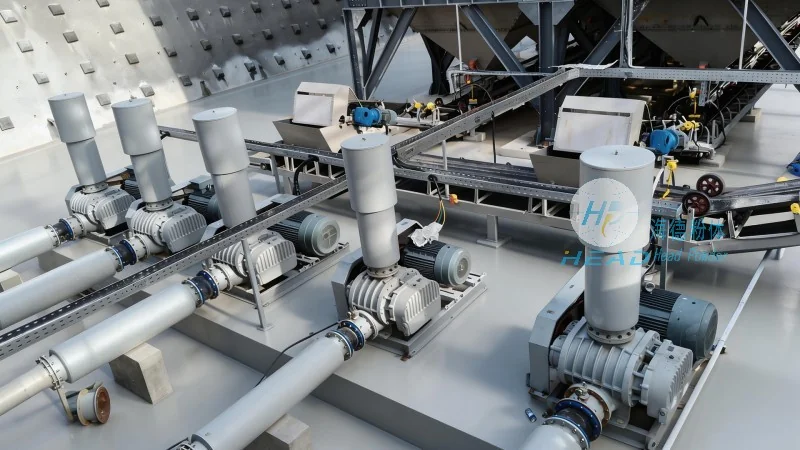
Key Components and Their Roles in the System
Several components work together to make a dust-free pneumatic conveying system effective. The hopper serves as the storage and feeding unit, where material is loaded and metered before being conveyed. The conveying line, often made of stainless steel or other corrosion-resistant materials, transports the material. The receiver collects the material at the destination, and a filter or cyclone unit separates the material from the air, preventing dust contamination. Additionally, control valves and sensors are used to regulate the flow and monitor system performance. These components are designed to work in harmony, ensuring smooth and consistent material transport.
Application Scenarios and Industry Benefits
Dust-free pneumatic conveying systems are applied in various industries where material purity and safety are essential. In the pharmaceutical industry, they are used to transport active pharmaceutical ingredients (APIs) and excipients without cross-contamination. In food processing, they handle ingredients like flour, sugar, and spices, maintaining product quality and meeting regulatory standards. In chemical manufacturing, they transport powders and granules, reducing the risk of dust explosions and ensuring consistent material handling. The benefits include improved product quality, reduced labor costs, and enhanced safety for operators. These systems also contribute to increased productivity by minimizing downtime and material loss.
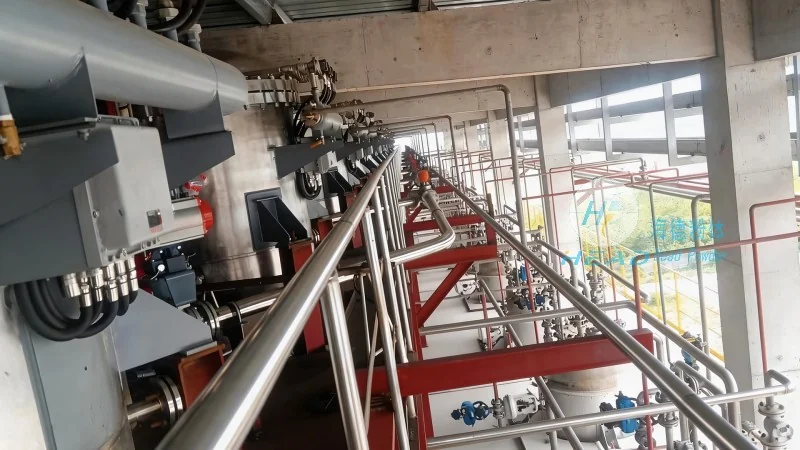
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of dust-free material handling solutions. With a focus on innovation and quality, the company designs and manufactures pneumatic conveying systems tailored to meet the specific needs of various industries. HeadPowder's products are engineered to provide reliable, efficient, and safe material transport, adhering to international standards and regulations. The company's headquarters is located in Shandong, China, where it continues to develop advanced technologies for the material handling industry. HeadPowder has built a reputation for delivering high-performance systems that enhance operational efficiency and ensure compliance with industry standards.