Water-in-powder material handling systems represent a specialized approach to transporting and managing dry powders, particularly in industrial applications where precise control over moisture content and material flow is critical. These systems integrate a water-based carrier with powdered materials to facilitate efficient and controlled movement, often used in sectors such as pharmaceuticals, food processing, and chemical manufacturing. The core objective of such systems is to ensure consistent material handling while maintaining product integrity and operational efficiency.
Design Principles of Water-in-Powder Systems
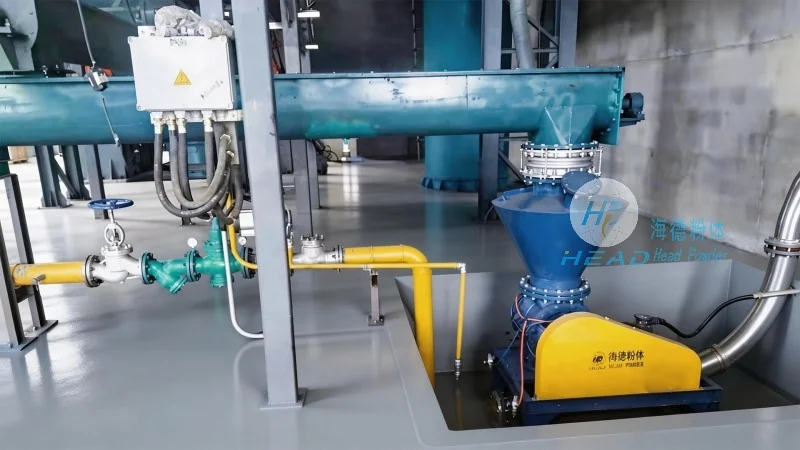
The design of a water-in-powder material handling system revolves around several key principles that ensure optimal performance. First, the system must effectively combine water with the powdered material to create a slurry or suspension, which allows for smooth transport through pipelines. This involves precise control over the water-to-powder ratio to prevent clogging or excessive moisture that could affect downstream processes. Second, the system employs pumps and pipelines specifically designed to handle the slurry, ensuring minimal pressure loss and consistent flow rates. Additionally, the design incorporates components like mixers and agitators to maintain the suspension's stability, preventing separation of the powder from the water carrier. Finally, the system includes filtration and separation mechanisms to recover the water and return it to the process, promoting sustainability and cost-effectiveness.
Key Components and Their Functions
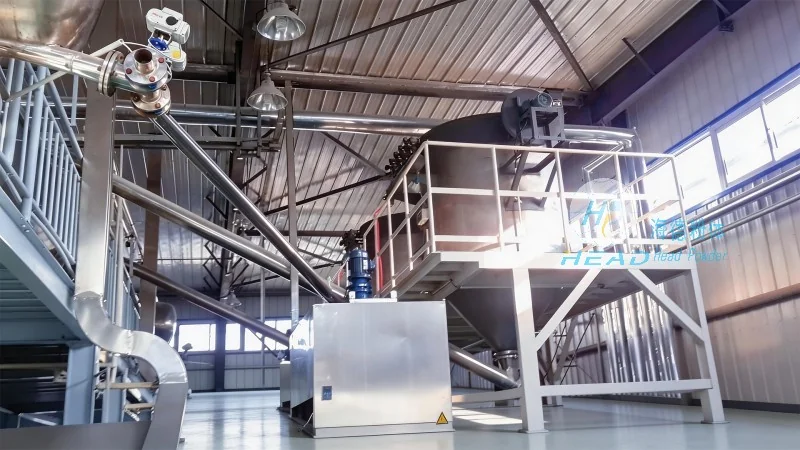
Several critical components make up a water-in-powder material handling system, each playing a vital role in the overall operation. The primary components include a water tank or reservoir, a powder feeder, a mixing chamber, a pump, and a pipeline network. The water tank supplies the carrier fluid, while the powder feeder accurately measures and dispenses the dry material. The mixing chamber is where the water and powder are combined, often using high-speed agitators to ensure a uniform slurry. The pump then transports the slurry through the pipelines to the destination, such as a storage tank or processing unit. The pipeline network may include valves, regulators, and sensors to monitor flow rates and pressure, ensuring the system operates within safe and efficient parameters. Additionally, filtration systems are integrated to separate the powder from the water, allowing the water to be recycled and the powder to be directed to its intended use.
Applications and Benefits in Industrial Settings
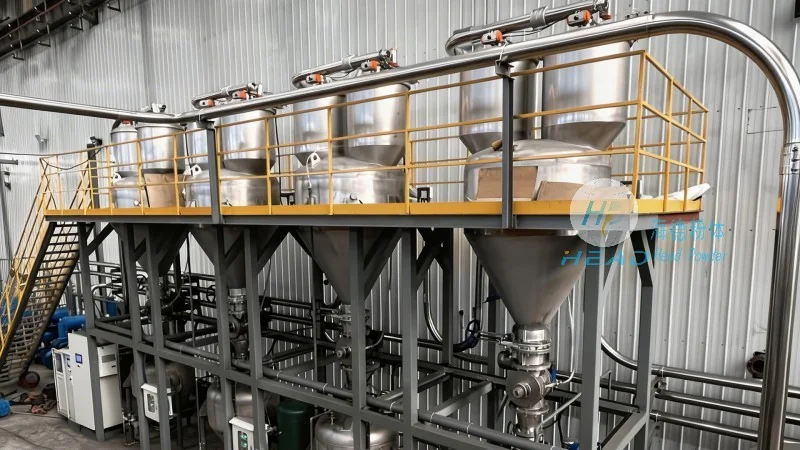
Water-in-powder material handling systems find extensive applications across various industries due to their ability to handle fine powders and maintain product quality. In the pharmaceutical industry, these systems are used to transport active pharmaceutical ingredients (APIs) and excipients, ensuring precise dosing and preventing contamination. In food processing, they facilitate the handling of powdered ingredients like spices, sugars, and dairy products, maintaining freshness and preventing caking. The chemical industry also benefits from these systems when transporting sensitive powders, such as catalysts or pigments, where moisture control is essential to prevent degradation. The primary benefits of using water-in-powder systems include improved material flow control, reduced dust generation, enhanced safety due to enclosed systems, and increased product consistency. Furthermore, the ability to recycle water reduces operational costs and minimizes environmental impact, making these systems a sustainable choice for modern industrial operations.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing water-in-powder material handling systems tailored to meet the unique needs of industrial clients. With a focus on innovation and quality, the company has established itself as a trusted partner in the field, offering customized solutions that enhance operational efficiency and product integrity. HeadPowder's expertise lies in understanding the specific challenges of powder handling, such as dust control, moisture management, and material flow, and developing systems that address these challenges effectively. The company's facilities, located in Shandong, China, are equipped with advanced technology and skilled personnel to ensure that each system is designed, manufactured, and tested to meet the highest industry standards. By combining technical expertise with customer-centric approaches, HeadPowder delivers reliable and efficient material handling solutions that help clients achieve their production goals while maintaining compliance with industry regulations.




