Coal and coke are essential raw materials in various industrial processes, particularly in the steel and chemical industries. Efficient handling and transportation of these materials are critical for maintaining production efficiency and safety. A coal and coke material handling system is a specialized setup designed to manage the movement of these bulk materials from storage to processing units. This system integrates various components such as conveyors, feeders, and storage silos to ensure smooth and reliable operation.
Key Components of a Coal and Coke Material Handling System
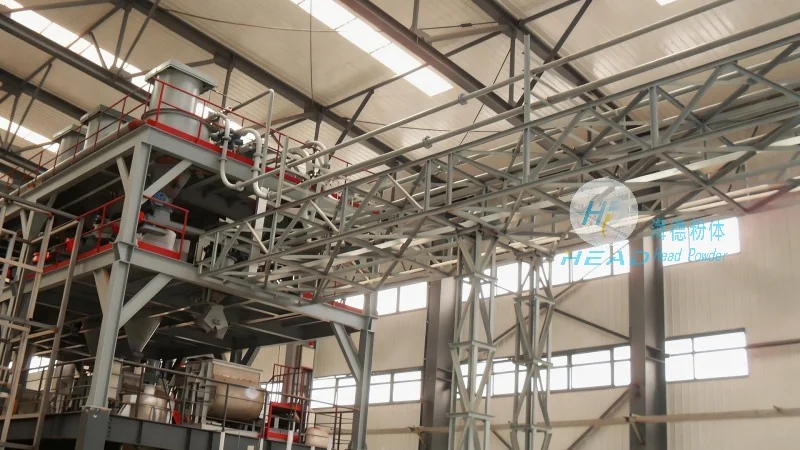
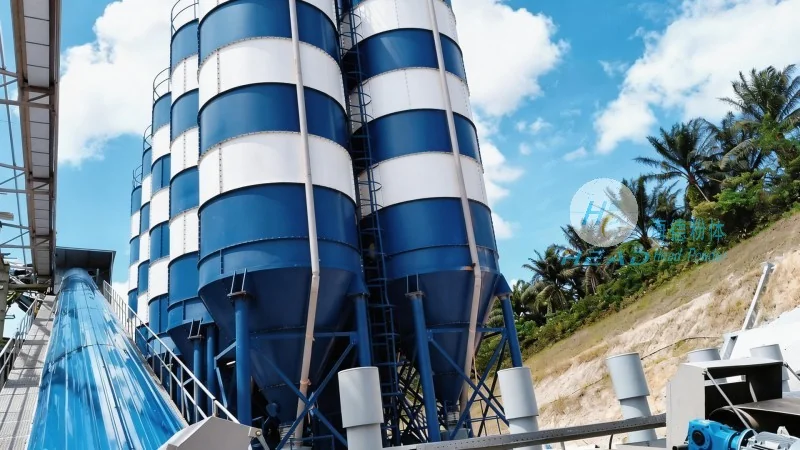
The design of a coal and coke material handling system involves several key components that work in tandem to achieve optimal performance. The primary components include bulk material conveyors, which can be belt conveyors, screw conveyors, or pneumatic conveyors, depending on the material characteristics and operational requirements. Feeders are used to regulate the flow of material from storage silos to the conveyors, ensuring consistent and controlled feeding. Storage silos or hoppers are crucial for storing large quantities of coal or coke, providing a buffer to meet varying production demands. Additionally, the system may include screening and crushing equipment to prepare the material for further processing, especially if the raw material contains impurities or requires size reduction.
Design Principles for Coal and Coke Material Handling Systems
The design principles of a coal and coke material handling system are centered on several critical factors to ensure durability, efficiency, and safety. First, the system must be designed to handle the specific physical properties of coal and coke, including their bulk density, moisture content, and abrasiveness. Coal and coke are often abrasive and can cause wear on equipment, so materials such as high-strength steel or wear-resistant coatings are used for components like conveyor belts and hoppers. Second, the system should be designed for high throughput and reliability, as these materials are typically used in large-scale industrial operations. This involves selecting appropriate conveyor capacities and ensuring proper maintenance schedules to minimize downtime. Third, safety is a paramount consideration. The system must incorporate safety features such as emergency stop mechanisms, dust suppression systems, and proper ventilation to protect operators and prevent accidents. Finally, the design should consider the overall layout and integration with other industrial processes, ensuring that the material handling system fits seamlessly into the existing production line.
HeadPowder's Expertise in Coal and Coke Material Handling Systems
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of coal and coke material handling systems. With years of experience in the industry, HeadPowder has developed a comprehensive range of solutions tailored to the unique needs of coal and coke handling. The company's team of engineers and technicians works closely with clients to understand their specific requirements, from raw material characteristics to production capacity, and designs systems that meet or exceed industry standards. HeadPowder's systems are known for their durability, efficiency, and safety features, ensuring that clients can rely on them for long-term operation. The company's commitment to quality and customer satisfaction has made it a trusted partner in the coal and coke handling industry.
Conclusion
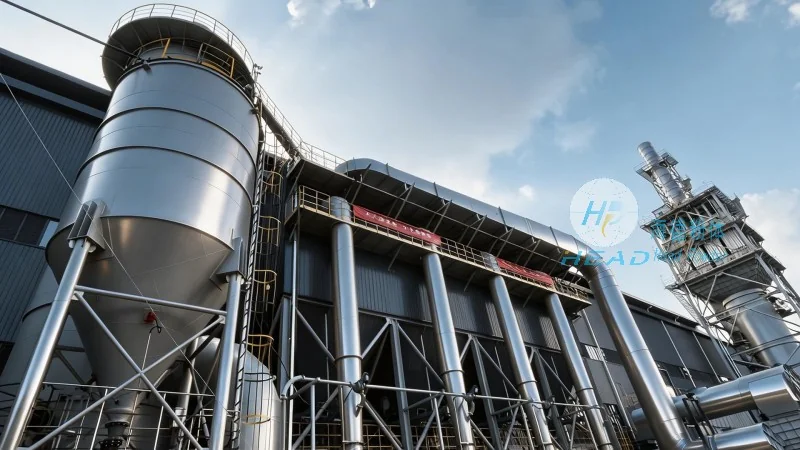
In conclusion, a coal and coke material handling system is a vital component in industrial operations, enabling the efficient and safe transportation of these essential raw materials. The design principles, which focus on material properties, throughput, safety, and integration, are crucial for the system's success. Companies like Shandong HeadPowder Engineering Co., Ltd. play a key role in providing specialized solutions that meet the demands of the industry, ensuring that coal and coke are handled effectively and reliably.




