Rare earth powder material conveying lines are specialized systems engineered to handle the transportation of rare earth powders, which are critical components in various high-tech industries such as electronics, aerospace, and renewable energy. These lines are designed to ensure efficient, safe, and reliable movement of these powders from one processing stage to another. The design principles behind these systems are tailored to address the unique properties of rare earth powders, including their fine particle size, hygroscopic nature, and potential for dust generation.
Key Design Principles for Rare Earth Powder Conveying Systems
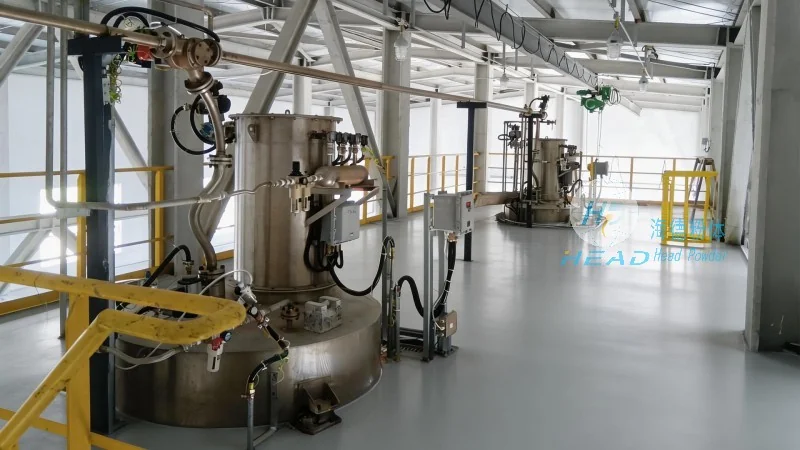
The design of a rare earth powder material conveying line is governed by several key principles that ensure optimal performance and safety. First, the system must maintain a closed environment to prevent dust contamination and environmental exposure. This is typically achieved through the use of sealed pipelines, dust collection systems, and proper ventilation. Second, the conveying equipment must be capable of handling fine powders without causing agglomeration or blockages. This often involves the selection of appropriate materials for the conveyor components, such as stainless steel or specialized coatings that resist corrosion and powder adhesion. Third, the system is designed to minimize material loss and ensure accurate dosing, which is crucial for maintaining product quality and consistency in downstream processes. Additionally, the design incorporates features for easy maintenance and cleaning to prevent cross-contamination and ensure compliance with industrial standards.
Components and Technologies Used in Rare Earth Powder Conveying Lines
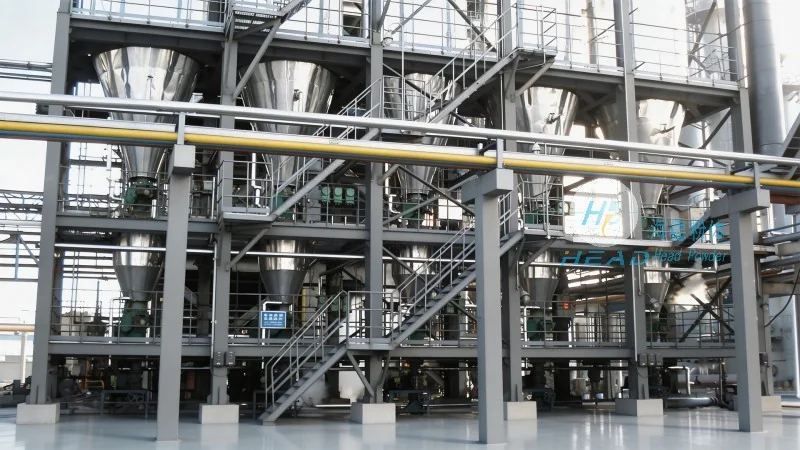
A typical rare earth powder material conveying line consists of several key components, each playing a vital role in the overall operation. The primary components include a feeding hopper, which is used to store and feed the rare earth powder into the system. The hopper is often equipped with a level indicator and a discharge valve to control the flow rate. Next, the conveying mechanism, which can be either pneumatic or mechanical. Pneumatic conveying systems use compressed air to transport the powder through pipelines, while mechanical systems employ screw conveyors, belt conveyors, or bucket elevators. For rare earth powders, pneumatic systems are often preferred due to their ability to handle fine powders without causing excessive wear. The pipeline system is designed with smooth, non-porous surfaces to prevent powder buildup and ensure consistent flow. Additionally, the system includes a dust collection and filtration unit to capture any airborne particles and return them to the process, maintaining a clean and safe working environment. The control system, which may include sensors for level, pressure, and flow monitoring, allows for real-time adjustment and optimization of the conveying process.
Applications and Benefits of Rare Earth Powder Conveying Lines
Rare earth powder material conveying lines are widely used in various industrial applications where the handling of fine powders is essential. In the electronics industry, these systems are used to transport rare earth powders for the production of magnets, catalysts, and other components. In the aerospace sector, they are employed in the manufacturing of high-performance alloys and materials. The benefits of using such specialized conveying lines include improved process efficiency, reduced material loss, enhanced safety through dust control, and consistent product quality. By maintaining a closed system and controlling the flow of powders, these lines minimize the risk of contamination and ensure that the rare earth powders remain in their optimal condition throughout the conveying process. This is particularly important for rare earth elements, which are often used in high-value applications where purity and consistency are critical.
About Shandong HeadPowder Engineering Co., Ltd.
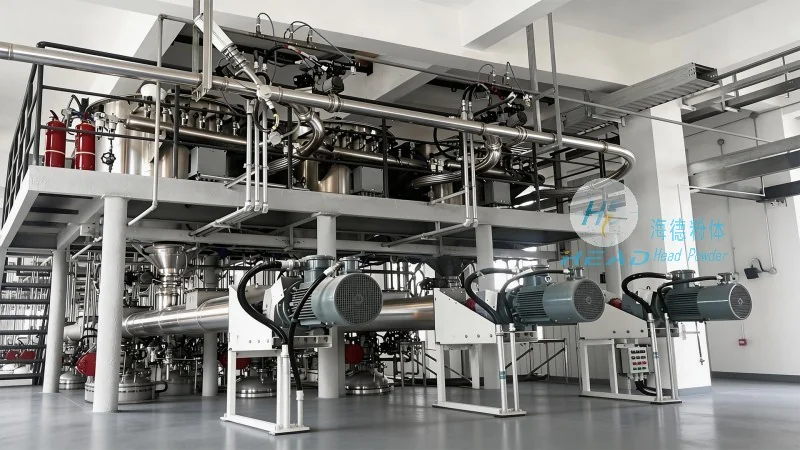
Shandong HeadPowder Engineering Co., Ltd., also known as headpowder, is a leading manufacturer and supplier of specialized material handling systems, including rare earth powder conveying lines. With a focus on innovation and quality, the company has developed advanced solutions tailored to the unique needs of the rare earth industry. HeadPowder's team of engineers and technicians work closely with clients to understand their specific requirements and design customized conveying systems that meet their operational and safety standards. The company's facilities are equipped with state-of-the-art technology and testing equipment to ensure that each system is manufactured to the highest standards. HeadPowder is committed to providing reliable, efficient, and safe material handling solutions that help clients optimize their production processes and enhance their competitive edge in the market. With its headquarters in Shandong, China, the company serves clients both domestically and internationally, delivering solutions that meet the demands of modern industrial applications.




