Efficient and environmentally friendly material handling is a critical concern for the fertilizer industry, where the safe and sustainable transport of granular materials like fertilizers is essential for operational success. Pneumatic conveying systems offer a superior alternative to traditional methods such as belt conveyors or bucket elevators, providing a solution that minimizes environmental impact while maximizing operational efficiency. This article explores the benefits of pneumatic conveying for fertilizer granules, highlighting the innovative solutions provided by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field.
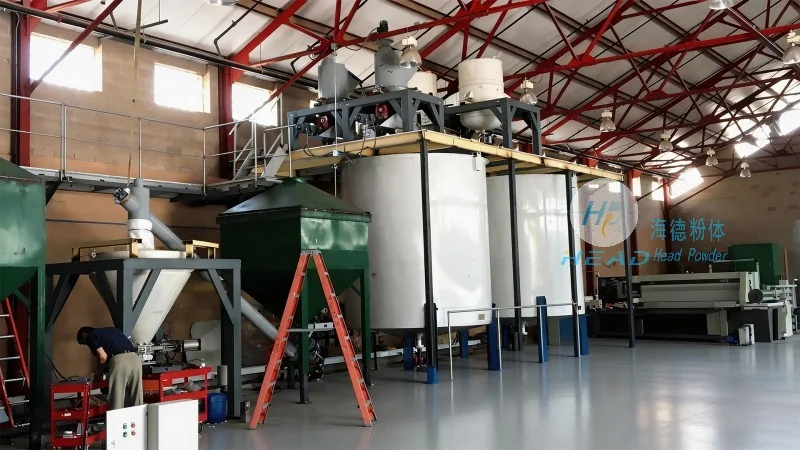
HeadPowder Engineering: A Trusted Name in Pneumatic Conveying Technology
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a prominent company specializing in the design, manufacturing, and installation of pneumatic conveying systems. With years of experience in the industry, HeadPowder has established itself as a reliable partner for businesses seeking advanced material handling solutions. The company's commitment to quality, innovation, and customer satisfaction has made it a preferred choice for clients across the fertilizer sector. HeadPowder's expertise lies in developing customized pneumatic conveying systems tailored to the specific needs of each client, ensuring optimal performance and cost-effectiveness.
Key Features of Pneumatic Conveying Systems for Fertilizer Granules
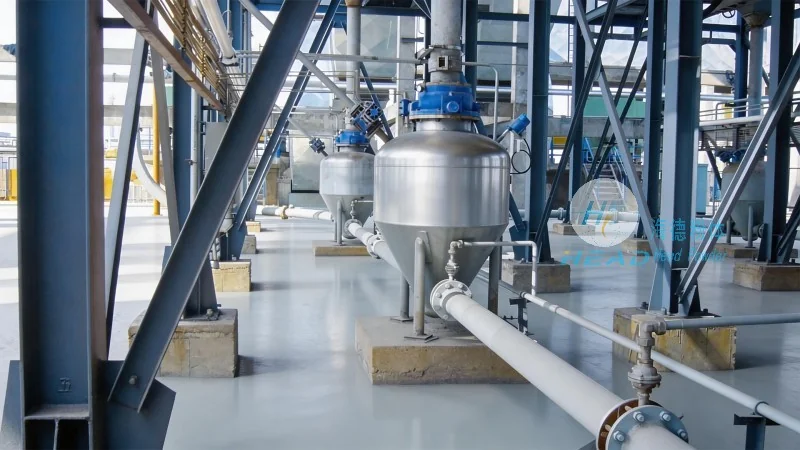
Pneumatic conveying systems for fertilizer granules utilize air to transport materials, eliminating the need for mechanical components that can cause wear and tear or contamination. This method offers several advantages, including reduced energy consumption, lower maintenance costs, and improved product quality. The systems are designed to handle a wide range of fertilizer granules, from nitrogen-based to phosphorus-based products, ensuring versatility and adaptability. HeadPowder's systems are equipped with advanced control mechanisms that allow for precise regulation of air flow and pressure, preventing material degradation and ensuring consistent product quality. Additionally, the enclosed nature of pneumatic conveying minimizes dust emissions, contributing to a cleaner and safer working environment.
Environmental Benefits and Sustainability
One of the most significant advantages of pneumatic conveying for fertilizer granules is its environmental impact. Unlike traditional methods that may generate dust and require additional cleaning processes, pneumatic systems are enclosed, reducing air pollution and minimizing the risk of product contamination. This not only complies with environmental regulations but also enhances workplace safety by eliminating exposure to harmful dust particles. Furthermore, the energy efficiency of pneumatic conveying systems contributes to lower carbon emissions, aligning with global sustainability goals. HeadPowder's commitment to environmental responsibility is reflected in the design of their systems, which incorporate energy-saving features and eco-friendly materials, making them a sustainable choice for the fertilizer industry.
Operational Efficiency and Cost Savings
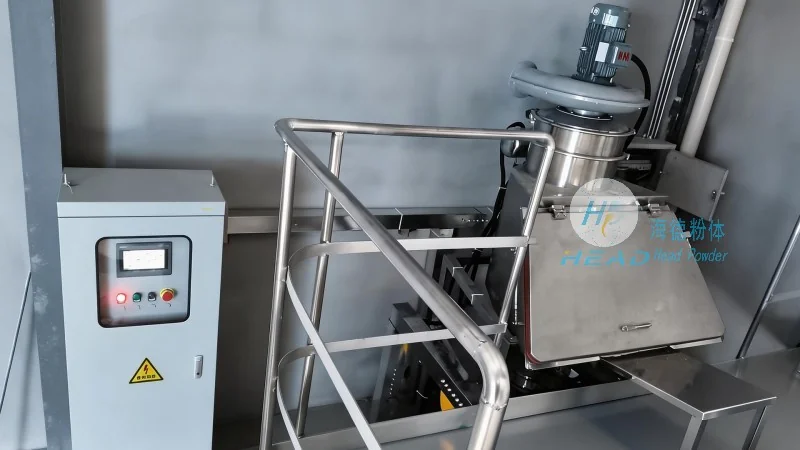
Pneumatic conveying systems for fertilizer granules offer substantial operational efficiency and cost savings compared to traditional methods. The enclosed design reduces downtime due to maintenance and cleaning, as there is no need for frequent belt replacement or cleaning of dust accumulation. This leads to increased productivity and reduced labor costs. Additionally, the precise control of air flow allows for optimal material transport, minimizing waste and maximizing throughput. HeadPowder's systems are engineered to handle high volumes of fertilizer granules with minimal energy input, resulting in lower operational costs over the long term. The company's expertise in system integration ensures that clients can achieve seamless operation, from raw material intake to final product delivery, enhancing overall operational efficiency.
Customized Solutions for Diverse Fertilizer Applications
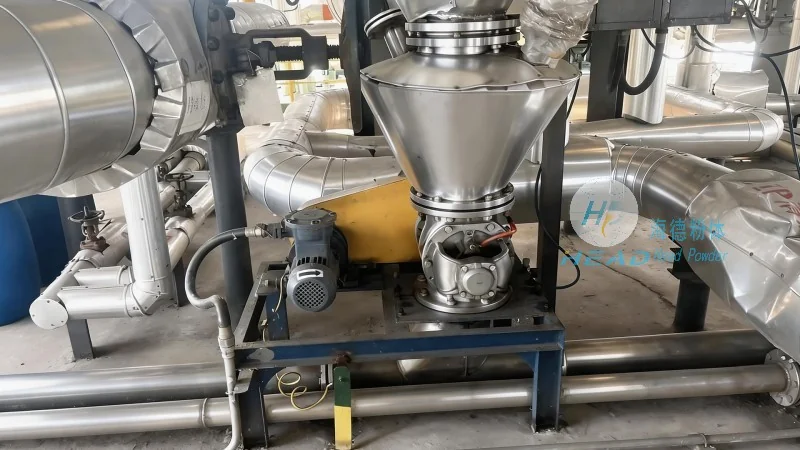
HeadPowder understands that the fertilizer industry requires tailored solutions to meet the unique demands of different applications. Whether handling bulk granules for agricultural use or specialized fertilizers for industrial processes, the company's pneumatic conveying systems are designed to accommodate diverse requirements. The systems can be configured for both positive and negative pressure operations, allowing flexibility in material transport. HeadPowder's engineers work closely with clients to assess their specific needs, including material characteristics, transport distances, and operational constraints, to develop a customized solution that meets all requirements. This approach ensures that clients receive a system that is not only efficient but also reliable and durable, providing long-term value.
Conclusion: The Future of Fertilizer Material Handling
As the fertilizer industry continues to evolve, the demand for efficient and sustainable material handling solutions remains high. Pneumatic conveying systems, particularly those designed by HeadPowder Engineering, offer a compelling solution that addresses the industry's key challenges. By combining advanced technology with environmental responsibility, these systems provide a pathway to improved operational efficiency, reduced costs, and enhanced sustainability. For businesses seeking to upgrade their material handling processes, HeadPowder's pneumatic conveying solutions represent a forward-thinking investment that aligns with both current and future industry needs. With a strong commitment to quality and customer satisfaction, HeadPowder is well-positioned to support the fertilizer industry's transition to more efficient and eco-friendly practices.




