For industrial applications requiring efficient dust collection and powder handling, the pulse jet dust collector powder conveying line has emerged as a critical system. This article explores the fundamental aspects of this technology, focusing on its design principles and the role of companies like Shandong HeadPowder Engineering Co., Ltd. in providing advanced solutions.
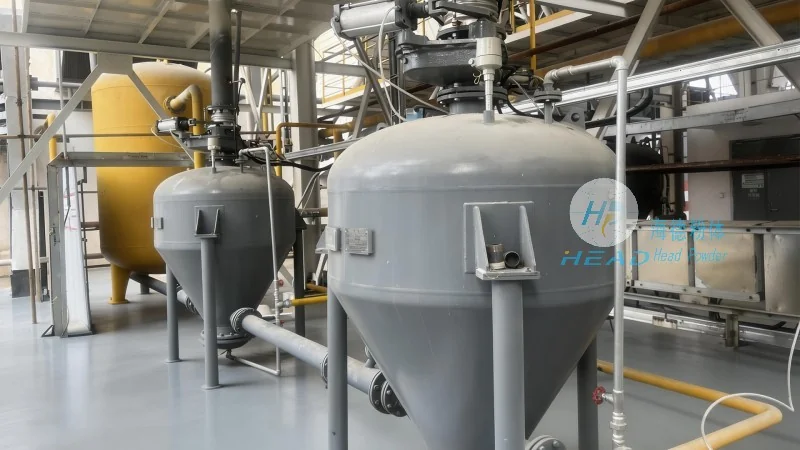
Introduction to Pulse Jet Dust Collector Powder Conveying Lines
A pulse jet dust collector powder conveying line is a specialized system designed to capture airborne particles and transport powders through a network of ducts and filters. It combines the functionality of a dust collector with a powder conveying mechanism, making it ideal for industries such as chemical processing, pharmaceutical manufacturing, and food processing where both air purification and material handling are essential. The system operates by drawing contaminated air into a filtration chamber, where dust particles are trapped by a series of filter bags. Simultaneously, it conveys powders from a hopper or storage tank to processing equipment, ensuring a continuous and clean operation.
Design Principles of the System
The core design principle of a pulse jet dust collector powder conveying line revolves around the use of compressed air pulses to clean the filter bags and maintain optimal filtration efficiency. When dust accumulates on the filter bags, the pressure drop across the filter increases, triggering a cleaning cycle. During this cycle, a high-pressure pulse of air is injected into each filter bag through a pulse valve. This pulse dislodges the collected dust, which then falls into a hopper for removal. The design also incorporates a dust hopper and a conveying system that uses the same air flow to transport the collected powder back to the processing line or storage area. The system is engineered to balance filtration efficiency with the need for regular maintenance, ensuring long-term performance and minimal downtime.
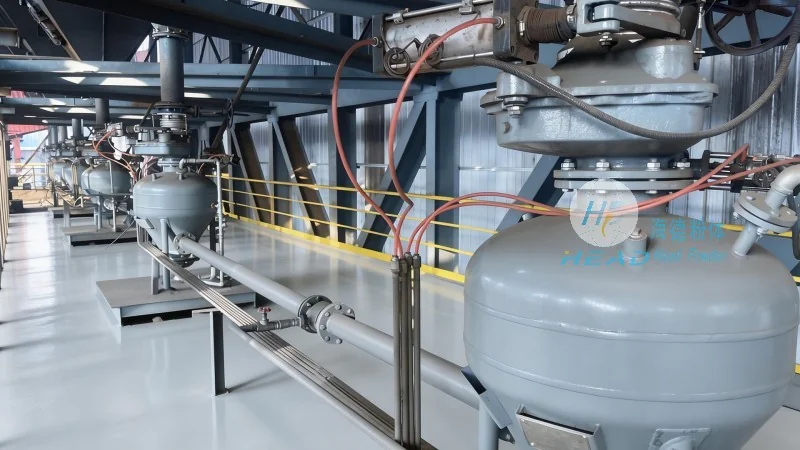
Key Components and Their Functions
Several critical components work in tandem to ensure the effective operation of a pulse jet dust collector powder conveying line. The filter housing, typically made of metal or high-strength plastic, houses the filter bags and provides structural support. The filter bags, often made of synthetic fibers like polyester or polypropylene, are the primary filtration media, capturing fine particles from the air stream. The pulse valve, a crucial component, controls the release of high-pressure air pulses to clean the bags. It is usually a solenoid valve that opens and closes rapidly to deliver the cleaning pulses. The air tank or compressor supplies the compressed air needed for the cleaning process, while the dust hopper collects the dislodged dust and may include a discharge mechanism for removal. The conveying ducts connect the filter housing to the powder source and processing equipment, ensuring a smooth flow of material. Each component is designed to withstand the operational pressures and temperatures typical of industrial environments, contributing to the overall reliability of the system.
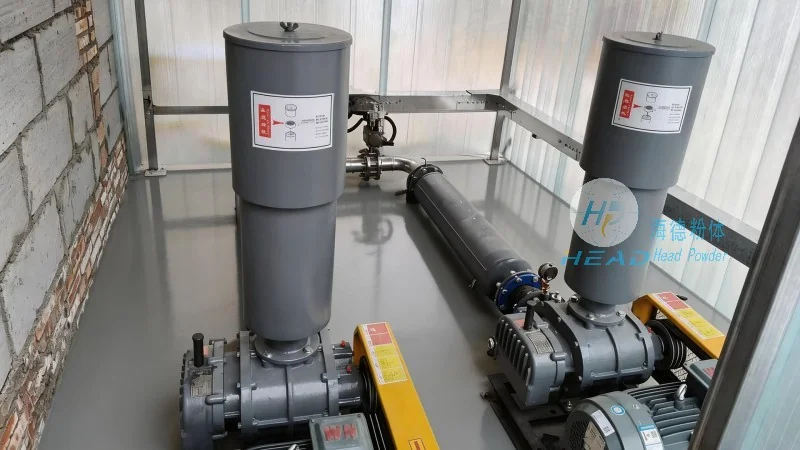
HeadPowder's Expertise in Powder Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of advanced powder handling and dust collection systems. The company specializes in designing and manufacturing pulse jet dust collector powder conveying lines tailored to the specific needs of various industries. With years of experience in the field, HeadPowder leverages cutting-edge technology and rigorous engineering standards to deliver systems that meet or exceed industry benchmarks. The company’s commitment to quality is reflected in its use of high-grade materials, precise manufacturing processes, and comprehensive testing protocols. Additionally, HeadPowder offers technical support and maintenance services to ensure that its clients can maximize the performance and lifespan of their equipment. By partnering with HeadPowder, businesses can benefit from reliable, efficient, and cost-effective solutions that enhance productivity and improve air quality in their operations.
Applications and Benefits
The pulse jet dust collector powder conveying line finds wide application across multiple sectors due to its versatility and effectiveness. In the chemical industry, it is used to handle powders such as pigments, polymers, and catalysts, ensuring that the production process remains clean and free from contamination. In pharmaceutical manufacturing, the system helps maintain stringent air quality standards, which are critical for producing high-purity drugs. The food processing industry also benefits from this technology, as it enables the safe handling of powders like flour, sugar, and spices while preventing cross-contamination. The primary benefits of the pulse jet dust collector powder conveying line include high filtration efficiency, which can reach up to 99.9% for fine particles, and reliable powder conveying capabilities that minimize material loss and improve process consistency. Additionally, the system is designed for low maintenance, with automated cleaning cycles reducing the need for manual intervention. This not only lowers operational costs but also enhances worker safety by minimizing exposure to dust and other airborne contaminants.




