Industrial applications frequently require the efficient and safe transport of bulk materials, and copper sulfate is a key chemical in many processes. The use of pneumatic conveying systems for copper sulfate offers a reliable solution, ensuring material handling that minimizes dust exposure and optimizes operational efficiency. This article explores the structure and working principles of such equipment, highlighting the technical aspects that make it suitable for handling this specific material.
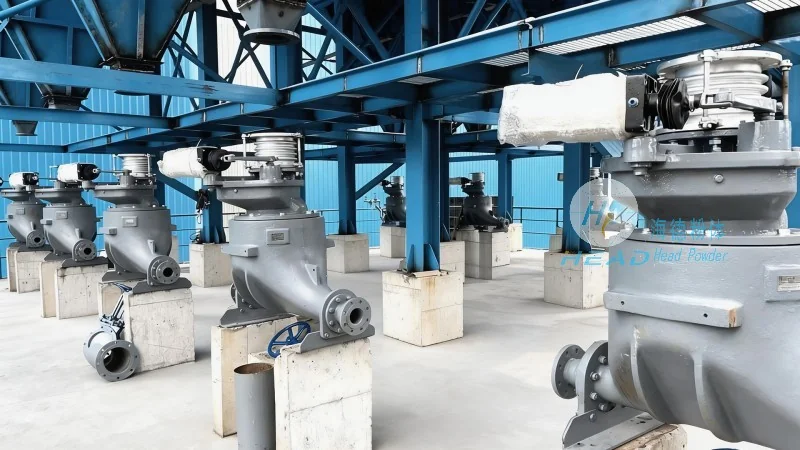
HeadPowder Engineering Co., Ltd.: A Leading Provider of Powder Handling Solutions
HeadPowder Engineering Co., Ltd., a company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced powder handling equipment. With a focus on precision engineering and customer-centric solutions, HeadPowder has established itself as a trusted partner in the chemical processing industry. The company's expertise in material handling systems ensures that equipment is tailored to meet the unique requirements of each application, including those involving copper sulfate.
Understanding Pneumatic Conveying Systems for Copper Sulfate
Pneumatic conveying equipment is designed to transport bulk materials like copper sulfate through a pressurized or vacuum system. The system typically consists of several key components, each playing a critical role in the overall operation. These components include a material feed hopper, a conveying line (often made of corrosion-resistant materials such as stainless steel), a separation unit, and a control system. The design of the system is tailored to the physical properties of copper sulfate, such as its particle size, density, and moisture content, to ensure efficient and safe transport.
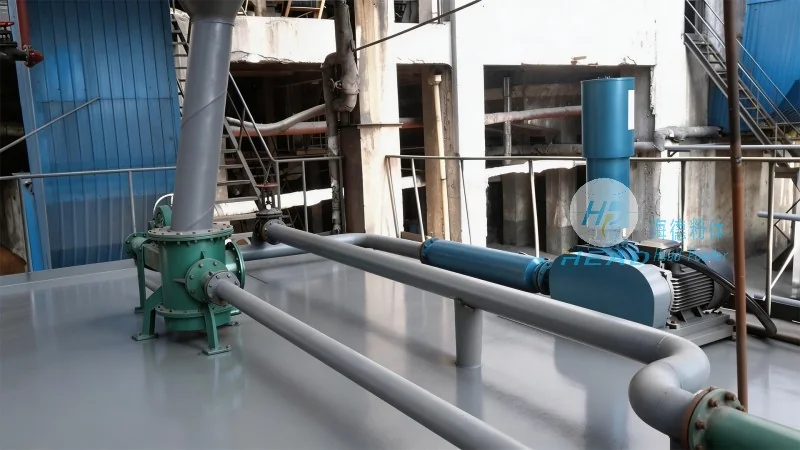
Key Structural Components of Copper Sulfate Pneumatic Conveying Equipment
The structural design of the equipment is crucial for the effective handling of copper sulfate. The feed hopper is engineered to accommodate the bulk material and provide a controlled feed rate, preventing overloading or blockages. The conveying line is constructed from materials that resist corrosion, as copper sulfate can be chemically aggressive. Stainless steel or specialized alloys are commonly used to ensure durability and longevity. The separation unit, such as a cyclone or bag filter, is designed to separate the conveyed material from the air stream, ensuring that the copper sulfate is collected efficiently and without loss. The control system integrates sensors and valves to regulate the flow of material and air, maintaining optimal operating conditions.
Working Principle of the Pneumatic Conveying Process
The operation of the copper sulfate pneumatic conveying system involves the creation of a flow of air through the conveying line. In an aspirated system, a vacuum is created at the receiving end, drawing the copper sulfate particles into the line along with the air. In a pressurized system, air is forced through the line, pushing the material forward. The air velocity is carefully controlled to ensure that the particles are carried without causing excessive wear or degradation. The system's design ensures that the copper sulfate remains in a dry, free-flowing state throughout the process, minimizing the risk of caking or agglomeration.
Advantages of Using Pneumatic Conveying for Copper Sulfate
Implementing a pneumatic conveying system for copper sulfate offers several advantages over traditional methods. Firstly, it provides a dust-free environment, reducing health hazards and improving workplace safety. Secondly, the system is highly efficient, with minimal material loss and reduced downtime due to blockages. Thirdly, the equipment is compact and can be integrated into existing production lines, making it a cost-effective solution. Additionally, the system allows for precise control over the flow rate and pressure, ensuring consistent performance and product quality.
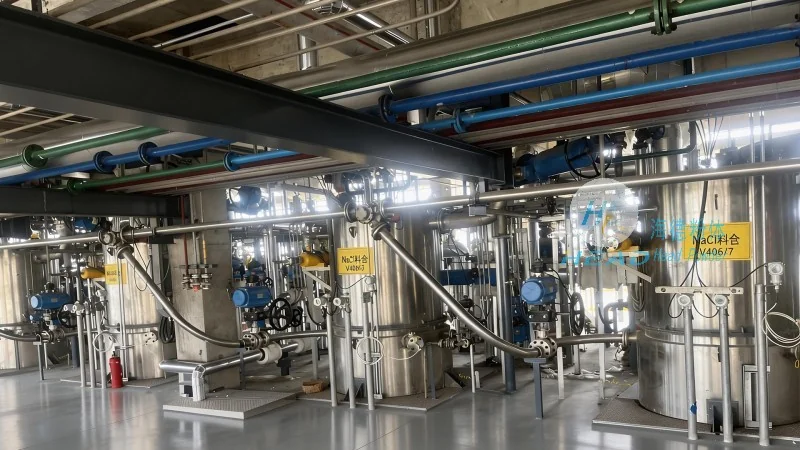
Application Examples in Industrial Settings
Copper sulfate pneumatic conveying equipment is widely used in various industrial applications. In the chemical industry, it is employed in the production of fertilizers, pigments, and other copper-based compounds. In the pharmaceutical sector, the system ensures the safe and hygienic transport of copper sulfate used in drug formulations. The equipment is also utilized in water treatment facilities, where copper sulfate is used as a coagulant. In each of these applications, the system's ability to handle the material efficiently and safely is critical to operational success.
Conclusion: The Role of Advanced Powder Handling in Copper Sulfate Processing
As the demand for copper sulfate continues to grow, the importance of reliable and efficient material handling systems cannot be overstated. Pneumatic conveying equipment, with its advanced structural design and working principles, provides an effective solution for transporting copper sulfate in industrial settings. Companies like HeadPowder Engineering Co., Ltd. play a vital role in delivering these systems, ensuring that the material is handled safely, efficiently, and in compliance with industry standards. By leveraging the expertise in powder handling, industries can enhance their operational performance and maintain high product quality.




