HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced solutions for powder material handling. The dust-free bulk bag loading station is a critical component in modern industrial processes, designed to ensure efficient and safe transfer of bulk materials from bulk bags into processing equipment.
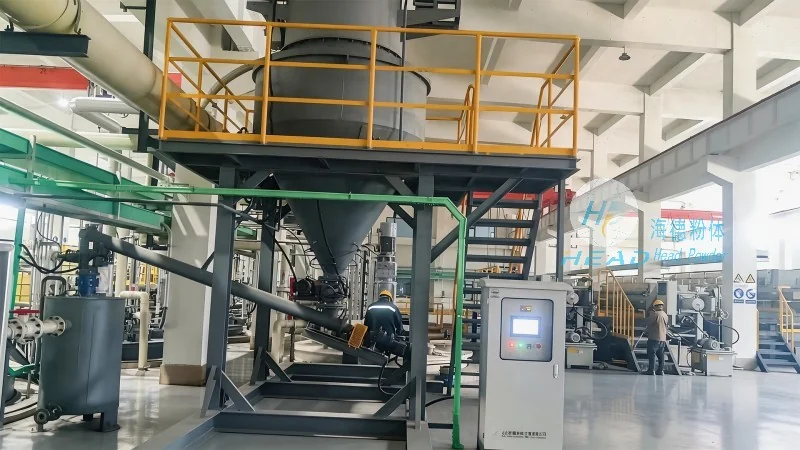
Overview of the Dust-Free Bulk Bag Loading Station
The dust-free bulk bag loading station is engineered to minimize dust generation and exposure during the material transfer process. It integrates a series of components that work in tandem to achieve a clean and controlled environment. This system is particularly valuable in industries such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining product purity and operator safety is paramount.
Key Components and Structure
The system comprises several key components, each playing a vital role in the overall operation. The primary structure includes a bulk bag support frame, a hopper with a discharge valve, an air filtration system, and a material transfer mechanism. The bulk bag is securely placed on the support frame, which is designed to accommodate various bag sizes and weights. The hopper, positioned above the bag, collects material from the bag and channels it through the discharge valve. The air filtration system is crucial for capturing and filtering dust particles, ensuring that the air remains clean and safe for the operators.
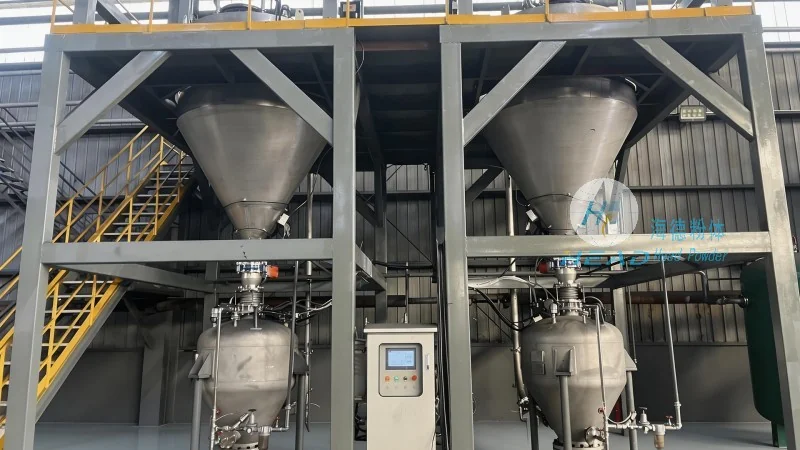
Working Principle of the Powder Material Handling System
The operation of the dust-free bulk bag loading station follows a systematic process. First, the bulk bag is positioned on the support frame, and the bag's top is opened to allow material to flow. The hopper then begins to draw material from the bag, using a combination of gravity and controlled air flow if necessary. The discharge valve regulates the flow rate, preventing overloading and ensuring a steady transfer. The air filtration system continuously captures any dust particles that may be generated during the process, preventing them from entering the workspace or contaminating the material.
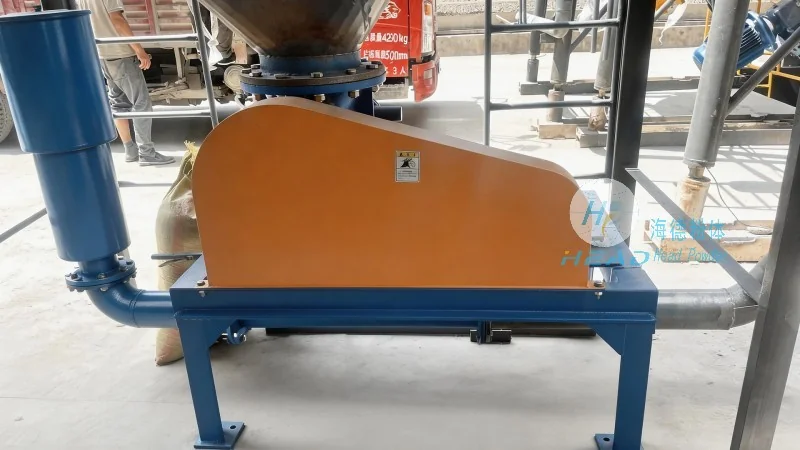
Advantages and Applications
Implementing a dust-free bulk bag loading station offers numerous advantages. It significantly reduces dust exposure, enhancing operator safety and compliance with health regulations. The system also improves material handling efficiency by automating the transfer process, reducing downtime and labor costs. Additionally, it maintains product quality by preventing contamination from external sources. The system is widely used in industries where bulk materials are handled, including chemicals, food products, and pharmaceuticals, where precision and cleanliness are essential.
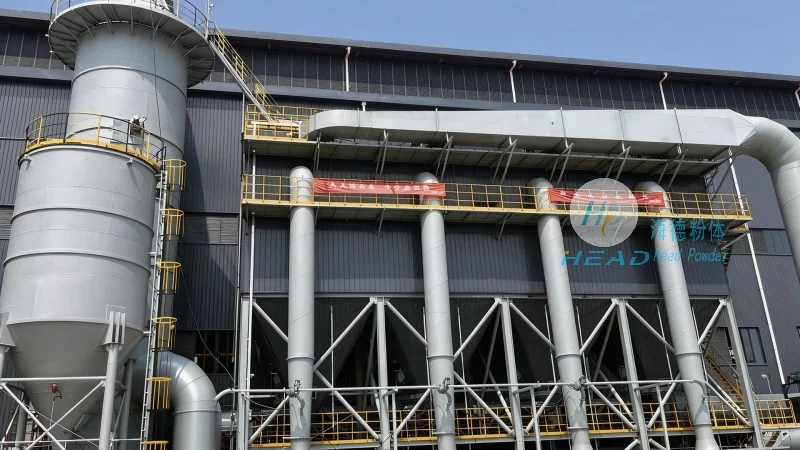
Customization and Integration
HeadPowder understands that different industrial applications have unique requirements. Therefore, the dust-free bulk bag loading station can be customized to meet specific needs. This includes adjustments to the hopper size, discharge valve type, and air filtration capacity. The system can also be integrated with existing processing equipment, such as mixers or reactors, to create a seamless material handling workflow. Customization ensures that the system operates optimally in the specific environment, maximizing efficiency and minimizing operational challenges.
Maintenance and Safety Considerations
Proper maintenance is essential to ensure the long-term performance and safety of the dust-free bulk bag loading station. Regular inspections of the air filtration system, discharge valve, and support frame are necessary to identify and address any potential issues. The system should be cleaned and serviced according to the manufacturer's guidelines to maintain its efficiency. Safety is a top priority, and the station is equipped with features such as dust extraction ports and emergency stop buttons to protect operators. Training for personnel on the proper operation and maintenance of the system is also crucial to prevent accidents and ensure compliance with safety standards.




