Ammonium sulfate, a vital fertilizer and industrial chemical, demands efficient material handling solutions for its transportation. Pneumatic conveying technology has become a cornerstone for moving this material, offering benefits such as reduced dust, enhanced safety, and improved process control. This article explores the technical nuances of pneumatic conveying for ammonium sulfate, focusing on the two primary methods: vacuum and positive pressure systems. Understanding the distinctions and applications of each is crucial for selecting the most appropriate system for specific operational needs.
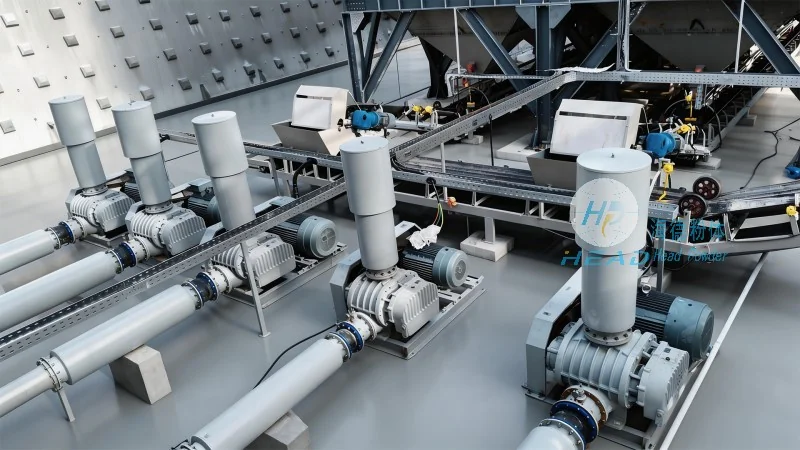
Vacuum Pneumatic Conveying Systems for Ammonium Sulfate
Vacuum pneumatic conveying systems operate by creating a negative pressure at the receiving end, drawing material from the source through a pipeline. This approach is particularly effective for transporting ammonium sulfate from storage silos or bulk containers to processing or packaging units. The system typically includes a vacuum pump, a hopper with a feeder, and a filter to separate material from the air stream. A key advantage of vacuum systems is their ability to convey materials over relatively short distances—often up to several hundred meters—with minimal pressure drop. They are also well-suited for applications where material is collected from multiple points, as the vacuum can be maintained at each source location.
The design of a vacuum system for ammonium sulfate must account for factors like the material's bulk density, flowability, and potential for bridging or caking. HeadPowder Engineering, a leading provider in the field, specializes in customizing vacuum conveying solutions that address these challenges. Their systems are engineered to ensure consistent material flow, preventing blockages and maintaining system efficiency. The company's expertise in material handling allows them to recommend the appropriate vacuum pump size and filter capacity, optimizing the conveying process for ammonium sulfate applications.
Positive Pressure Pneumatic Conveying Systems for Ammonium Sulfate
In contrast to vacuum systems, positive pressure pneumatic conveying generates positive pressure at the discharge end, pushing material through the pipeline. This method is ideal for long-distance transportation, often exceeding 1 kilometer, and for applications requiring high throughput. Positive pressure systems use a blower or compressor to create the pressure, moving material from the source to the destination. The system typically includes a hopper, a feeder, and a pressure vessel to store material before discharge.
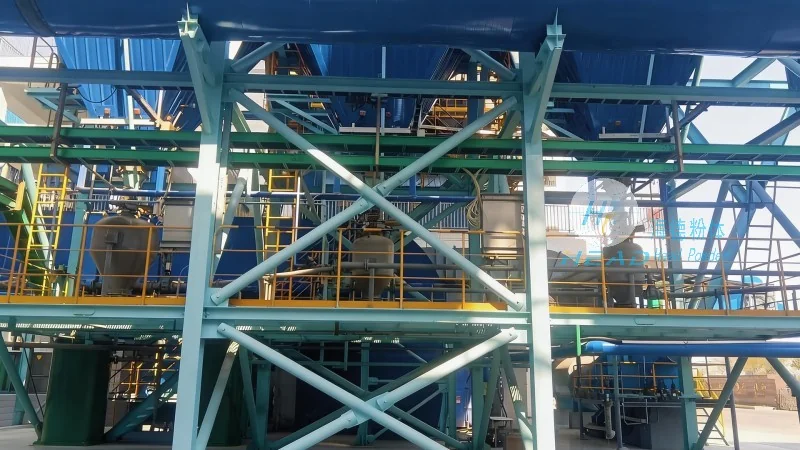
For ammonium sulfate, positive pressure systems offer several benefits, including the ability to handle abrasive materials without excessive wear on components. The positive pressure also helps maintain material integrity, reducing the risk of degradation during transport. HeadPowder Engineering's positive pressure solutions are designed with durable materials and efficient blowers to ensure long-term performance. Their systems are capable of handling high volumes of ammonium sulfate, making them suitable for large-scale industrial operations. The company's engineers work closely with clients to determine optimal pressure levels and pipeline configurations, ensuring the system meets specific application requirements.
Key Considerations and Application Scenarios
When selecting between vacuum and positive pressure pneumatic conveying for ammonium sulfate, several factors must be evaluated. The distance between the source and destination is a primary consideration, as vacuum systems are generally limited to shorter distances, while positive pressure systems are better suited for longer runs. The material's characteristics—such as flowability and tendency to clog—also play a role. For example, if the ammonium sulfate is prone to bridging, a positive pressure system with a high-pressure blower might be more effective in breaking up the material and maintaining flow.
Another critical factor is environmental impact and safety considerations. Vacuum systems are often preferred in applications where dust control is paramount, as the negative pressure helps contain particles within the system. Positive pressure systems, while capable of handling high volumes, require proper ventilation to prevent dust accumulation in the workspace. HeadPowder Engineering's solutions address these concerns by incorporating advanced filtration and dust suppression technologies, ensuring compliance with environmental regulations and workplace safety standards.
HeadPowder Engineering's Expertise in Ammonium Sulfate Conveying
Shandong HeadPowder Engineering Co., Ltd., based in China, is a trusted partner in designing and implementing pneumatic conveying systems for ammonium sulfate. The company combines technical expertise with practical experience to deliver customized solutions tailored to each client's unique needs. Their team of engineers conducts thorough assessments of material properties, operational requirements, and site conditions to develop optimal conveying systems. Whether a client requires a vacuum system for short-distance transport or a positive pressure system for long-distance handling, HeadPowder Engineering provides comprehensive support from system design to installation and maintenance.
The company's commitment to quality and innovation is reflected in its use of advanced materials and components. Their vacuum systems feature high-efficiency filters that capture fine particles, reducing environmental impact and ensuring product purity. The positive pressure systems are equipped with robust blowers and wear-resistant pipelines, extending equipment lifespan and minimizing downtime. HeadPowder Engineering's focus on customer satisfaction and long-term partnerships has made it a preferred choice for industries relying on ammonium sulfate transportation.
Conclusion
Pneumatic conveying technology offers efficient and effective solutions for transporting ammonium sulfate, with vacuum and positive pressure systems each providing distinct advantages based on specific application requirements. By understanding the technical differences and benefits of each method, industries can select the most suitable system to enhance material handling processes. HeadPowder Engineering's expertise in both vacuum and positive pressure conveying ensures clients receive tailored solutions that optimize performance, safety, and cost-effectiveness. For businesses seeking reliable and efficient ammonium sulfate transportation, HeadPowder Engineering provides the technical knowledge and practical solutions to meet their needs.




