Ammonium bicarbonate, a widely used chemical in the fertilizer industry, requires efficient and reliable transportation methods to ensure smooth production and distribution processes. The pneumatic conveying system designed for ammonium bicarbonate offers a solution that combines efficiency, safety, and cost-effectiveness. This article provides an overview of the system's structure and working principles, highlighting its key components and operational mechanisms.
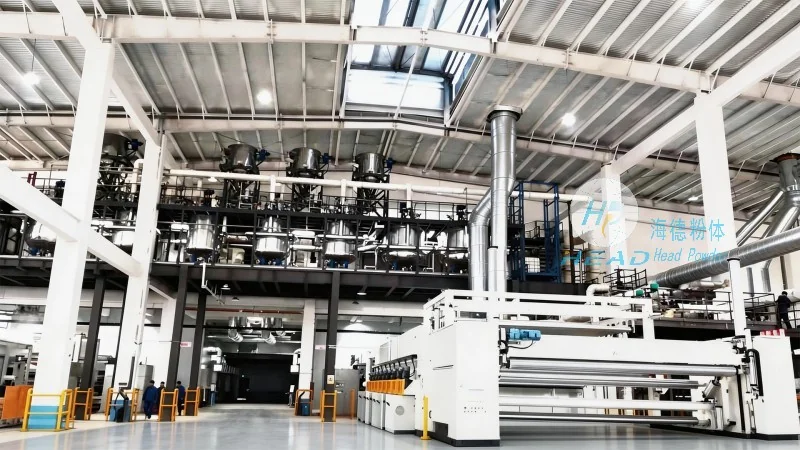
Key Components of the Ammonium Bicarbonate Pneumatic Conveying System
The pneumatic conveying system for ammonium bicarbonate typically consists of several essential components that work in tandem to achieve effective material transport. The primary components include the hopper, feeder, air compressor, conveying pipe, and dust collector. Each component plays a crucial role in the overall operation of the system.
The hopper serves as the storage container for the ammonium bicarbonate, ensuring a consistent feed supply. It is designed with a sloped bottom to facilitate the material's flow into the feeder. The feeder, often a rotary valve or a screw feeder, regulates the flow rate of the material into the conveying line, preventing overloading and maintaining system stability. The air compressor generates the necessary air pressure to create the airflow that propels the material through the system. The conveying pipe, usually made of stainless steel or other corrosion-resistant materials, is designed to withstand the chemical properties of ammonium bicarbonate and ensure minimal material degradation. The dust collector, equipped with filtration systems, captures any airborne particles, ensuring environmental compliance and worker safety.
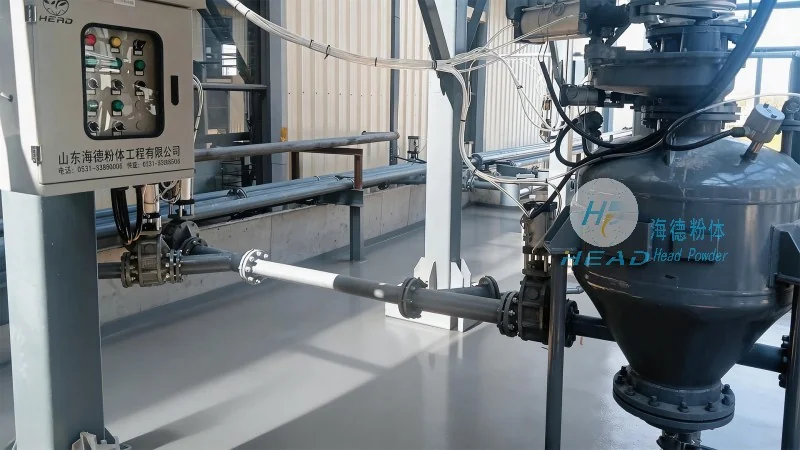
Working Principle of the Pneumatic Conveying System
The operation of the ammonium bicarbonate pneumatic conveying system is based on the principle of air movement and material suspension. When the air compressor starts, it generates a high-pressure airflow that enters the conveying pipe. The feeder then introduces the ammonium bicarbonate into the pipe, where the material particles are suspended by the airflow. The combination of air velocity and particle size allows the material to be transported through the system without the need for mechanical conveyors, which can be prone to material buildup and maintenance issues.
The system operates in a closed loop, with the air returning to the compressor after passing through the conveying line and dust collector. This closed-loop design minimizes air loss and energy consumption, making the system more efficient. The dust collector filters the air to remove any fine particles, ensuring that the air is clean before it is recirculated. The material is discharged at the receiving end of the system, typically into a storage silo or processing unit.
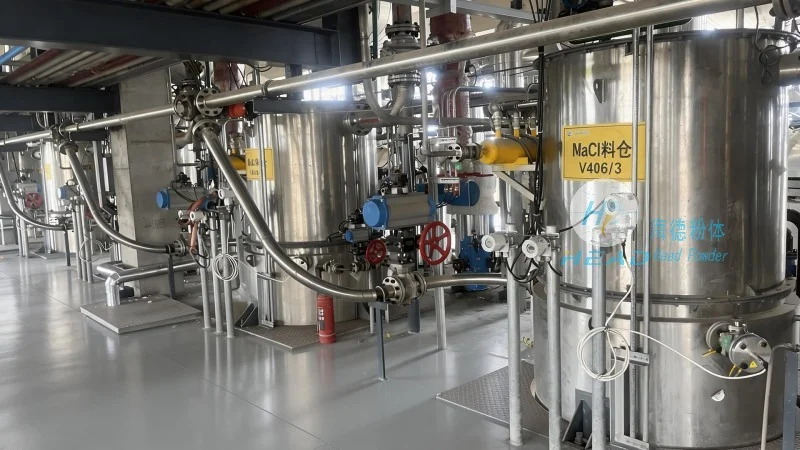
Advantages of the Ammonium Bicarbonate Pneumatic Conveying System
Compared to traditional mechanical conveying methods, the pneumatic conveying system for ammonium bicarbonate offers several advantages. Firstly, it eliminates the need for moving parts in the conveying line, reducing maintenance requirements and increasing system reliability. Secondly, the closed-loop design minimizes material loss and contamination, ensuring product quality. Thirdly, the system can handle a wide range of material flow rates, from low to high, making it adaptable to different production needs. Additionally, the system is less susceptible to material caking or bridging, which can occur in traditional hoppers and silos.
Applications and Industries
The ammonium bicarbonate pneumatic conveying system is widely used in the chemical and fertilizer industries, particularly in the production and handling of ammonium bicarbonate. It is also applicable in other industries where fine powders need to be transported, such as food processing and pharmaceuticals. The system's ability to handle sensitive materials without degradation makes it a preferred choice for industries that require high product quality and purity.
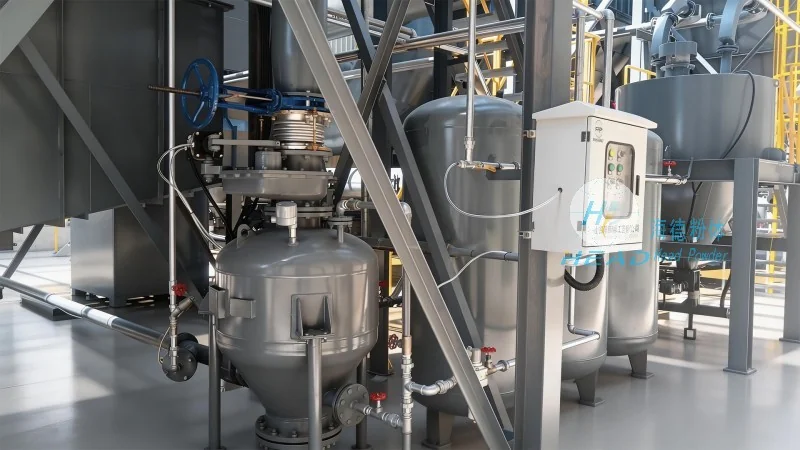
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., also known as headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the chemical processing industry. Headpowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients. The company's products are known for their durability, efficiency, and compliance with industry standards. Headpowder's commitment to customer satisfaction and technical excellence has earned it a reputation for reliability and professionalism in the market.
Contact Information
Headpowder is located in Shandong, China, and serves clients worldwide with its advanced pneumatic conveying solutions. The company's address is in Shandong, China, and it continues to be a leader in providing efficient and reliable transportation systems for ammonium bicarbonate and other fine materials.




