Bin pump pneumatic conveying equipment is a critical component in modern material handling systems, designed to efficiently transport bulk materials over long distances with minimal maintenance and operational complexity. This equipment is widely used in various industries, including chemical, food processing, and mining, where reliable and flexible material transport is essential. The bin pump, as the core component, operates by creating a vacuum or pressure differential to move materials through a pipeline network. Understanding its structure and working principles is vital for optimizing performance and ensuring longevity in industrial applications.
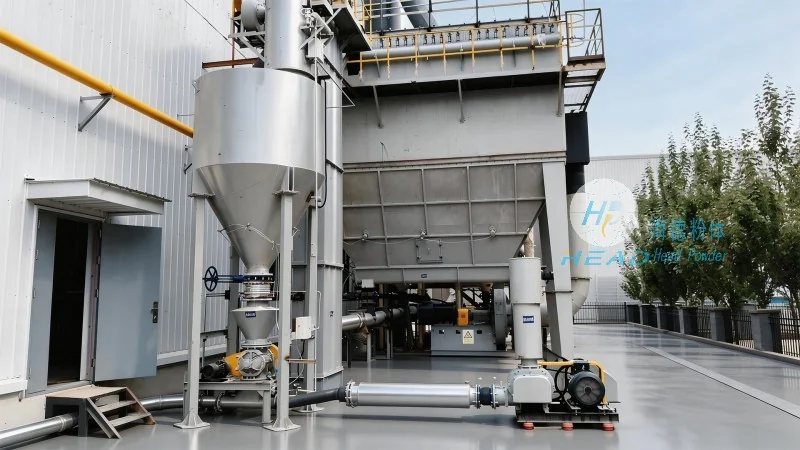
Key Structural Components of the Bin Pump System
The bin pump system comprises several key components that work in harmony to achieve efficient material transport. The primary components include the hopper, which serves as the material storage and feeding chamber; the pump body, which houses the impeller and drive mechanism; the control valve, responsible for regulating the flow and pressure; and the pipeline network, which connects the pump to the discharge point. Each component is engineered to withstand the specific demands of the material being conveyed, ensuring durability and consistent performance. The hopper is typically designed with a conical or rectangular shape to facilitate material flow and prevent blockages, while the pump body features a robust impeller that rotates to create the necessary air flow for material movement.
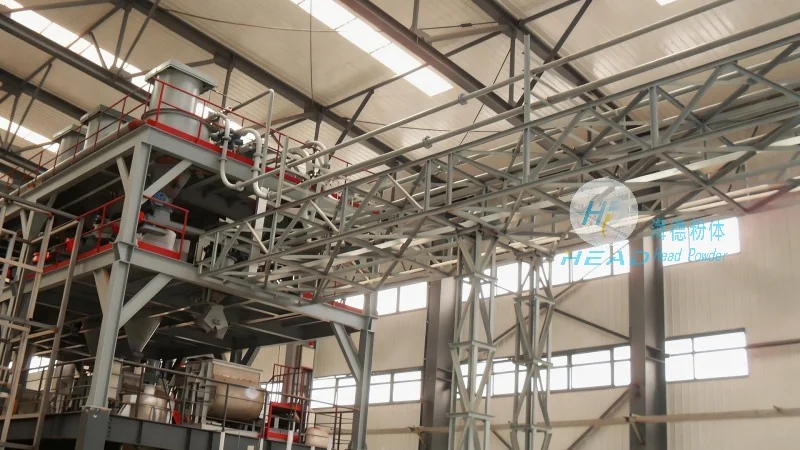
Principle of Operation: How the Bin Pump Transfers Materials
The operational principle of the bin pump is based on the creation of a pressure differential between the inlet and outlet of the system. When the pump is activated, the impeller rotates, drawing air and material from the hopper into the pump chamber. The impeller then forces this mixture through the discharge pipeline to the destination point. The process can be controlled to operate under vacuum or pressure, depending on the application requirements. This dual-mode operation allows for flexibility in handling different types of materials, from fine powders to bulk solids. The system's ability to handle a wide range of materials without the need for mechanical parts in contact with the material stream reduces wear and maintenance costs, making it a preferred choice for many industries.
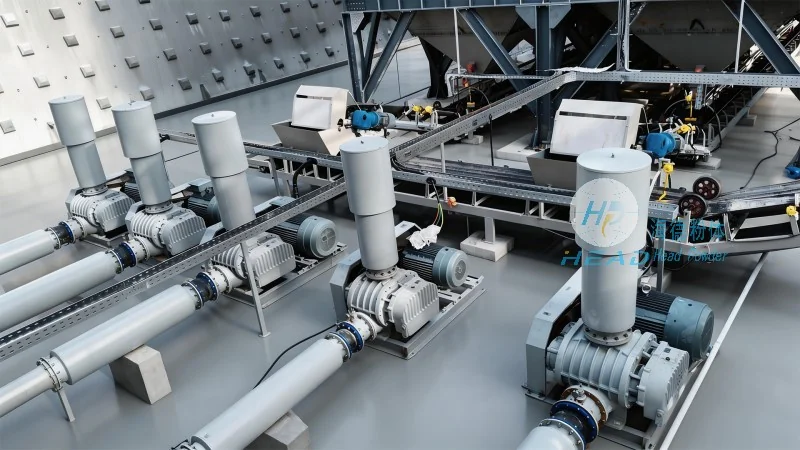
Advantages of Using Bin Pump Pneumatic Conveying Equipment
Bin pump systems offer several advantages over traditional mechanical conveying methods. Firstly, they provide a dust-free and hygienic conveying solution, which is crucial in industries like food and pharmaceuticals where contamination control is paramount. Secondly, the equipment is highly flexible, allowing for changes in material flow direction and distance without significant modifications. Thirdly, the system is energy-efficient, as it uses compressed air or vacuum to move materials, reducing operational costs compared to other methods. Additionally, the compact design of the bin pump makes it suitable for installation in confined spaces, optimizing factory layouts. These advantages make the bin pump an ideal solution for businesses seeking reliable, cost-effective, and versatile material handling solutions.
Applications in Diverse Industrial Sectors
Bin pump pneumatic conveying equipment is applied across a broad spectrum of industrial sectors, each benefiting from its unique capabilities. In the chemical industry, it is used to transport powders and granules safely, minimizing the risk of explosion or contamination. The food processing industry relies on it for conveying ingredients and finished products, ensuring compliance with hygiene standards. In mining and mineral processing, the equipment is used to transport ore and other bulk materials from processing plants to storage or processing facilities. The versatility of the bin pump allows it to adapt to various material characteristics, such as particle size, density, and moisture content, making it a universal solution for material handling challenges.
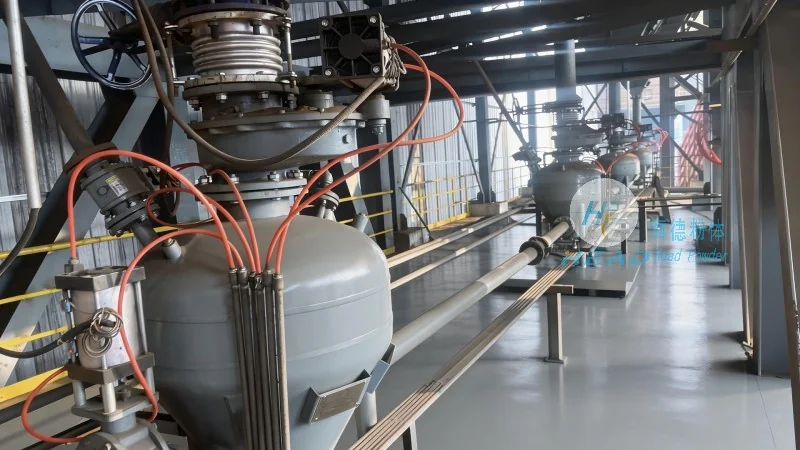
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of bin pump pneumatic conveying equipment. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the material handling industry. HeadPowder's products are designed and manufactured to meet international standards, ensuring reliability and performance in demanding industrial environments. The company's headquarters is located in Shandong, China, where it leverages advanced manufacturing technologies and a skilled workforce to produce high-quality equipment. HeadPowder is committed to providing customized solutions tailored to the specific needs of its clients, offering technical support and after-sales service to ensure customer satisfaction.




