HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced bulk bag unloading and pneumatic conveying systems. This equipment is widely used in various industries to efficiently handle bulk materials from large bags, ensuring smooth material transfer and processing. The following content provides a detailed overview of the equipment's structure, working principles, and key features.
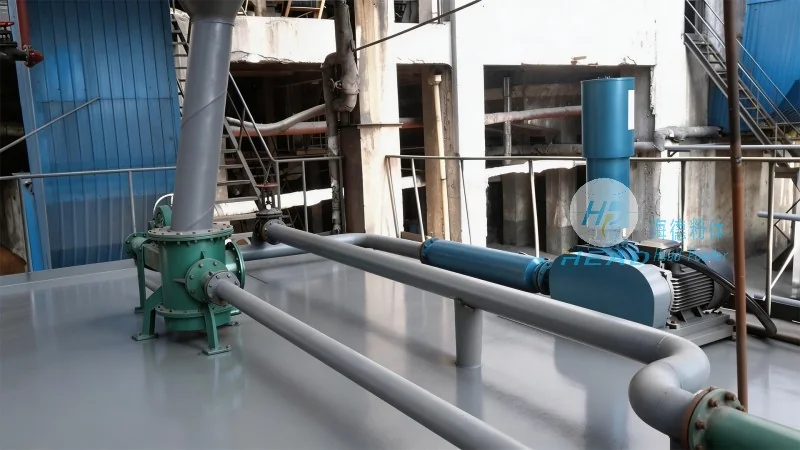
Overview of the Equipment
Bulk bag unloading and pneumatic conveying equipment is a critical component in material handling processes, particularly for industries dealing with dry bulk materials such as powders, granules, and other fine substances. The system typically consists of a bulk bag discharger, a pneumatic conveyor, and associated control mechanisms. It is engineered to safely and efficiently transfer material from the bulk bag into a storage silo, hopper, or processing unit, minimizing manual handling and reducing the risk of material contamination or loss.
Structural Components and Working Principle
The core structure of the bulk bag unloading and pneumatic conveying system includes several key components. The bulk bag discharger, often equipped with a bag support frame and a discharge valve, is designed to hold the bulk bag securely while allowing controlled material release. The pneumatic conveyor, which may use positive or negative pressure systems, transports the material from the discharger to the destination. The system operates by creating a pressure differential: in a positive pressure system, air is blown into the conveying line, pushing the material along; in a negative pressure system, air is drawn out, creating a vacuum that pulls the material. The control unit manages the flow rate, pressure, and timing to ensure optimal performance and material handling efficiency.
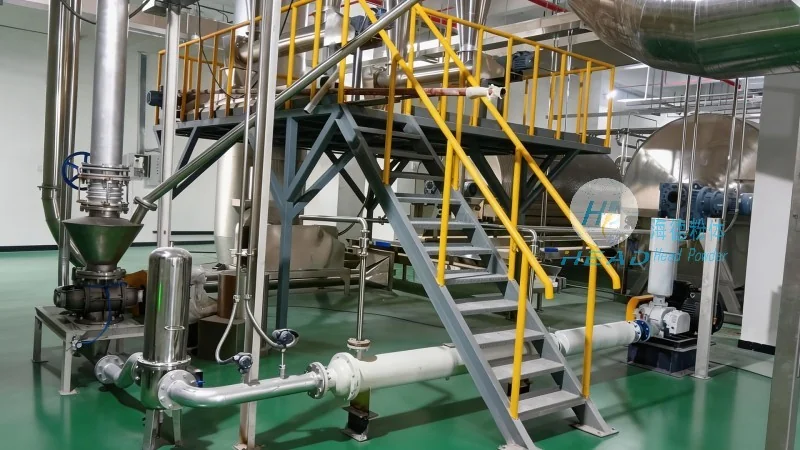
Technical Features and Advantages
HeadPowder's bulk bag unloading and pneumatic conveying equipment is characterized by several technical features that enhance its performance and reliability. The equipment is designed with robust materials to withstand the handling of various bulk materials, including abrasive or corrosive substances. Advanced control systems provide precise regulation of material flow, preventing overfilling or underfilling. The system also includes safety features such as overpressure relief valves and material flow sensors to ensure safe operation. Additionally, the equipment is modular and customizable, allowing it to be adapted to different bag sizes, material types, and processing requirements.
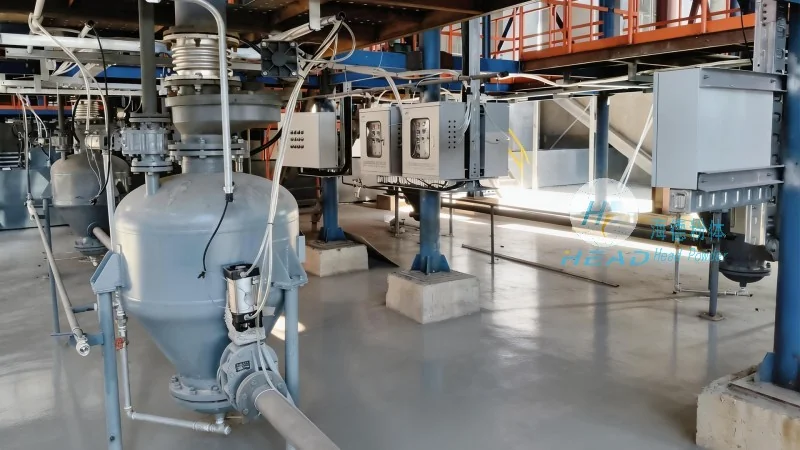
Application Scenarios
The bulk bag unloading and pneumatic conveying equipment is applicable in a wide range of industries, including chemical, food, pharmaceutical, and agricultural sectors. In the chemical industry, it is used to handle raw materials like powders and granules, ensuring a clean and efficient supply chain. In the food industry, the equipment is employed to process ingredients such as flour, sugar, and spices, maintaining hygiene standards. The pharmaceutical industry benefits from the equipment's ability to handle sensitive materials with minimal contamination, ensuring product quality and safety. In the agricultural sector, it is used to transfer bulk fertilizers, seeds, and other agricultural products, improving operational efficiency.
Performance and Efficiency Analysis
The performance of the bulk bag unloading and pneumatic conveying system is evaluated based on several key metrics, including material flow rate, system efficiency, and energy consumption. The system is designed to achieve high material throughput while minimizing energy usage. The positive pressure pneumatic conveyor, for example, can handle large volumes of material at a consistent flow rate, reducing the time required for material transfer. The negative pressure system, on the other hand, is ideal for handling fine powders that are prone to dusting, as it creates a sealed environment that prevents dust emissions. The equipment's efficiency is further enhanced by the use of advanced materials and engineering, which reduce wear and tear and extend the equipment's service life.




