In industrial production, efficient and clean material conveying systems are crucial for ensuring production quality and environmental safety. The dust-free bag opening material conveying system serves as a key link, enabling seamless transition from packaging to production lines while ensuring materials remain dust-free during processing. This article will detail the operation process and working principle of such a system, and introduce Shandong HeadPowder Engineering Co., Ltd. (company name: headpowder), located in Shandong, China, which is dedicated to providing professional material handling equipment solutions for industrial clients.
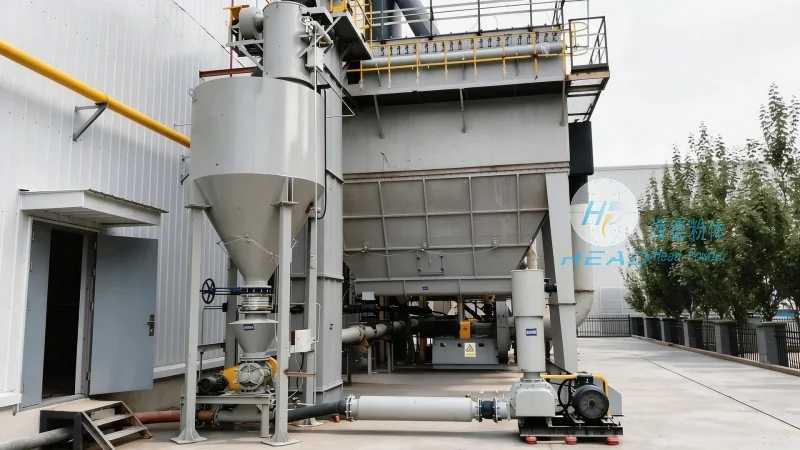
System Overview and Core Functions
The dust-free bag opening material conveying system is primarily used for handling powders or granular materials that require a clean environment, commonly found in industries like pharmaceuticals, food, and chemicals. Through an integrated design, the system achieves full automation from bagged material opening, weighing, to conveying to subsequent production processes. Core functions include automatic bag opening, material weighing, dust-free conveying, and dust collection and treatment. These functions collectively ensure materials are not contaminated during processing while improving production efficiency.
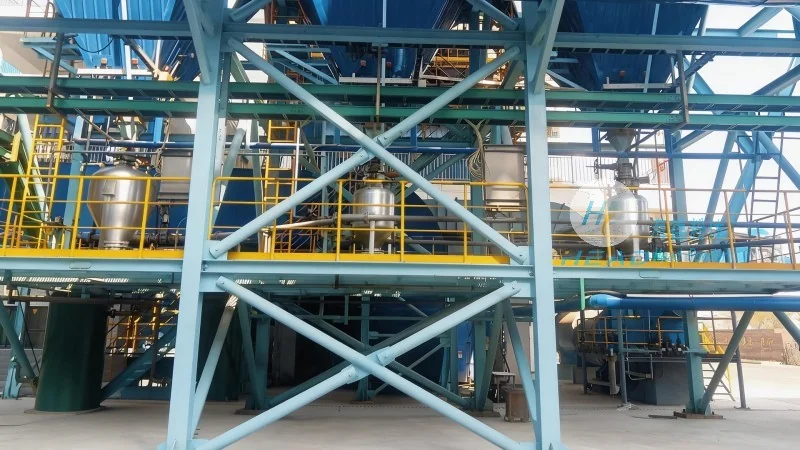
Detailed Operation Process
The operation process of the dust-free bag opening material conveying system typically involves the following steps: First, bagged materials are placed on the opening device, where the system uses mechanical or pneumatic mechanisms to open the packaging and release the internal material. Subsequently, the material enters a weighing module for precise weight measurement to control the amount of material sent for subsequent conveying. After weighing, the material is conveyed to a conveying device, such as a screw conveyor or pneumatic conveyor, to the designated storage or production area. Throughout the process, the system continuously monitors dust concentration and uses dust collection equipment (e.g., baghouse dust collectors or wet dust collectors) to capture generated dust, ensuring a clean working environment.
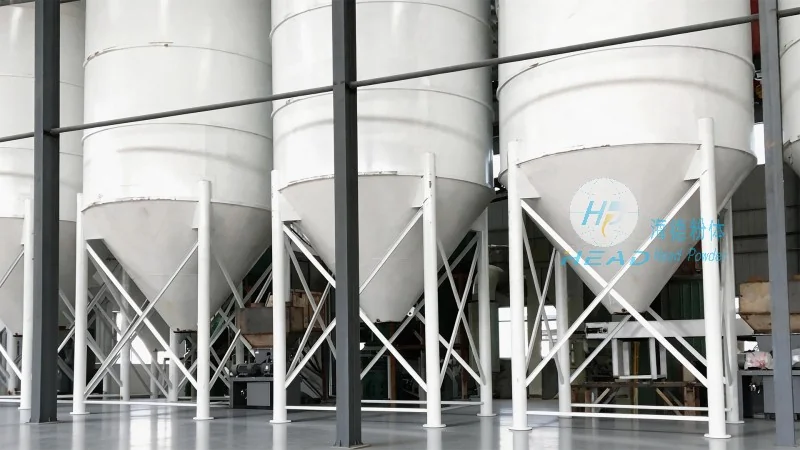
Working Principle Analysis
The core working principle of this system is based on automation control and clean technology. The bag opening device typically uses blade cutting or pneumatic blowing to safely open the packaging without damaging the material. The weighing module utilizes sensors and a weighing platform to measure material weight in real-time, with the control system adjusting the conveying amount accordingly. The conveying section selects an appropriate method based on material characteristics—for example, screw conveyors are suitable for powder conveying, while pneumatic conveying is used for light or dust-prone materials. The dust collection system employs filtration or absorption technology to capture dust particles in the air and prevent their spread. The entire system is centrally controlled by a PLC (Programmable Logic Controller) or industrial computer, enabling coordinated operation of all sections and ensuring stable system performance.
Technical Features and Advantages
The dust-free bag opening material conveying system offers several technical advantages, making it highly valued in industrial production. Firstly, the system uses a closed design to effectively prevent material dusting during conveying, maintaining a clean environment. Secondly, high automation reduces manual operations, enhancing production efficiency and safety. Additionally, the system can be customized based on material characteristics to meet the needs of different industries. As a professional manufacturer, Shandong HeadPowder Engineering Co., Ltd. provides comprehensive services from design, manufacturing to installation, ensuring the system meets specific customer requirements.
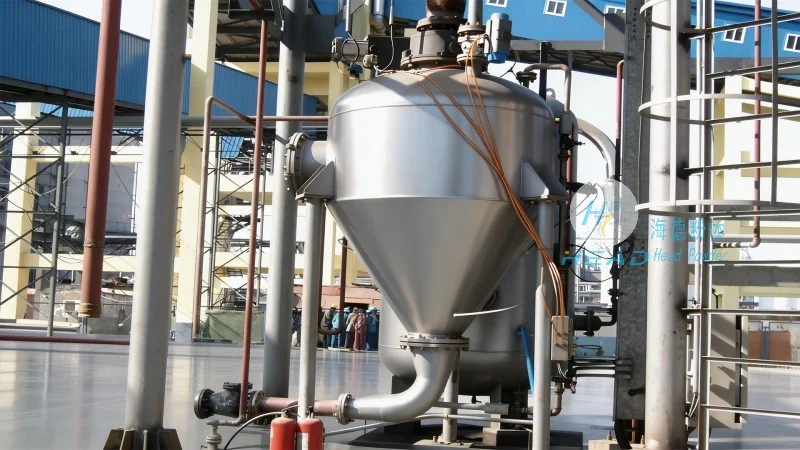
Application Scenarios and Industry Value
The dust-free bag opening material conveying system is widely applied in industries such as pharmaceuticals, food, chemicals, and electronics. In the pharmaceutical industry, the system is used to handle drug raw materials, ensuring compliance with GMP (Good Manufacturing Practice) standards for drug quality. In the food industry, it processes food additives or raw materials to ensure food hygiene and safety. In the chemical industry, it conveys chemical raw materials to prevent dust explosion accidents. By using this system, enterprises not only improve production efficiency but also reduce environmental pollution risks, enhancing overall production management levels.




