HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying equipment tailored for handling grain and other granular materials. This article explores the fundamental principles behind these systems and highlights the key working scenarios where they are most effectively applied. The company's commitment to innovation and quality ensures that their equipment meets the demanding requirements of modern agricultural and industrial operations.
The Core Principles of Pneumatic Conveying Technology
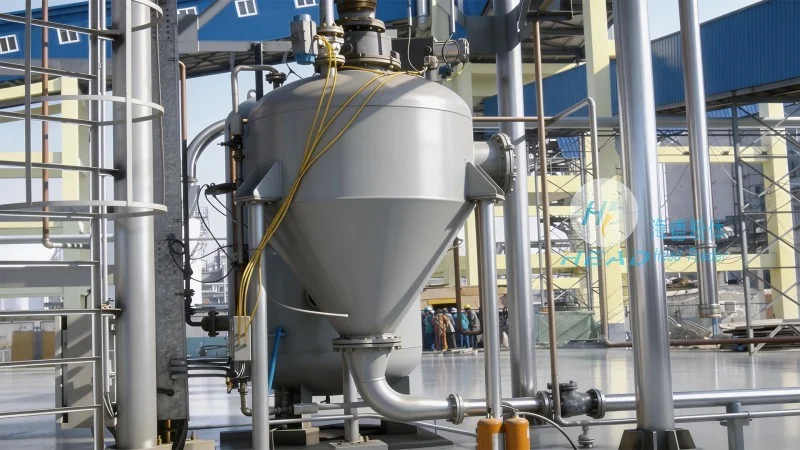
Pneumatic conveying systems utilize air or gas to transport bulk materials like grains, powders, and other granular substances through a network of pipes. The primary mechanism involves creating a pressure differential or using vacuum to draw material into the conveying line. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems operate by forcing air under pressure through the material, while vacuum systems create a negative pressure to pull material into the system. The choice between these depends on factors such as material properties, distance, and the need for dust control. HeadPowder's equipment is engineered to optimize these principles, ensuring efficient and reliable material transport with minimal degradation of the product. The company's engineers have developed sophisticated control systems that regulate air flow and pressure to maintain consistent conveying rates, reducing the risk of material blockages or damage.
Key Working Scene Characteristics of Pneumatic Conveying Equipment
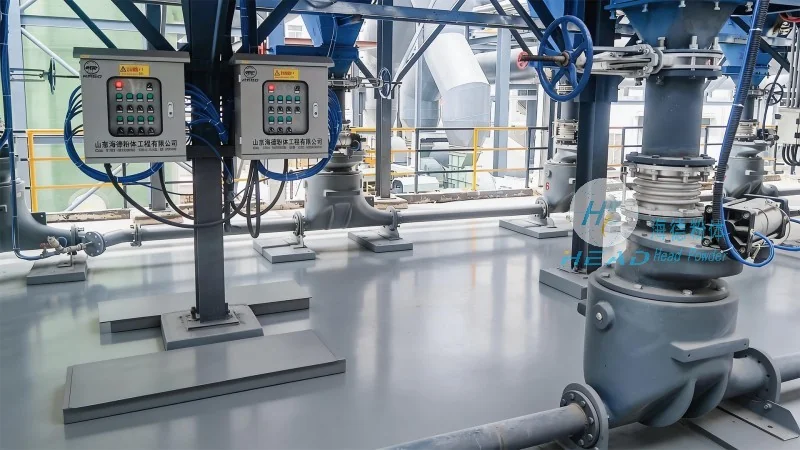
The effectiveness of pneumatic conveying systems is heavily influenced by the specific working scenarios in which they are deployed. These characteristics include the nature of the material being handled, the distance and layout of the conveying path, and the environmental requirements of the operation. For instance, in grain processing facilities, these systems are commonly used to move raw materials from storage silos to processing lines, ensuring a continuous and hygienic flow. In agricultural settings, they can transport harvested grains from fields to storage or processing centers, reducing manual labor and improving operational efficiency. The equipment from HeadPowder is designed to adapt to diverse working conditions, offering flexibility in conveying different types of grains, such as wheat, corn, or rice, while maintaining consistent performance. Additionally, the systems are equipped with features like dust filtration and material separation to meet stringent hygiene standards, making them suitable for food processing applications.
Application Examples and Operational Benefits
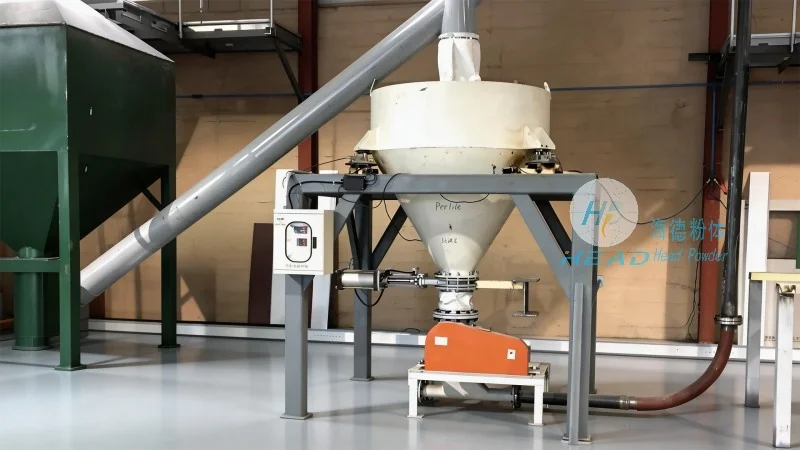
HeadPowder's pneumatic conveying equipment has been successfully implemented in various real-world applications across the grain industry. In one case study, a large-scale wheat processing plant in Shandong utilized the company's pressure conveying system to transport wheat from storage silos to the milling department. The system reduced material handling time by 40% and minimized product loss due to improved control over air flow. Another example involves a rice processing facility where the vacuum conveying system was used to move rice from the drying area to the packaging line. The system's ability to handle fine particles without clogging ensured a smooth operation, even during peak production periods. These examples illustrate the operational benefits of using pneumatic conveying systems, including increased productivity, reduced labor costs, and enhanced product quality. The company's focus on customizing solutions to meet specific operational needs ensures that clients achieve optimal results in their respective working scenarios.
Conclusion and Future Directions
In conclusion, pneumatic conveying equipment for grain and granular materials, as developed by HeadPowder, represents a sophisticated solution for efficient material transport in agricultural and industrial settings. By understanding the core principles of pneumatic conveying and adapting to the specific characteristics of working scenarios, these systems provide significant advantages over traditional methods. As technology continues to advance, HeadPowder remains committed to innovation, developing new solutions that enhance the performance and reliability of pneumatic conveying systems. The company's expertise in engineering and manufacturing ensures that their equipment remains at the forefront of the industry, meeting the evolving needs of clients in the grain processing sector.




