Intelligent pneumatic conveying systems represent a sophisticated solution for material handling, combining advanced technology with traditional pneumatic transport principles. Based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and implementing these systems, leveraging decades of experience to meet the diverse needs of modern industrial operations.
Understanding the Core Principles of Pneumatic Conveying
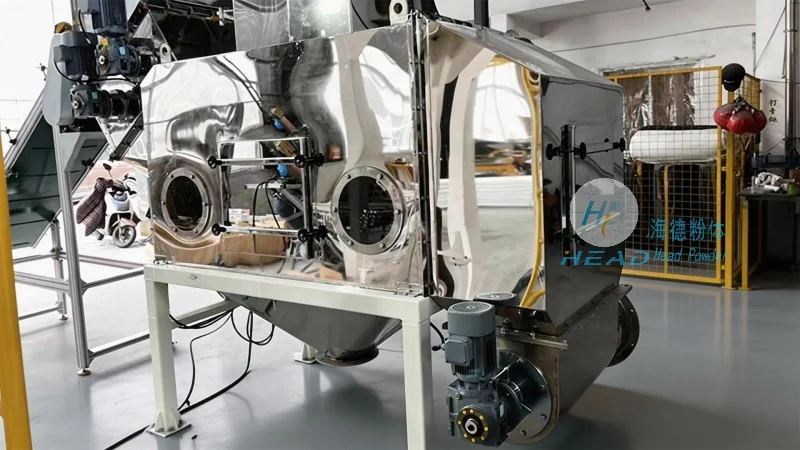
Pneumatic conveying operates by transporting bulk materials through a pipeline using air or gas as the medium. The fundamental principle involves creating a pressure differential between the inlet and outlet of the system. In positive pressure systems, air is forced into the material, propelling it through the pipeline, while negative pressure systems draw material into the system by creating a vacuum. This method offers several advantages, including the ability to handle a wide range of materials, from fine powders to granules, and the flexibility to transport materials over long distances without the need for mechanical components like belts or buckets.
Key Components and Their Roles
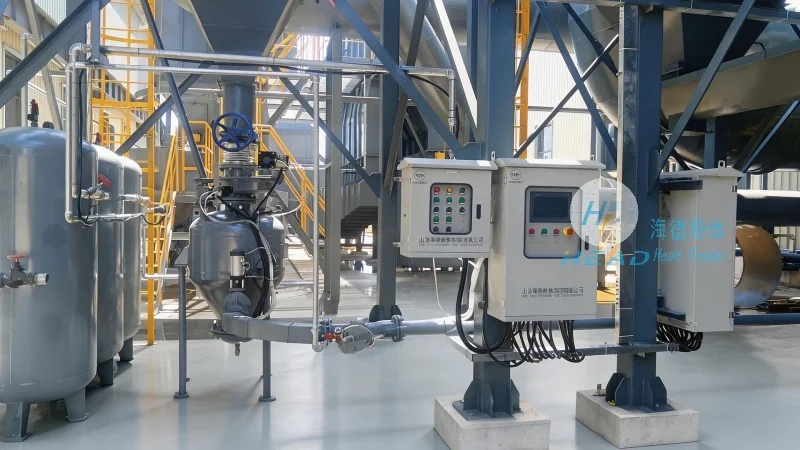
The effectiveness of a pneumatic conveying system relies on several critical components. The feed hopper is responsible for storing and feeding the material into the system, ensuring a consistent flow. The conveying line itself, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the pressure and temperature variations of the process. The air compressor or vacuum pump provides the necessary air or gas to drive the material, with control systems regulating pressure and flow rates. Additionally, filters and cyclones are essential for separating the material from the air, preventing contamination and ensuring compliance with environmental regulations. These components work in harmony to create a seamless material transport process.
Types of Pneumatic Conveying Systems
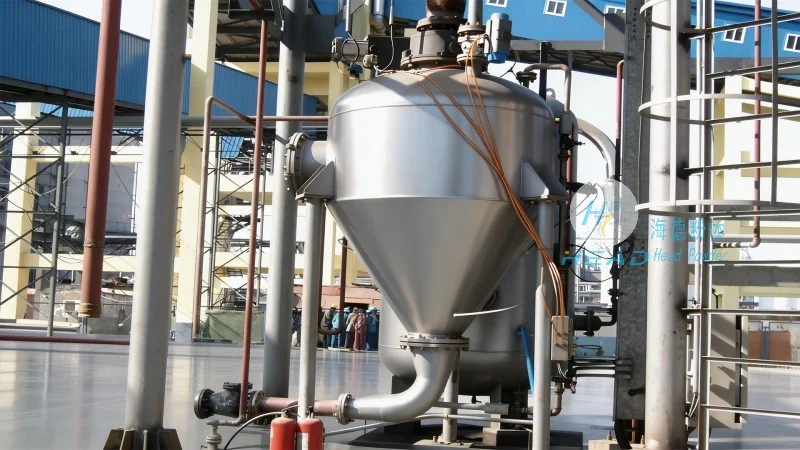
There are primarily two types of pneumatic conveying systems: positive pressure and negative pressure. Positive pressure systems are commonly used for short to medium distances and for materials that are prone to caking or agglomeration, as the high pressure helps maintain material flow. Negative pressure systems, on the other hand, are ideal for long-distance transport and for applications where dust control is a priority, as the system operates under a vacuum, drawing material into the pipeline without releasing air. Each type has its own advantages and is selected based on the specific requirements of the application, including material characteristics, distance, and environmental considerations.
Application Scenarios and Industry Use Cases
The versatility of intelligent pneumatic conveying makes it suitable for a wide array of industries. In the chemical industry, these systems are used to transport raw materials and finished products, ensuring safe and efficient handling of hazardous substances. The food and beverage sector benefits from the hygienic design of these systems, which prevents contamination and maintains product quality. In the pharmaceutical industry, the precision and cleanliness of pneumatic conveying are critical, as they help maintain sterile conditions and comply with stringent regulatory standards. Additionally, in the mining and minerals sector, these systems are used to transport ores and other bulk materials from processing plants to storage facilities. The ability to handle abrasive and corrosive materials makes them a preferred choice in these applications.
Advantages of Intelligent Pneumatic Conveying
Intelligent pneumatic conveying systems offer numerous benefits over traditional mechanical conveying methods. One of the key advantages is the reduction in labor costs, as the system operates with minimal human intervention. The automation features, including real-time monitoring and control, enhance operational efficiency and reduce downtime. Additionally, these systems are more energy-efficient compared to other transport methods, as they use compressed air or vacuum, which can be optimized for specific applications. The flexibility to handle various material types and sizes also makes them a versatile solution for changing production needs. Furthermore, the hygienic design of these systems is particularly valuable in industries where product purity is paramount, such as food and pharmaceuticals.
Customization and Integration with Existing Systems
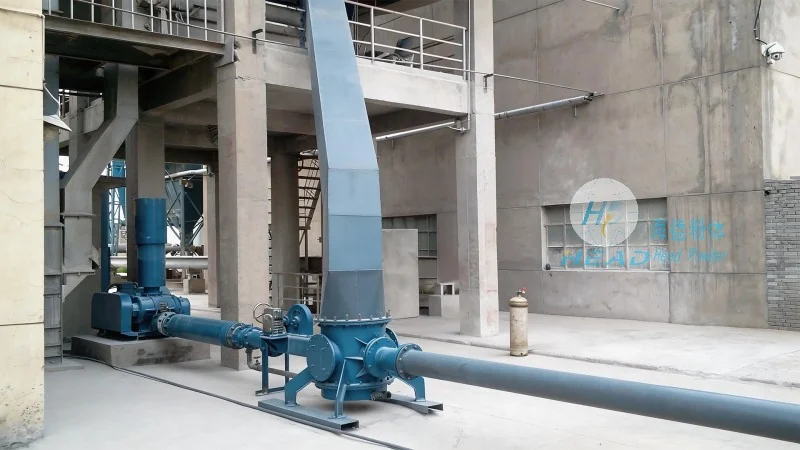
At Shandong HeadPowder Engineering Co., Ltd., we understand that each industrial operation has unique requirements. Our intelligent pneumatic conveying solutions are highly customizable, allowing us to integrate the system with existing infrastructure and processes. Whether it's retrofitting an existing plant or designing a new system from the ground up, our team works closely with clients to develop a solution that meets their specific needs. We also offer integration with other industrial systems, such as batching and weighing equipment, to create a comprehensive material handling solution. This approach ensures that the system not only transports materials efficiently but also enhances overall operational productivity.
Conclusion and Future Trends
Intelligent pneumatic conveying represents a significant advancement in material handling technology, offering a reliable and efficient solution for a wide range of industrial applications. At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing high-quality, customized systems that meet the evolving needs of our clients. By leveraging advanced technology and our expertise, we continue to innovate and improve the performance of our pneumatic conveying systems, ensuring they remain at the forefront of industrial material handling solutions.




