Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced material handling solutions tailored for sodium sulphate processing. The company, known as headpowder, is headquartered in Shandong, China, and has developed a range of equipment designed to efficiently transport and manage sodium sulphate, a key industrial chemical used in various applications such as glass manufacturing, detergents, and paper production. This article explores the working principle and key features of the material handling equipment used for sodium sulphate, highlighting how these systems enhance operational efficiency and safety in industrial settings.
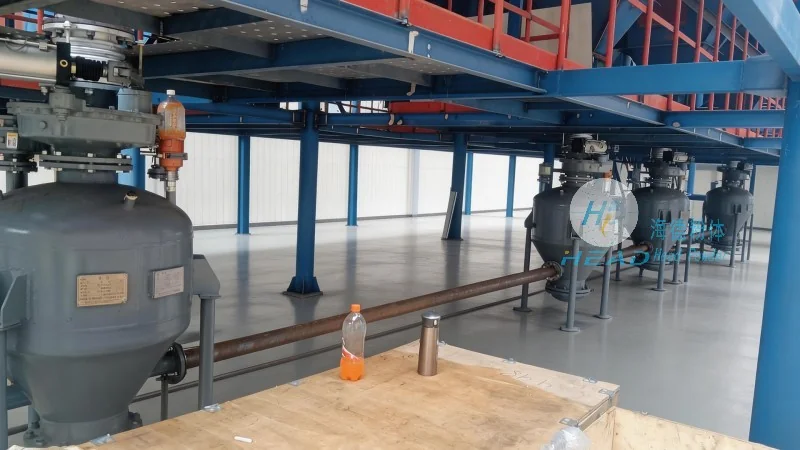
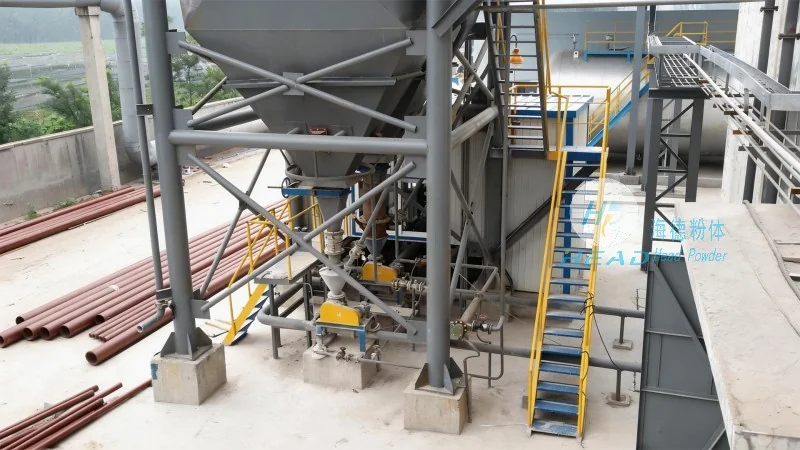
The Working Principle of Sodium Sulphate Material Handling Equipment
The core of sodium sulphate material handling equipment lies in its ability to transport bulk materials in a controlled and efficient manner. These systems typically consist of several components that work in tandem to move the material from one location to another. The primary mechanism involves the use of conveyor systems, which can be either belt conveyors or screw conveyors, depending on the specific application and material characteristics. For sodium sulphate, which is often in a powder or granular form, belt conveyors are commonly employed due to their effectiveness in handling loose materials without causing excessive dust or degradation. The working principle starts with the material being fed into the conveyor system, where it is then transported along a path defined by the conveyor's design. Motor-driven rollers or pulleys move the belt, carrying the sodium sulphate forward. In some cases, additional components like hoppers or feeders are integrated to regulate the flow of material, ensuring a consistent and controlled feed rate. This controlled movement minimizes material spillage and optimizes the transfer process, making it suitable for both short and long-distance transportation within industrial facilities. The system also includes safety features such as emergency stop buttons and overload protection to prevent equipment damage and ensure operator safety. By integrating these components, the equipment operates smoothly, providing reliable performance in handling sodium sulphate.
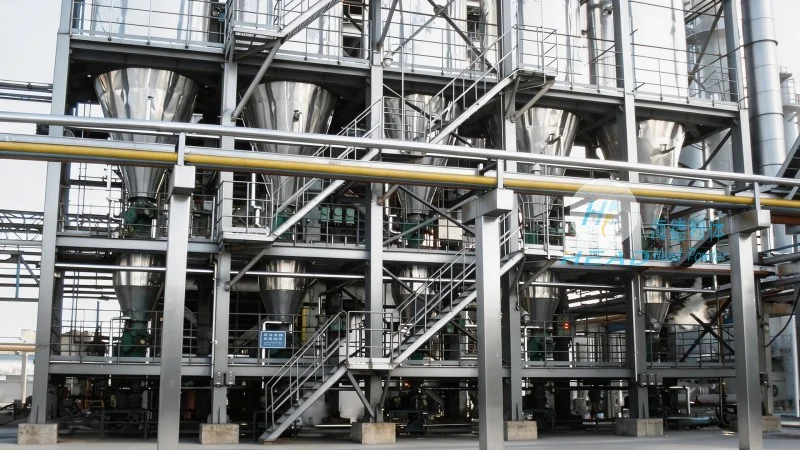
Key Features of Sodium Sulphate Material Handling Equipment
HeadPowder's material handling equipment for sodium sulphate is designed with several key features that enhance its functionality and adaptability. One of the primary features is its durability, as the equipment is constructed from materials resistant to corrosion and wear, which is crucial when handling sodium sulphate, a chemical that can be abrasive and cause degradation over time. The equipment is also equipped with adjustable speed controls, allowing operators to modify the conveyor speed based on the material's flow characteristics and the specific requirements of the process. This flexibility ensures that the system can handle varying loads and maintain optimal performance under different conditions. Another important feature is the integration of dust control mechanisms, such as enclosed conveyor systems and dust collection units, which help to minimize airborne particles and maintain a clean working environment. This is particularly important in industrial settings where dust can pose health risks and affect product quality. The equipment also includes easy maintenance features, such as accessible components and quick-release mechanisms, which reduce downtime and lower maintenance costs. Additionally, the systems are designed for easy integration with other industrial equipment, such as storage silos and processing units, allowing for seamless operation within the overall production line. These features collectively contribute to the efficiency and reliability of the material handling process, making the equipment a valuable asset for sodium sulphate processing facilities.
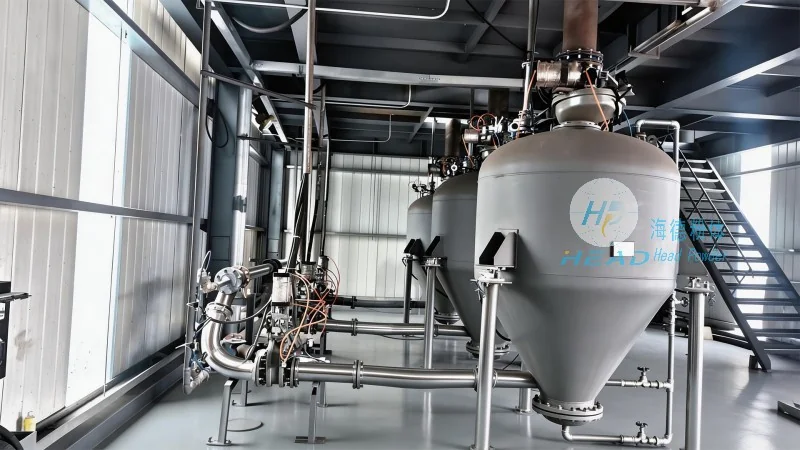
Operational Benefits and Applications
The use of specialized material handling equipment for sodium sulphate offers several operational benefits that improve overall productivity and safety. One of the main advantages is the reduction in manual labor, as the equipment automates the material transport process, minimizing the need for workers to handle heavy or dusty materials. This not only improves safety but also increases the speed and consistency of material transfer. Another benefit is the improved material flow control, which helps to prevent bottlenecks and ensure a steady supply of sodium sulphate to downstream processes. The equipment's ability to handle varying material conditions, such as different particle sizes and moisture levels, makes it versatile and suitable for a wide range of applications. For example, in glass manufacturing, the equipment efficiently transports sodium sulphate to the furnace, while in detergent production, it ensures a consistent feed of the chemical to the mixing units. The durability and low maintenance requirements of the equipment also contribute to long-term cost savings, as the systems require less frequent repairs and replacements. Overall, the material handling equipment from headpowder provides a reliable and efficient solution for managing sodium sulphate, supporting the smooth operation of industrial processes and enhancing the overall productivity of the facility.




