Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in powder handling technology, specializes in designing, manufacturing, and integrating advanced dust-free automatic powder pneumatic conveying systems. The company focuses on precision, efficiency, and safety, establishing itself as a trusted partner for industries requiring reliable powder transport solutions. This article explores the fundamental principles behind these systems and highlights their key application scenarios, providing insights into how they enhance operational performance and ensure compliance with industry standards.
Understanding the Core Principles of Dust-Free Pneumatic Conveying Systems
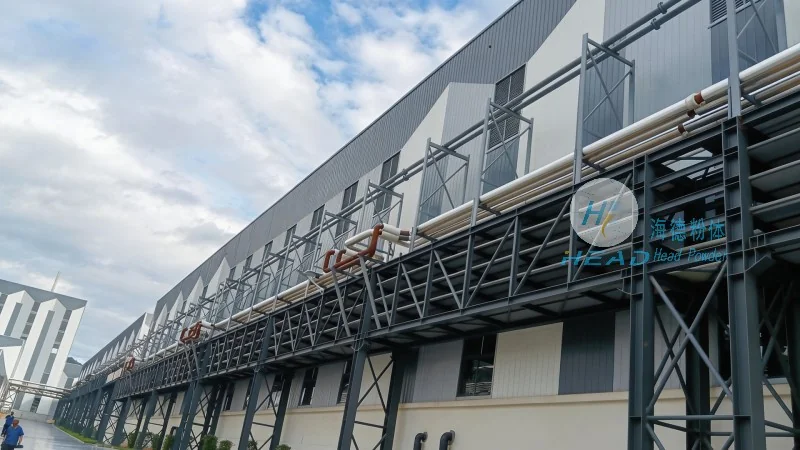
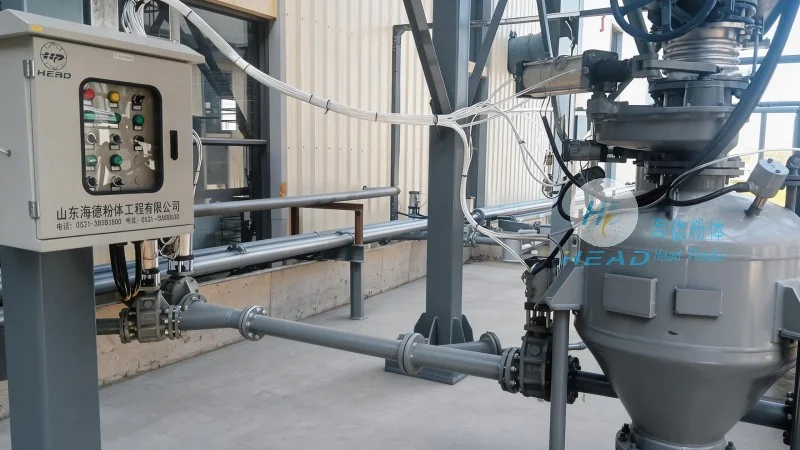
The dust-free automatic powder pneumatic conveying system operates on the principle of using compressed air to transport dry powders or granules through a sealed pipeline. Unlike traditional bulk material handling methods, this system eliminates manual handling and reduces dust contamination risks, making it ideal for applications where product purity and environmental safety are critical. The system typically includes a material feeder, conveying line, separation unit, and dust collection system. The material feeder, often with a rotary valve or screw feeder, ensures consistent powder flow into the conveying line. Compressed air from an air compressor creates a pressure differential to propel powder particles forward. The conveying line, made of stainless steel or PTFE-coated tubing, maintains airtightness to prevent dust leakage. At the receiving end, a cyclone or bag filter separates powder from the air stream, ensuring accurate deposition and filtered air release. The dust collection system captures residual particles, maintaining a clean working environment. The entire system is automated, with sensors and control panels monitoring flow rate, pressure, and temperature to optimize performance and prevent issues. This automation enhances efficiency, reduces labor costs, and minimizes human error.
Key Application Scenarios and Benefits in Industrial Settings
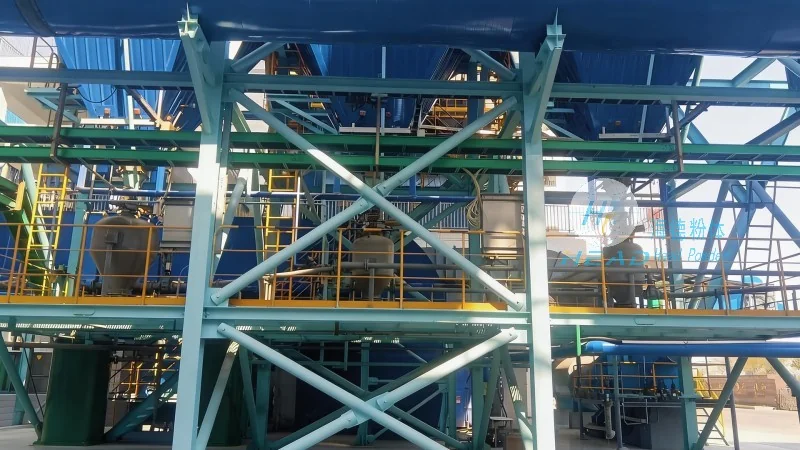
The dust-free automatic powder pneumatic conveying system is widely used across industries such as pharmaceuticals, food processing, chemical manufacturing, and cosmetics. In pharmaceuticals, it is crucial for transporting active pharmaceutical ingredients (APIs) and excipients with strict purity requirements, as the sealed environment prevents contamination and meets regulatory standards. In the food industry, the system handles ingredients like flour, sugar, and spices, maintaining food safety and avoiding cross-contamination. The chemical industry benefits from handling hazardous powders (e.g., chemicals, pigments) with minimal worker exposure risk. The cosmetics industry relies on it to transport raw materials like pigments and powders, ensuring consistent quality and color uniformity. Beyond these sectors, it is used in ceramics, plastics, and other materials where precision and cleanliness are essential. Primary benefits include improved product quality, reduced downtime from maintenance, enhanced operator safety, and increased operational efficiency. By eliminating manual handling and dust exposure, the system minimizes contamination and workplace accidents. The automated nature allows consistent flow rates and lower labor costs, making it cost-effective for large-scale operations. The system can handle a wide range of powders (fine to coarse granules), expanding applicability across industries. Its modular design enables easy integration with existing production lines, minimizing modifications and ensuring smooth transitions to automated powder handling.
Technical Advantages and Customization Options
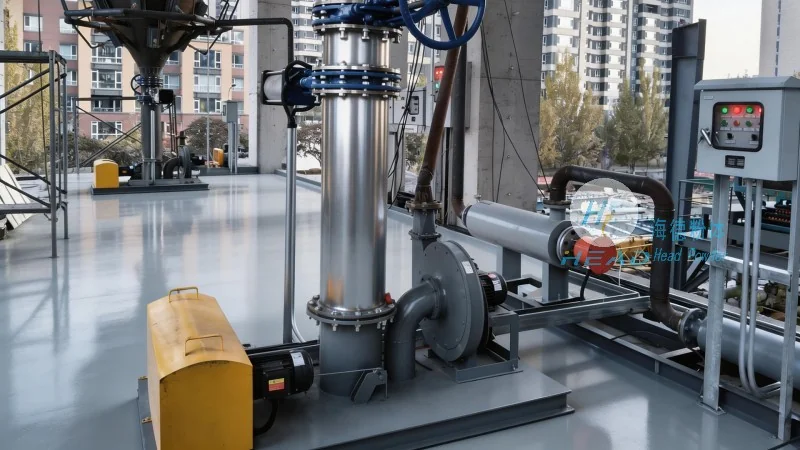
Shandong HeadPowder Engineering Co., Ltd. offers technical advantages and customization options tailored to industry needs. Systems use high-quality materials (stainless steel, PTFE) for corrosion and wear resistance, ensuring long-term durability. Advanced control systems allow precise monitoring and adjustment of air pressure/flow rate for optimal performance with different powders. The company provides customized solutions, including varied conveying line lengths, material feeder types, and separation units. For high-purity applications, HEPA filters can be added to ensure air is particle-free, further enhancing product purity. The modular design allows easy expansion or modification as production scales. The company’s expertise in powder handling enables technical support and maintenance services, ensuring peak efficiency. These technical advantages and customization options make the system a versatile solution for diverse industrial applications. By leveraging advanced technology and deep powder handling knowledge, Shandong HeadPowder Engineering Co., Ltd. continues to deliver innovative solutions that enhance operational performance and ensure compliance with industry standards.




