HeadPowder, a leading provider of industrial powder handling solutions, specializes in vacuum dilute phase powder conveying systems. These systems are engineered to efficiently transport bulk powders over long distances with minimal pressure differentials, making them ideal for various industrial applications.
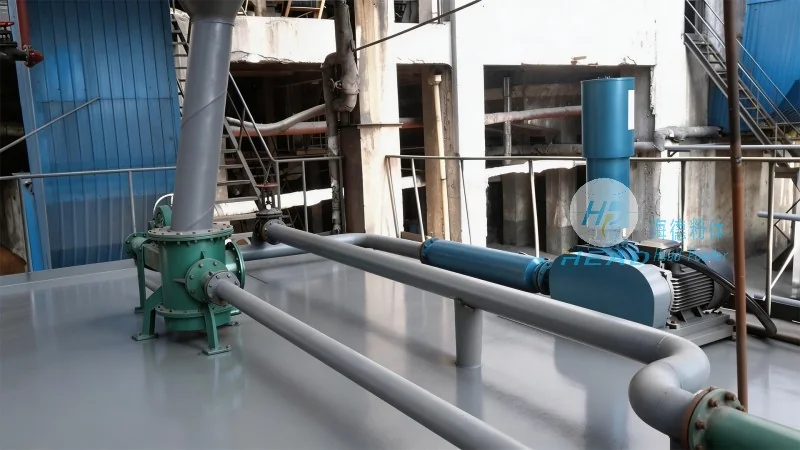
Overview of Vacuum Dilute Phase Powder Conveying Systems
Vacuum dilute phase powder conveying systems are a type of pneumatic conveying technology that operates under negative pressure. The system draws the powder from the source, typically a hopper or silo, into a pipeline using a vacuum pump. The powder is then transported through the pipeline to the destination point, such as a storage tank or processing unit. This method is particularly effective for handling fine or abrasive powders, as it minimizes product degradation and equipment wear compared to positive pressure systems.
Working Principle of the System
The core of the vacuum dilute phase powder conveying system is the vacuum pump, which creates a pressure differential between the source and the destination. The process begins when the vacuum pump is activated, drawing air and powder particles from the source into the conveying line. The powder is suspended in the air stream as a dilute phase, meaning the powder concentration is low (typically 1-5% by volume). The air flow carries the powder particles through the pipeline, and the system uses cyclone separators or filters at the destination to separate the powder from the air. The cleaned air is then returned to the system or released to the atmosphere, completing the cycle.
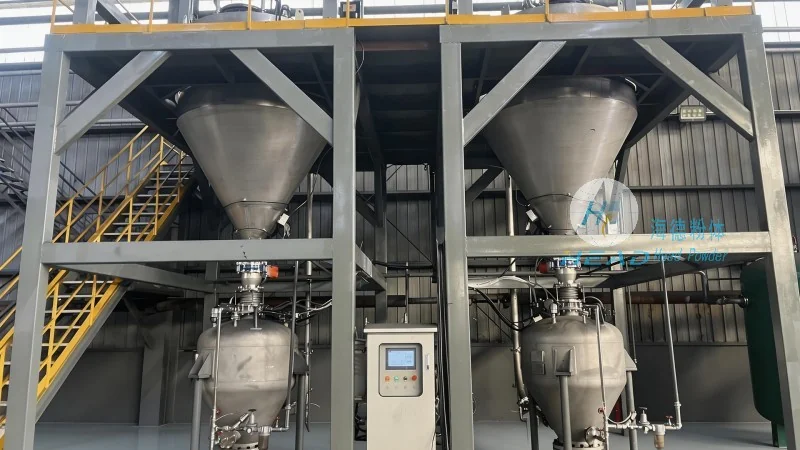
Key Features and Advantages
HeadPowder's vacuum dilute phase powder conveying systems offer several distinct advantages that make them a preferred choice for many industries. One of the primary features is the ability to operate under negative pressure, which reduces the risk of dust emissions and improves safety in the workplace. The low pressure differentials required mean that the system is less energy-intensive compared to positive pressure systems, resulting in lower operational costs. Additionally, the dilute phase operation minimizes the risk of product agglomeration and blockages, ensuring consistent and reliable performance. The systems are also designed for easy integration with existing industrial processes, allowing for seamless incorporation into production lines.
Applications and Industries
Vacuum dilute phase powder conveying systems are widely used across various industries, including food processing, pharmaceuticals, chemicals, and minerals. In the food industry, these systems are used to transport ingredients like flour, sugar, and spices, ensuring hygienic and efficient handling. In pharmaceutical applications, the systems are critical for conveying active pharmaceutical ingredients (APIs) and excipients, as they maintain product purity and prevent contamination. The chemical industry utilizes these systems for handling powders like catalysts, pigments, and fertilizers, while the minerals sector uses them for transporting ores and other bulk materials. The versatility of the system makes it suitable for a wide range of applications where reliable and safe powder transport is essential.
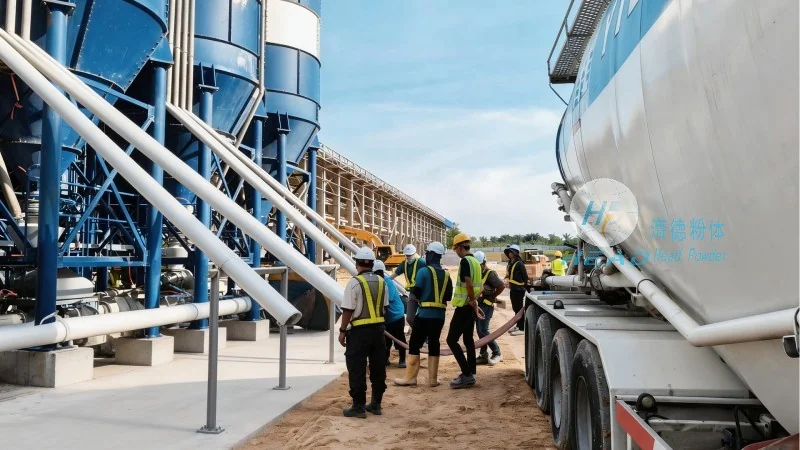
Installation and Maintenance Considerations
Proper installation and regular maintenance are crucial for the optimal performance and longevity of vacuum dilute phase powder conveying systems. The system should be installed with appropriate ductwork and fittings to minimize pressure losses and ensure smooth powder flow. HeadPowder recommends regular cleaning of the cyclone separators and filters to prevent clogging and maintain efficiency. Additionally, the vacuum pump and other components should be inspected periodically for wear and tear, with replacement of worn parts as needed. Proper maintenance not only ensures the system operates at peak efficiency but also extends its service life, reducing long-term operational costs.
Conclusion
HeadPowder's vacuum dilute phase powder conveying systems represent a reliable and efficient solution for bulk powder transport. By leveraging negative pressure and dilute phase operation, these systems offer significant advantages in terms of energy efficiency, safety, and product integrity. With their ability to handle a wide range of powders and integrate seamlessly into industrial processes, they are an essential component for many industries. As a leading manufacturer based in Shandong, China, HeadPowder continues to innovate and provide high-quality solutions that meet the evolving needs of the powder handling industry.




