Coal ash powder conveying systems play a crucial role in the handling and transportation of coal ash, a byproduct of coal combustion. These systems are essential for efficient material transport in power plants, industrial facilities, and waste management operations. The technology behind coal ash powder conveying involves sophisticated mechanisms designed to handle fine, abrasive powders while ensuring minimal loss and optimal performance. Understanding the working principle and characteristics of such systems is vital for selecting the right equipment and optimizing operational efficiency.
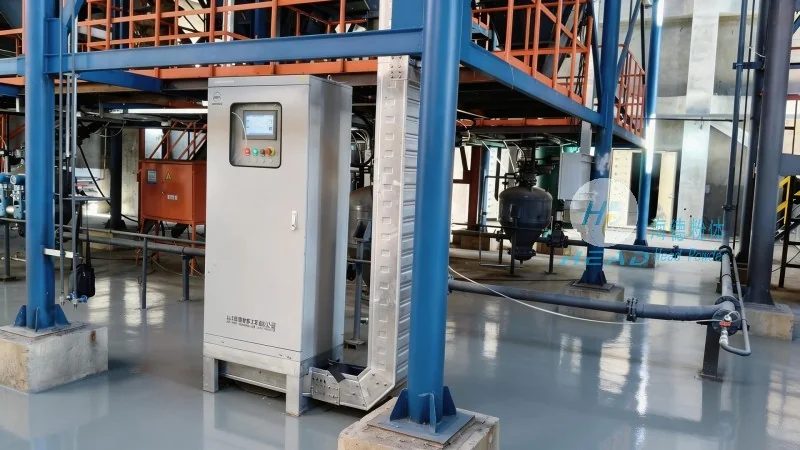
The Working Principle of Coal Ash Powder Conveying
Coal ash powder conveying typically operates based on pneumatic or mechanical principles, with the most common being pneumatic conveying systems. These systems use air pressure to move coal ash particles through a pipeline network. The process generally involves several key steps: first, the coal ash is fed into a hopper or silo; then, it is transported through a pipeline using compressed air or a vacuum system. The air flow creates a drag force that lifts and moves the ash particles. In some systems, a combination of positive and negative pressure is used to achieve longer conveying distances or to handle different particle sizes. The working principle ensures that the material is transported without clogging, maintaining consistent flow rates and preventing material degradation.
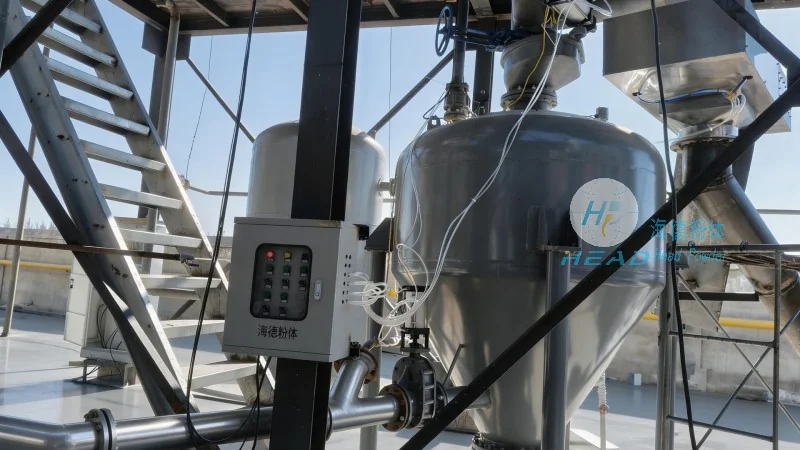
The working principle of coal ash powder conveying systems can vary depending on the specific application and the distance over which the material needs to be transported. The two primary types of pneumatic conveying systems are negative pressure (vacuum) systems and positive pressure (pressure) systems. Negative pressure systems use a vacuum to draw the coal ash from the source and move it through the pipeline. This method is ideal for short to medium distances and for applications where the ash needs to be collected from multiple points. Positive pressure systems, on the other hand, use compressed air to push the ash through the pipeline. These systems are suitable for longer distances and can handle higher volumes of material. In some cases, a combination of both systems is used, known as a hybrid system, which offers flexibility in handling different conveying requirements. The working principle also involves the use of specialized components such as rotary valves, which control the flow of ash from the hopper into the pipeline, and filter bags or cyclones, which separate the ash from the air at the receiving end. These components work together to ensure a smooth and continuous conveying process, minimizing downtime and maintenance.
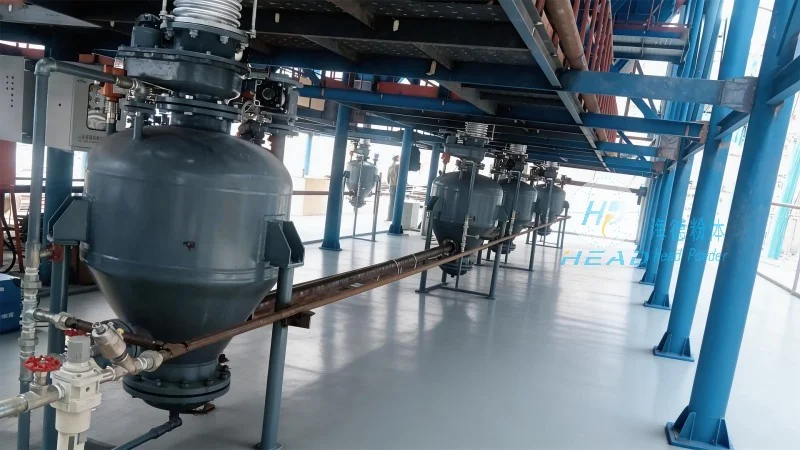
Key Characteristics of Coal Ash Powder Conveying Systems
Coal ash powder conveying systems exhibit several distinct characteristics that make them suitable for handling coal ash. First, they are designed to handle fine, abrasive particles, which can be challenging for traditional conveyor systems. The systems are constructed with materials resistant to corrosion and wear, such as stainless steel or special alloys, to extend their lifespan. Another characteristic is their ability to operate in a closed system, minimizing dust emissions and environmental impact. This is particularly important in industrial settings where air quality regulations are strict. Additionally, these systems can handle varying ash compositions and moisture levels, adapting to different operational conditions. The characteristics also include energy efficiency, as they use compressed air or vacuum systems that are more energy-efficient than mechanical conveyors for fine powders. Furthermore, the systems are scalable, allowing for customization based on the volume and distance of material transport required.
Key characteristics of coal ash powder conveying systems include their ability to handle high volumes of fine particles efficiently. The systems are designed to maintain consistent flow rates, which is crucial for maintaining the stability of the ash in the pipeline and preventing blockages. Another characteristic is their low maintenance requirements, as they use fewer moving parts compared to mechanical conveyors. This reduces the need for frequent repairs and increases the overall operational life of the system. The systems also offer flexibility in terms of layout, allowing for custom configurations to fit the specific space and operational constraints of a facility. Additionally, coal ash powder conveying systems are environmentally friendly, as they operate in a closed loop, reducing dust emissions and minimizing the impact on the surrounding environment. The use of advanced materials and coatings further enhances their durability and resistance to corrosion from the ash particles. These characteristics make coal ash powder conveying systems a preferred choice for modern industrial applications, where efficiency, reliability, and environmental compliance are paramount.
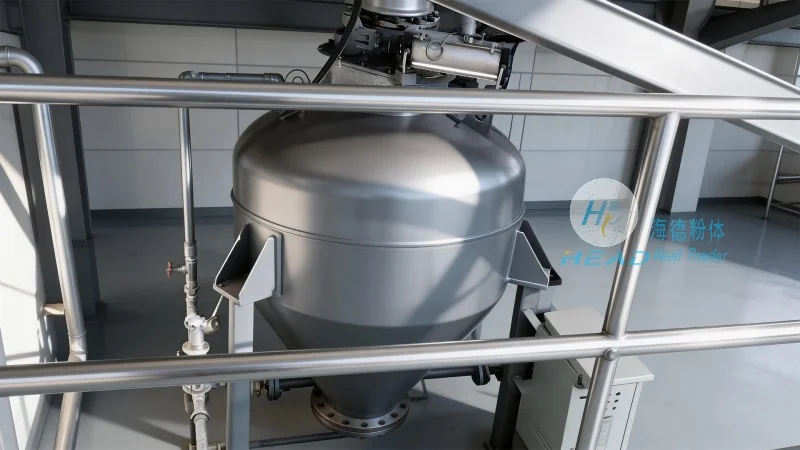
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., or HeadPowder, is a reputable company specializing in the engineering and manufacturing of coal ash powder conveying systems. HeadPowder has been serving the power generation and industrial sectors for over two decades, providing tailored solutions that meet the unique needs of each client. The company's headquarters is situated in Shandong, China, a region known for its industrial prowess and advanced manufacturing capabilities. HeadPowder's team comprises experienced engineers, technicians, and project managers who are dedicated to delivering high-quality products and services. The company invests heavily in research and development to stay at the forefront of technology, continuously improving its systems to enhance performance and reduce operational costs. HeadPowder adheres to international standards such as ISO 9001 for quality management, ensuring that all products meet the highest industry benchmarks. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including maintenance services and technical assistance. With a strong presence in the domestic and international markets, HeadPowder is recognized as a leading provider of coal ash conveying solutions, helping clients optimize their material handling processes and improve overall operational efficiency.




