Efficient and reliable bulk material handling is a critical factor in the sugar industry, where maintaining product quality and operational efficiency are paramount. Pneumatic conveying systems have emerged as a preferred solution for transporting white sugar and other granular materials, offering advantages such as minimal product degradation, reduced contamination risk, and enhanced safety compared to traditional methods like belt conveyors or bucket elevators.
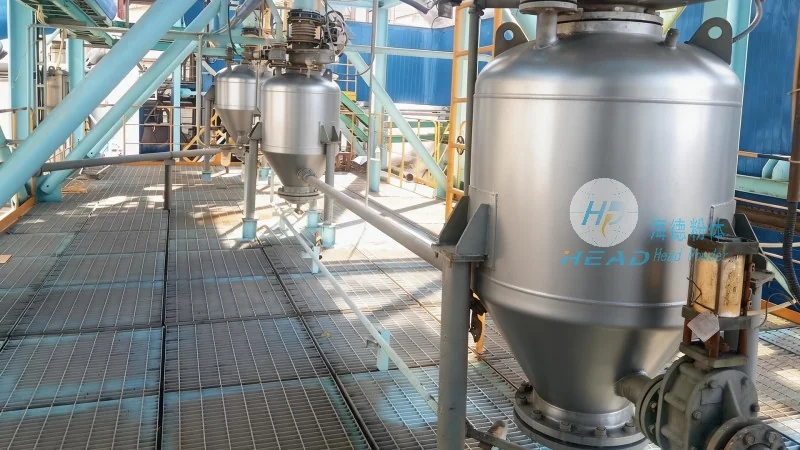
Advantages of Pneumatic Conveying for White Sugar Transport
When it comes to handling white sugar, pneumatic conveying systems provide several key benefits that make them ideal for industrial applications. One of the most significant advantages is the ability to maintain product integrity. The enclosed system prevents exposure to air, moisture, and contaminants, which can affect the quality and sweetness of the sugar. This is particularly important for white sugar, as it is highly sensitive to environmental factors that could lead to caking or spoilage. Additionally, pneumatic conveyors offer a dust-free operation, which is crucial for maintaining a clean and safe working environment in sugar processing facilities. The absence of moving parts in contact with the product reduces the risk of mechanical damage, ensuring that the sugar remains in its optimal condition throughout the conveying process.
How Pneumatic Conveying Works in Sugar Handling
Pneumatic conveying systems operate by using air pressure to move bulk materials through a network of pipes. In the case of white sugar, the system typically involves a hopper or storage silo where the sugar is loaded. A fan or blower creates a low-pressure zone, drawing the sugar into the conveying line. The sugar is then transported through the pipes to the destination, such as a processing unit or packaging area. The system can be designed as either a positive pressure or negative pressure system, depending on the specific requirements of the sugar handling operation. Positive pressure systems push the material through the pipes using compressed air, while negative pressure systems create a vacuum to pull the material. For white sugar, a positive pressure system is often preferred as it provides better control over the flow rate and reduces the risk of product degradation.
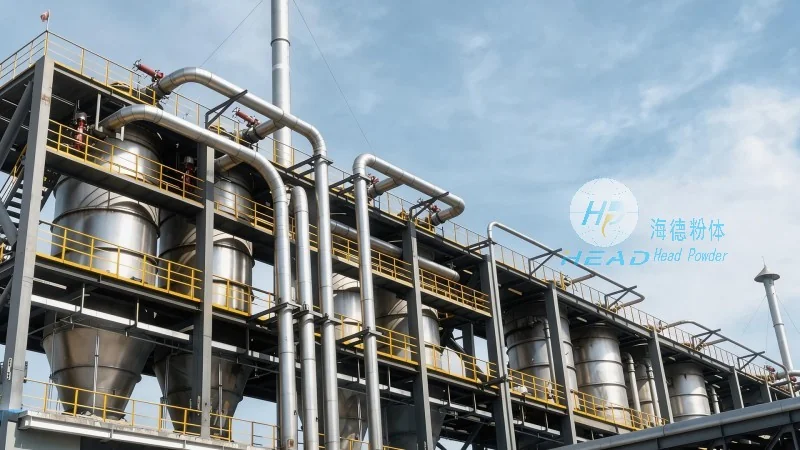
HeadPowder Engineering: Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of customized pneumatic conveying solutions tailored to the unique needs of the sugar industry. With years of experience in designing and manufacturing bulk material handling systems, HeadPowder has established itself as a trusted partner for sugar processing facilities worldwide. The company specializes in developing efficient and reliable systems that ensure optimal performance and minimal downtime. HeadPowder's team of engineers and technicians work closely with clients to understand their specific requirements, from the type of sugar being handled to the operational environment and safety standards. This collaborative approach ensures that the final solution is tailored to meet the exact needs of the client, providing a seamless integration into existing processes.
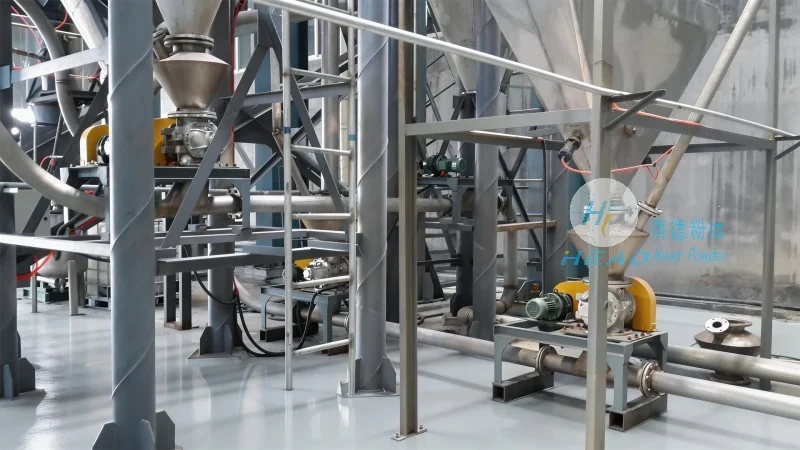
Key Features of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems for white sugar handling are designed with several key features that enhance performance and reliability. One of the most notable features is the use of high-quality materials that are resistant to corrosion and wear, ensuring long-term durability. The systems are equipped with advanced control systems that allow for precise regulation of the conveying rate, pressure, and temperature, providing optimal control over the entire process. Additionally, the systems are designed with safety in mind, incorporating features such as emergency shut-off valves and pressure relief devices to prevent accidents and ensure compliance with industry regulations. The company also offers customization options, allowing clients to choose the components and configurations that best suit their specific requirements, from the type of fan or blower to the material of the conveying pipes.
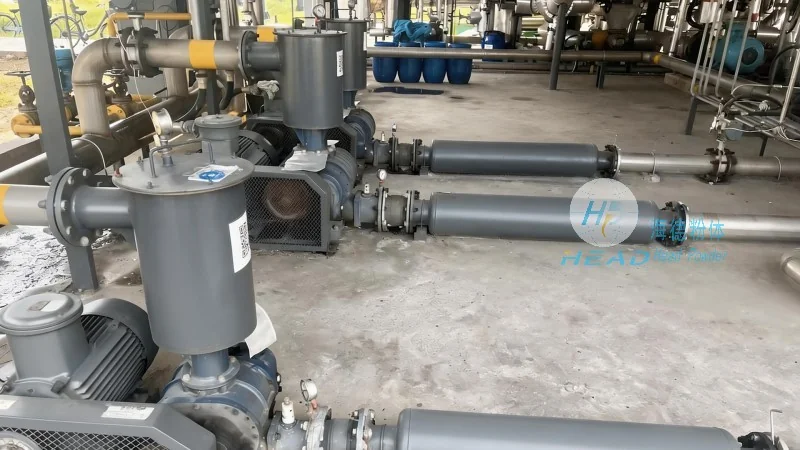
Applications and Use Cases in Sugar Processing
Pneumatic conveying systems from HeadPowder are used in a variety of applications within sugar processing facilities. One common application is the transport of white sugar from storage silos to processing units, such as refining or packaging equipment. The systems can also be used to move sugar between different stages of the production process, such as from the refining stage to the drying stage. Additionally, the systems are used in packaging operations, where the sugar is conveyed from the processing unit to the packaging line. In each of these applications, the pneumatic conveying system provides a smooth and efficient transfer of the material, minimizing the risk of product loss or contamination. The systems are also suitable for handling other granular materials, such as sugar beet pulp or molasses, making them a versatile solution for a range of sugar processing operations.
Benefits for Sugar Processing Facilities
Implementing a pneumatic conveying system from HeadPowder offers several benefits for sugar processing facilities. The most significant benefit is the improvement in operational efficiency. The systems provide a continuous and reliable flow of material, reducing downtime and increasing production capacity. Additionally, the systems help to maintain product quality, which is crucial for meeting customer expectations and regulatory requirements. The dust-free operation also reduces the risk of product contamination, which can lead to quality issues and recalls. Furthermore, the systems are designed with safety in mind, reducing the risk of accidents and ensuring compliance with industry regulations. The long-term durability of the systems also helps to reduce maintenance costs and increase the overall lifespan of the equipment.




